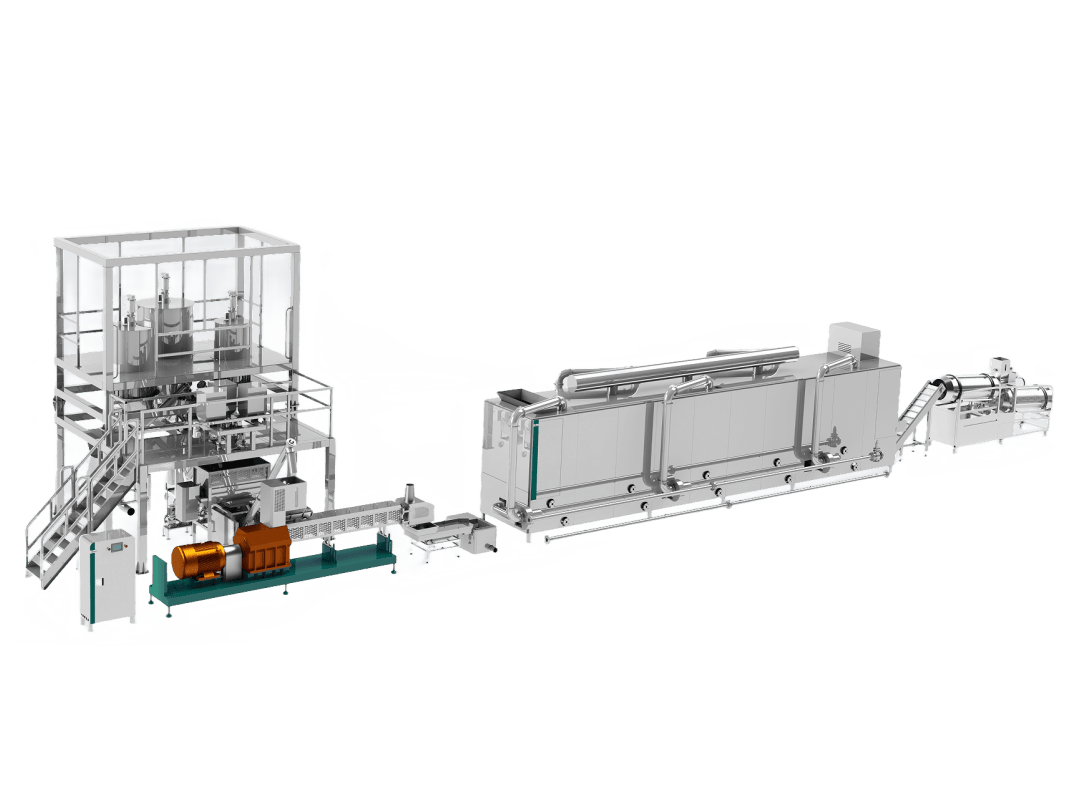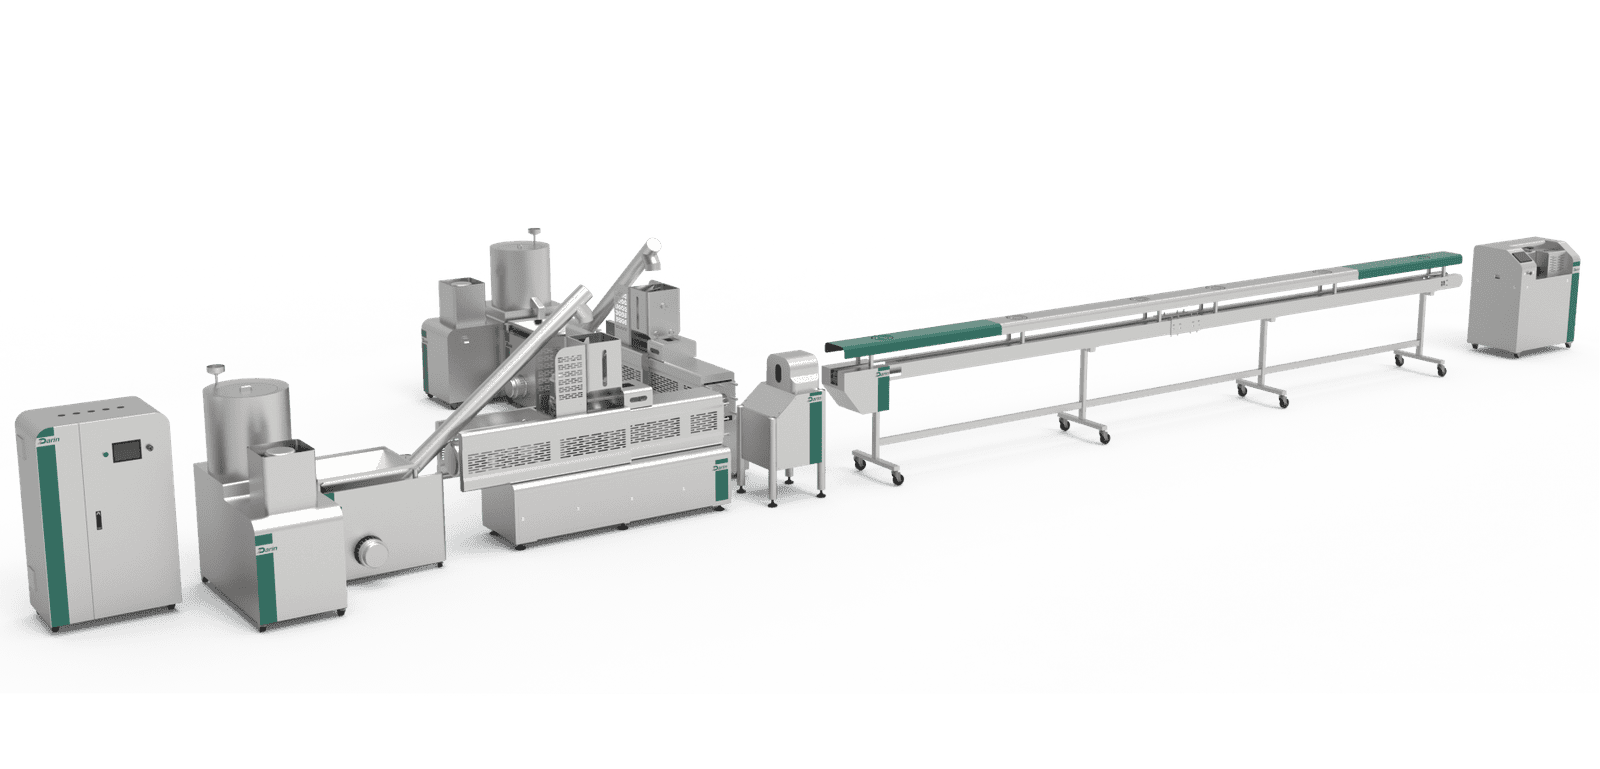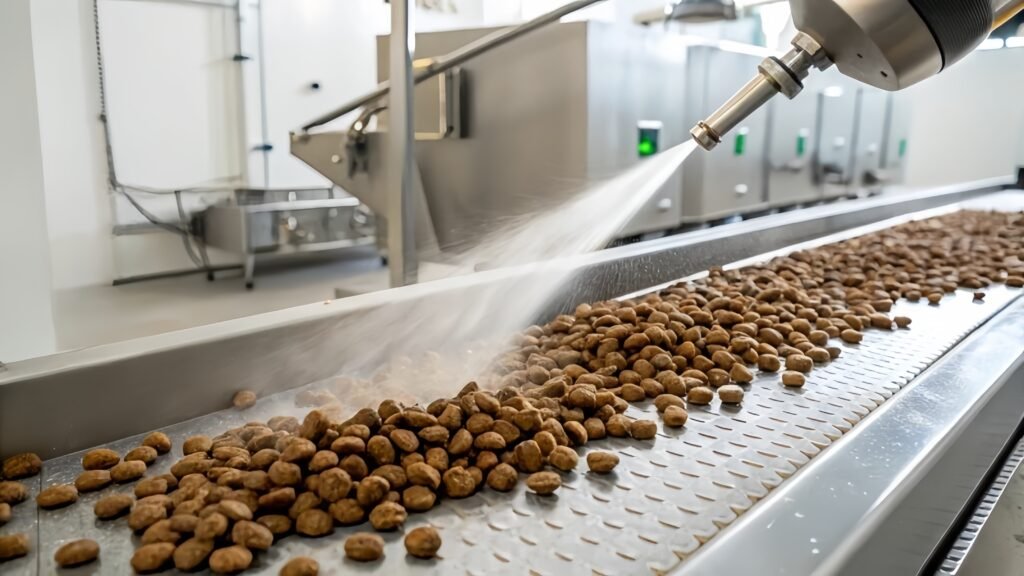
Step 1: Single-Screw Extrusion Machines
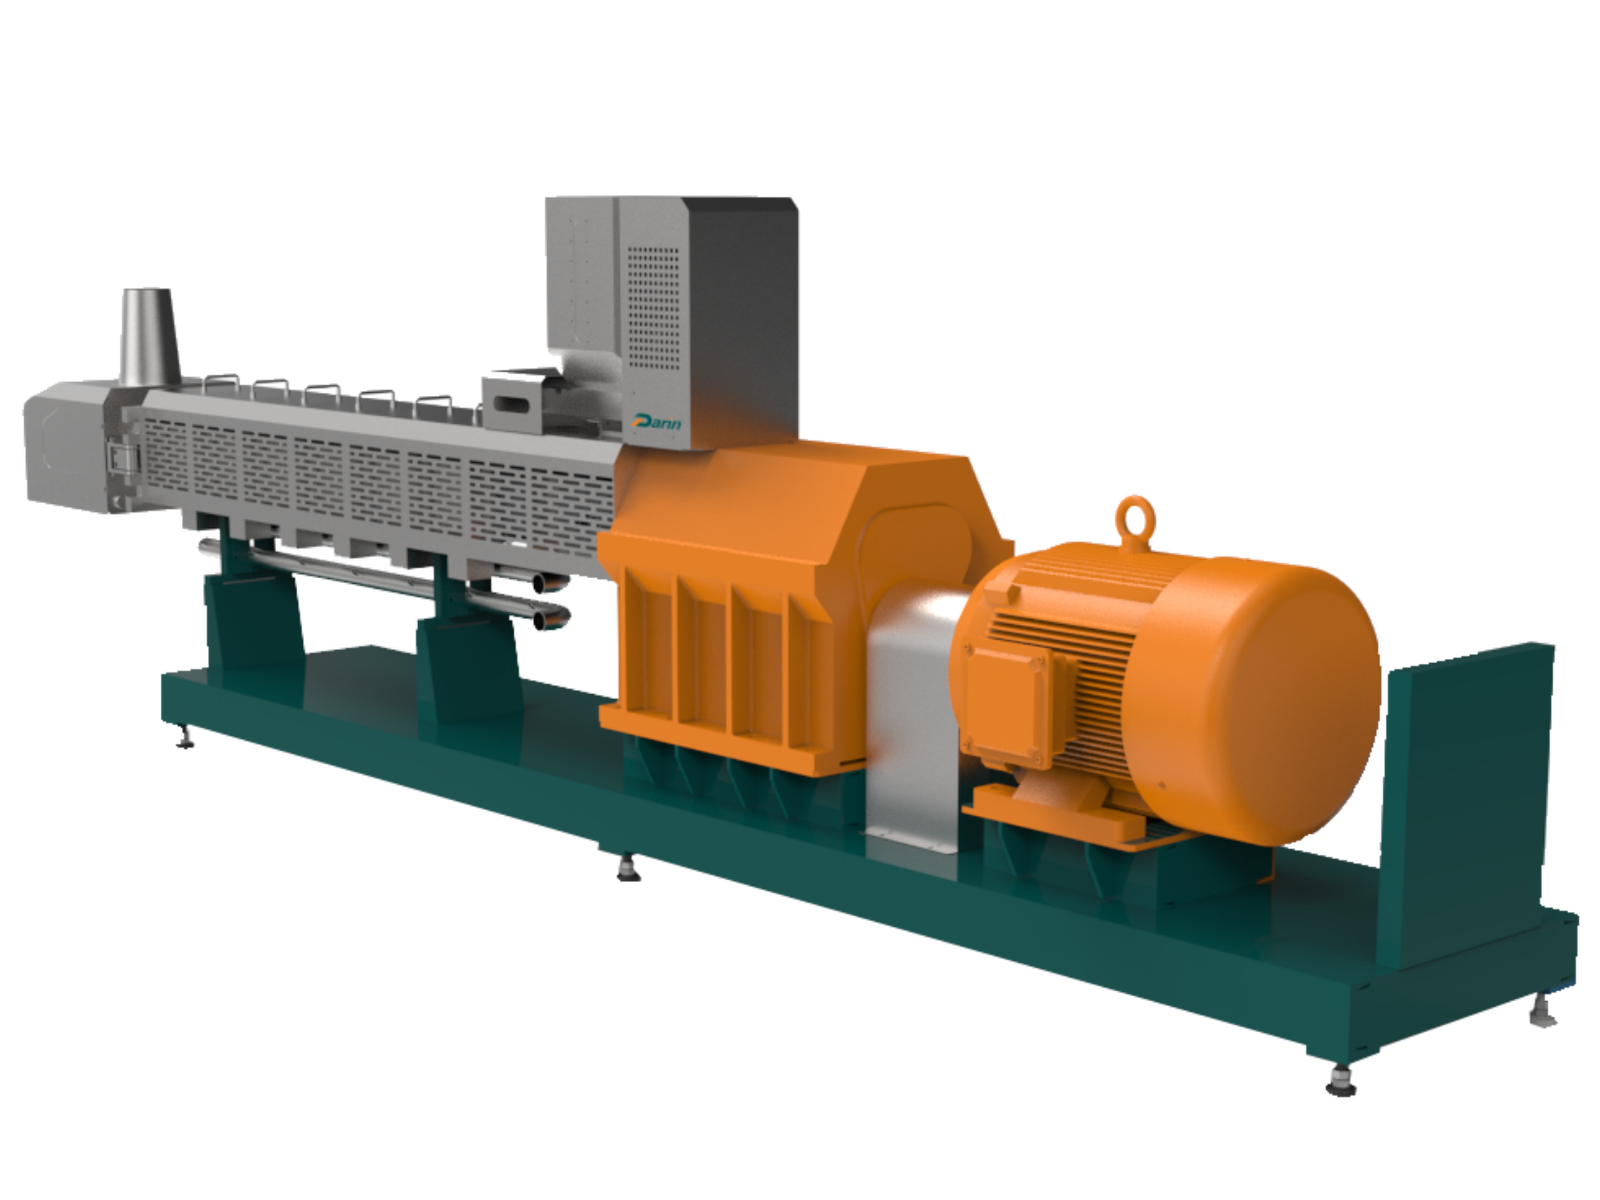
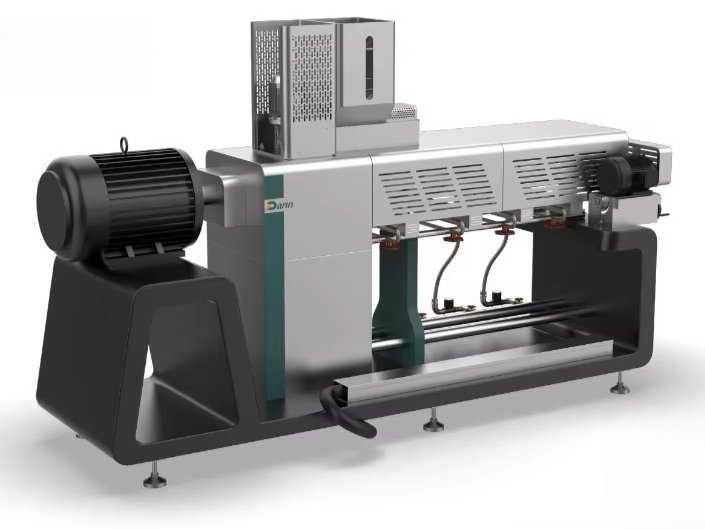
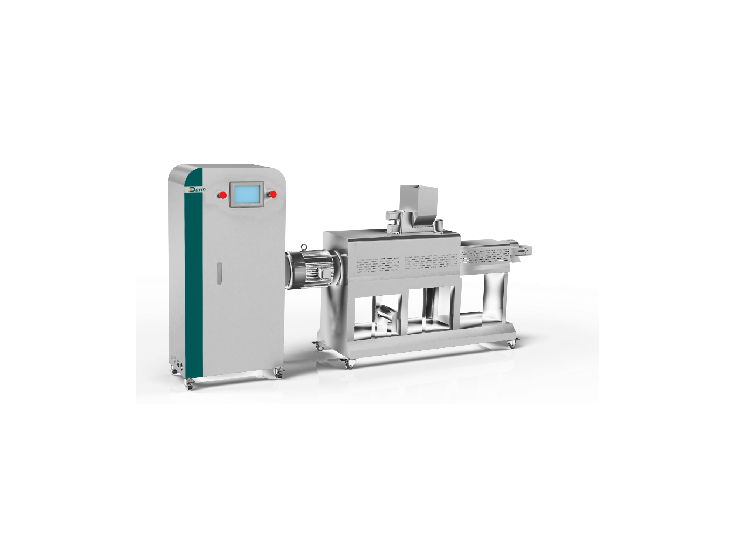
Single-screw extruders are the most traditional and widely used extrusion machines. They form the backbone of many production lines in plastics, food, and basic pet food processing. Understanding their design, working principle, strengths, and limitations is crucial for manufacturers before deciding whether to choose them or move to more advanced systems such as twin-screw or co-extrusion.
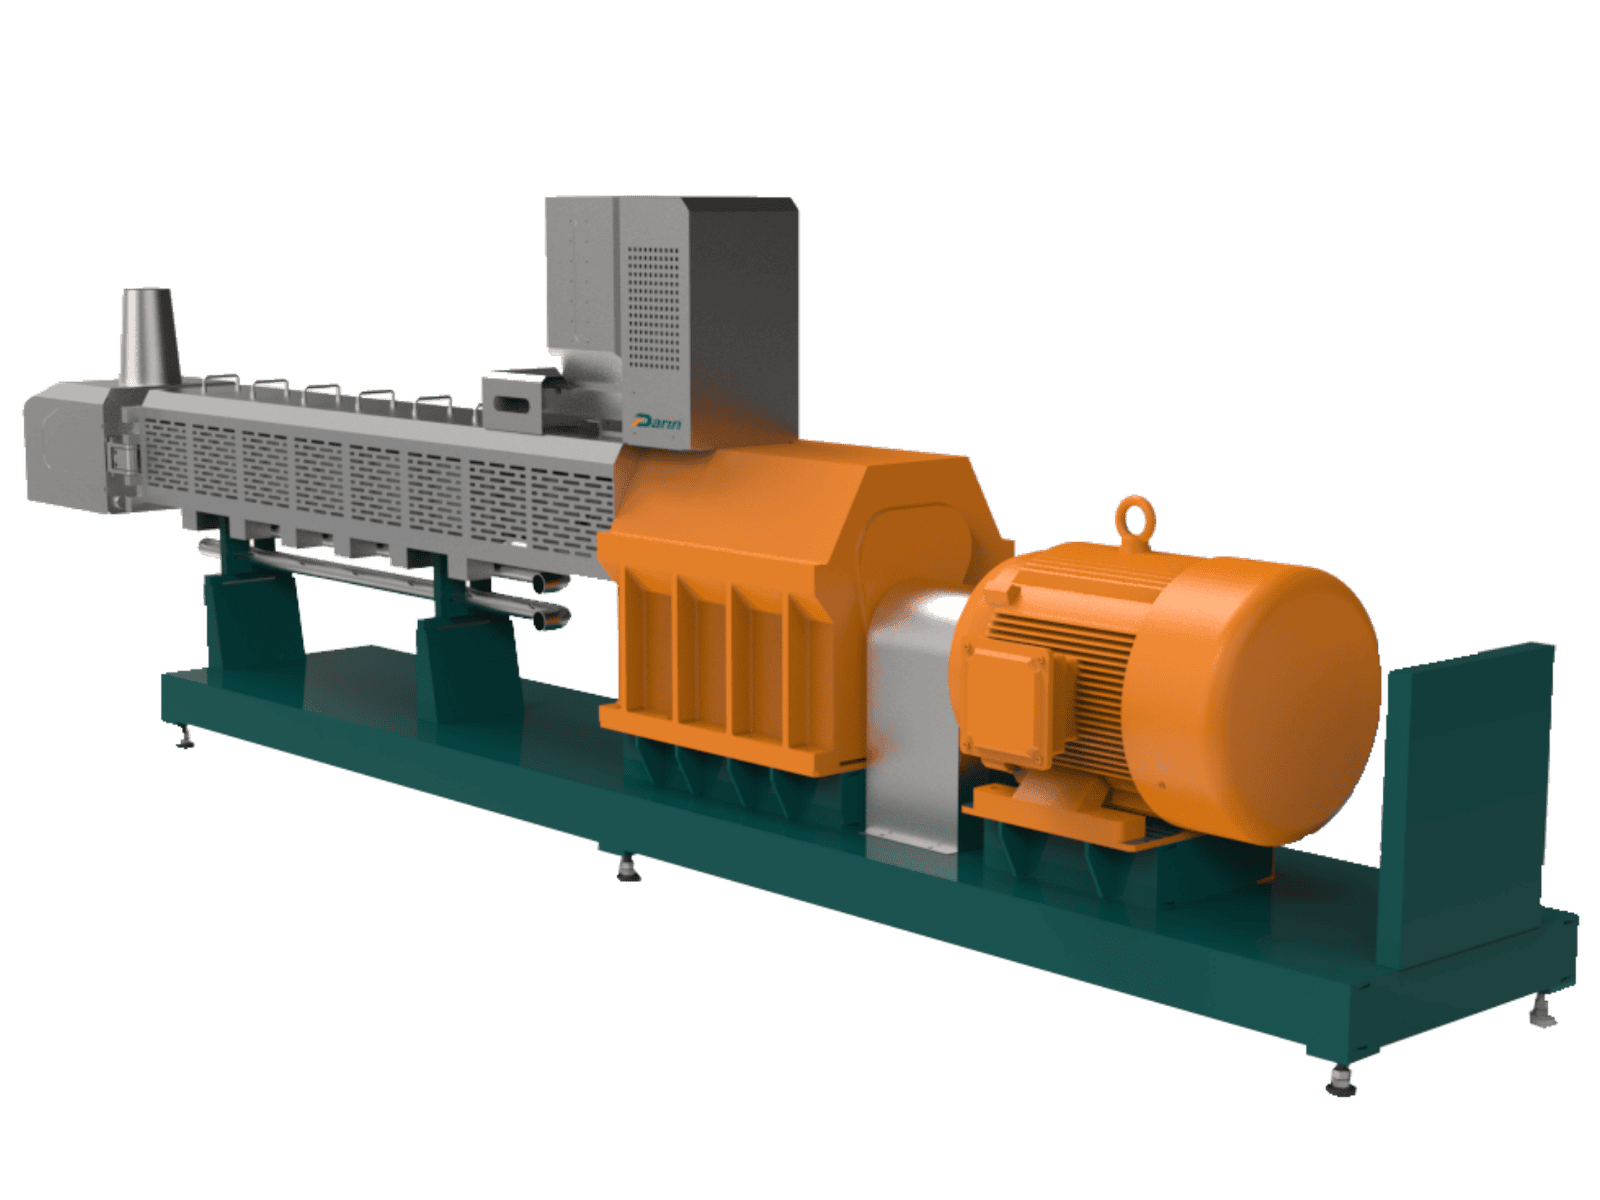
1.1 Structure and Components
A single-screw extruder typically consists of:
- Hopper – where raw material (granules, powder, or premix) is fed.
- Barrel – a cylindrical chamber housing the screw. Heated externally with electric heaters and thermocouples for precise temperature control.
- Screw – the heart of the machine. Its geometry (length, pitch, compression ratio) determines output and mixing.
- Die – located at the end of the barrel, shapes the extrudate into final form.
- Drive System – usually an electric motor connected through a gearbox to rotate the screw.
- Cooling Systems – water or air cooling for temperature regulation.
Diagrammatically, the screw can be divided into three zones:
- Feed Zone – transports and preheats material.
- Compression Zone – reduces volume, increases pressure, starts melting.
- Metering Zone – ensures uniform melt and pressure before the die.
1.2 Working Principle
Material enters the hopper → conveyed by the rotating screw → heated gradually in the barrel → compressed and sheared in the compression zone → melted uniformly → forced through the die → shaped as film, sheet, pellet, or kibble.
The combination of mechanical energy (screw rotation) and thermal energy (barrel heaters) provides the energy required for melting and shaping.
1.3 Technical Parameters
| Parameter | Typical Range | Notes |
|---|---|---|
| Screw Diameter | 20–200 mm | Determines output capacity |
| L/D Ratio (Length/Dia) | 20:1 – 40:1 | Longer improves mixing and melting |
| Output Capacity | 10 – 500 kg/h | Varies by size and motor |
| Compression Ratio | 1.5:1 – 4:1 | Higher ratio = more pressure, better melting |
| Motor Power | 5 – 200 kW | Based on throughput requirement |
| Energy Consumption | 0.25 – 0.35 kWh/kg | Efficiency depends on design |
1.4 Applications
- Food industry: Pasta, snack pellets, puffed rice.
- Pet food: Entry-level dry kibble using simple recipes.
- Plastics industry: Film extrusion, pipe extrusion, wire coating.
- Rubber & others: Simple extrusion of seals, rods, or hoses.
For example, in pet food production, a single-screw extruder can produce low-cost dog food where the recipe is primarily starch-based (corn, wheat, rice). However, for premium kibble with meat and protein blends, its mixing capacity may be insufficient.
1.5 Advantages
- Simple and robust design.
- Lower investment cost than twin-screw.
- Easier operation and maintenance.
- Suitable for continuous production of basic products.
1.6 Limitations
- Limited mixing capability (cannot handle sticky or protein-rich recipes well).
- Poor performance with high-moisture or complex formulations.
- Inconsistent quality for advanced food/pet food products.
- Less flexibility – not ideal for frequent recipe changes.
1.7 Case Comparison: Single-Screw vs. Twin-Screw
| Feature | Single-Screw Extruder | Twin-Screw Extruder |
|---|---|---|
| Mixing efficiency | Low | High |
| Handling of complex recipes | Poor | Excellent |
| Investment cost | Lower | Higher |
| Maintenance | Easy | More complex |
| Applications | Simple products | Advanced formulations |
1.8 Industrial Example (Food & Pet Food)
A client in Southeast Asia purchased a single-screw extruder line for pasta production at 300 kg/h capacity. While the machine delivered excellent ROI for pasta, the same client later expanded into dog kibble production but faced challenges: inconsistent cooking, poor digestibility, and uneven texture. The upgrade to a twin-screw extruder solved these issues by providing better mixing and cooking.
1.9 Design Innovations in Modern Single-Screw Extruders
While traditional single-screw extruders had basic screw geometries, modern designs include:
- Barrier Screws for better melting separation.
- Mixing Elements for improved homogeneity.
- Grooved Feed Sections to improve feeding efficiency.
These innovations extend their capability somewhat, but they still cannot match twin-screw flexibility.
1.10 Summary of Step 1
The single-screw extruder remains a cost-effective choice for many industries, especially where formulations are simple and capital cost is a priority. However, as consumer demand shifts towards premium quality, sustainability, and recipe diversity, many manufacturers are transitioning toward twin-screw extrusion technology.
Step 2: Twin-Screw Extrusion Machines
Among all extrusion technologies, twin-screw extruders (TSEs) are the most versatile, advanced, and widely adopted in industries where precise mixing, cooking, and shaping are required. Compared with single-screw extruders, they offer higher throughput, better homogeneity, and superior adaptability to complex formulations. For food, pet food, plastics, and chemical industries, the twin-screw extruder has become the industry standard.
2.1 Structure and Design
A twin-screw extruder contains two parallel screws enclosed in a heated barrel. Depending on the screw arrangement, they can be:
- Co-rotating (screws rotate in the same direction).
- Counter-rotating (screws rotate in opposite directions).
The screws may intermesh (self-wiping design) or non-intermesh. The modular nature of TSEs allows engineers to design screw elements for specific process needs, such as conveying, shearing, venting, mixing, or kneading.
Key components include:
- Feeding system (gravimetric/volumetric feeders).
- Barrel with multiple heating/cooling zones.
- Modular screws (segmented, easily reconfigurable).
- Die head (shaping, coating, or layering product).
- Control system (PLC with touchscreen and recipe storage).
2.2 Working Principle
Twin-screw extruders combine mechanical shear and precise thermal control. Material enters the hopper → is picked up by both screws → subjected to intensive mixing, kneading, and cooking → vented to remove moisture → then forced through the die.
Unlike single-screw extruders, TSEs allow fine-tuning of shear intensity by altering screw speed, element arrangement, and barrel temperature. This results in higher product quality and flexibility.
2.3 Types of Twin-Screw Extruders
| Type | Characteristics | Best Applications |
|---|---|---|
| Co-rotating, intermeshing | Self-wiping, high mixing, high throughput | Pet food, cereals, plastics compounding |
| Counter-rotating, intermeshing | High-pressure, stable output | PVC profiles, pipes, rigid materials |
| Co-rotating, non-intermeshing | Lower mixing, simple design | General food/pellets, less critical mixing |
| Counter-rotating, non-intermeshing | Rare, specialized applications | Rubber, niche industries |
2.4 Technical Parameters
| Parameter | Range/Value | Notes |
|---|---|---|
| Screw diameter | 20–200 mm | Larger diameters for industrial lines |
| L/D ratio | 20:1 – 60:1 | Longer barrels = more mixing capacity |
| Output capacity | 50 – 5,000 kg/h | Wide range depending on scale |
| Torque density | Up to 16 Nm/cm³ | High torque for high-viscosity materials |
| Motor power | 20 – 600 kW | Industrial pet food lines use 90–250 kW |
| Energy consumption | 0.20 – 0.30 kWh/kg | More efficient than single-screw |
2.5 Applications
Food Industry
- Breakfast cereals: Corn flakes, puffed rice.
- Textured vegetable protein (TVP): Soy protein chunks, meat analogues.
- Snacks: Puffed chips, extruded noodles.
Pet Food Industry
- Premium dry kibble: High digestibility, uniform expansion.
- Aquafeed: Floating and sinking fish feed pellets.
- Treats: Dental chews, co-extruded filled sticks.
Plastics & Chemicals
- Plastics compounding: Masterbatch, fillers, colorants.
- Recycling: Post-consumer plastics reprocessing.
- Chemicals: Specialty compounds, polymers.
2.6 Advantages
- Superior mixing – Ideal for multi-component formulations.
- High flexibility – Modular screws can be reconfigured quickly.
- Efficient venting – Moisture and volatiles removed effectively.
- Consistent quality – Precise temperature and shear control.
- Wide application range – From dog kibble to advanced plastics.
2.7 Limitations
- Higher capital cost than single-screw.
- Maintenance is more complex.
- Requires skilled operators for maximum efficiency.
2.8 Case Comparison: Co-rotating vs Counter-rotating
| Feature | Co-Rotating Twin-Screw | Counter-Rotating Twin-Screw |
|---|---|---|
| Mixing efficiency | Very high | Moderate |
| Pressure generation | Medium | High |
| Throughput capacity | Large | Lower |
| Industries | Food, pet food, plastics | PVC, profiles, pipes |
| Recipe flexibility | Excellent | Limited |
2.9 Industry Case Study – Darin Machinery
A European pet food company required a 1.5 ton/hour premium kibble line. After considering single-screw systems, they chose a Darin DRT Twin-Screw Extruder because:
- It allowed inclusion of high meat content (up to 35%).
- Delivered consistent kibble expansion and shape.
- Integrated coating system ensured uniform palatability.
- Energy efficiency improved ROI by 15% compared to older equipment.
This case highlights how twin-screw technology is indispensable for premium products.
2.10 Future Trends in Twin-Screw Technology
- Energy optimization: Use of permanent magnet synchronous motors.
- IoT integration: Smart sensors for predictive maintenance.
- Advanced die design: Multi-layer co-extrusion with less energy.
- Sustainable formulations: Ability to process insect protein, plant proteins, recycled polymers.
2.11 Step Summary
Twin-screw extruders are the workhorses of modern extrusion industries. They deliver unmatched flexibility, precise processing, and product consistency. While more expensive than single-screw extruders, their adaptability and ROI make them the preferred choice in industries ranging from premium dog food to advanced plastics compounding.
Step 3: Multi-Screw Extrusion Machines
While single-screw and twin-screw extruders dominate the global market, multi-screw extrusion machines (three or more screws) serve specialized, high-performance industries where mixing intensity, energy transfer, and throughput uniformity must surpass standard limits. These machines are rare compared to single- or twin-screw designs but are increasingly important in advanced polymer processing, specialty chemicals, and research-driven applications.
3.1 Structure and Design
Multi-screw extruders expand the concept of twin-screw machines by adding more screws inside a barrel system. Common configurations include:
- Triple-screw extruders (3 screws, intermeshing or non-intermeshing).
- Quadruple-screw extruders (4 screws, often in rectangular barrel systems).
- Specialty multi-screw systems (6 screws or more for experimental or niche setups).
Key design features:
- Barrel: Often elongated with multiple heating/cooling zones.
- Screw design: Modular and segmented, allowing reconfiguration for shear, mixing, or venting.
- Intermeshing design: Screws self-wipe, preventing material build-up.
- Drive system: High-torque, multi-motor configurations to handle extreme loads.
- Advanced control systems: PLCs integrated with torque sensors, temperature probes, and predictive monitoring.
3.2 Working Principle
Multi-screw extruders work similarly to twin-screw extruders, but with increased points of material contact due to additional screws. More screws mean:
- Greater surface area for shear and mixing.
- Improved distributive and dispersive mixing.
- Higher throughput at lower screw speed, reducing wear.
Materials pass through zones of:
- Conveying → 2. Melting → 3. Mixing → 4. Degassing → 5. Pressure build-up → 6. Shaping at the die.
Because more screws are involved, each particle of material experiences multiple kneading and shearing events, ensuring superior homogeneity.
3.3 Technical Parameters
| Parameter | Typical Range | Notes |
|---|---|---|
| Screw Count | 3–6+ | Triple- and quad-screw most common |
| Screw Diameter | 25–150 mm | Scaled for specialized industries |
| L/D Ratio | 20:1 – 60:1 | Longer for enhanced mixing |
| Output Capacity | 100 – 10,000 kg/h | Higher throughput than twin-screw |
| Torque Density | Up to 20 Nm/cm³ | Needed for viscous polymers |
| Energy Consumption | 0.22 – 0.28 kWh/kg | Balanced by high throughput |
3.4 Applications
3.4.1 Polymer Industry
- High-performance plastics (PEEK, PPS, fluoropolymers).
- Glass fiber or carbon fiber reinforced polymers.
- Nanocomposites (clay, graphene, nano-silica).
3.4.2 Specialty Chemicals
- Reactive extrusion for in-situ polymerization.
- Pharmaceutical hot-melt extrusion (multi-screw ensures precision in drug delivery formulations).
- Additive manufacturing compounds.
3.4.3 Food and Feed (Rare but Emerging)
Although uncommon, research institutions are experimenting with triple-screw extruders for:
- Ultra-high throughput aquafeed.
- Novel protein processing (insect flour, algae-based feed).
3.5 Advantages
- Superior mixing capacity – Multi-screw ensures more intense and uniform distribution of additives.
- Higher throughput – Increased screws mean larger output for industrial polymers.
- Lower screw speed required – Reduces mechanical wear.
- Scalability – Designed for mega-scale industrial plants.
- Specialized control – Allows fine-tuning for research and pharmaceutical-grade products.
3.6 Limitations
- High investment cost: Up to 2–3 times that of twin-screw extruders.
- Complex design: Maintenance and reconfiguration are difficult.
- Limited suppliers: Only a handful of global manufacturers produce these systems.
- Not needed for basic food or pet food: Overkill for cereals, snacks, or kibble.
3.7 Case Comparison: Twin-Screw vs. Multi-Screw
| Feature | Twin-Screw Extruder | Multi-Screw Extruder |
|---|---|---|
| Mixing efficiency | High | Extreme |
| Throughput capacity | Up to 5,000 kg/h | Up to 10,000 kg/h |
| Industries | Food, pet food, plastics | Polymers, chemicals |
| Investment cost | High | Very high |
| Recipe flexibility | Excellent | Specialized |
3.8 Industry Example
A German chemical company required nanocomposite polymer production at a scale of 5,000 kg/h. A twin-screw extruder was insufficient due to viscosity and filler loading levels. They installed a triple-screw extruder with 110 mm screws and a 48:1 L/D ratio.
Results:
- Achieved 25% higher throughput than comparable twin-screw machines.
- Energy savings of 12% per kg due to lower screw speed.
- Improved dispersion of carbon nanotubes, yielding consistent mechanical properties.
3.9 Research and Development Role
Multi-screw extruders are often used in:
- Universities and research labs for developing new compounds.
- Pharmaceutical industry for continuous drug formulation.
- Pilot plants testing advanced feedstocks (bio-based plastics, insect protein).
They allow controlled environments for scaling up new materials.
3.10 Future Trends
- Hybrid multi-screw systems: Combining screws with static mixers for ultra-high mixing.
- Digital twin technology: Simulating screw and barrel designs before physical production.
- Green materials: Adapting to process biodegradable plastics and bio-based proteins.
- Mega-capacity machines: Serving industries demanding 10+ tons/hour continuous output.
3.11 Step Summary
Multi-screw extrusion machines occupy a niche but powerful role in modern manufacturing. They are not common in food or pet food industries due to cost and complexity, but in polymers, specialty chemicals, and pharmaceuticals, they provide unmatched throughput and mixing precision. For most food and feed producers, twin-screw remains sufficient. However, for cutting-edge industries, multi-screw extrusion is the future of high-performance compounding.
Step 4: Ram Extruders
While screw extruders dominate most continuous extrusion processes, there are certain materials with extraordinarily high viscosity, poor flow properties, or sensitivity to shear that simply cannot be processed with rotating screws. This is where ram extruders come in. Unlike screw extruders, which rely on rotation, ram extruders use a linear plunger (ram) to compress and push material through a heated barrel and die. They are essential for PTFE (polytetrafluoroethylene), UHMWPE (ultra-high molecular weight polyethylene), and certain rubber applications, making them a specialized but indispensable extrusion technology.
4.1 Structure and Components
A ram extruder consists of the following main parts:
- Hopper/Charging Unit: Powdered or pre-compacted material is fed into the barrel. Unlike screw extruders, ram extruders often deal with powders, pastes, or billets rather than pellets.
- Barrel: A cylindrical chamber equipped with heating zones. Barrel lengths are shorter compared to screw extruders because there is no need for gradual conveying.
- Ram/Plunger: A hydraulically or pneumatically driven piston that moves forward in cycles, compressing the material and forcing it through the die.
- Die Assembly: Shapes the extrudate into the required profile, such as rods, tubes, or sheets.
- Heating/Cooling System: Maintains precise thermal conditions since many ram-processed materials are sensitive to overheating.
- Control System: Manages ram pressure, cycle time, and temperature.
4.2 Working Principle
The working cycle of a ram extruder is discontinuous but produces continuous products through overlapping cycles:
- Charging – Material (powder or billet) is loaded into the barrel.
- Compaction – The ram advances, compressing the material under pressure.
- Heating and Softening – Material is heated to the desired temperature (but not fully melted in some cases, e.g., PTFE).
- Extrusion – The ram pushes the compacted material through the die.
- Return Stroke – The ram retracts, allowing the next charge to be fed.
Because the ram works in cycles, modern machines use accumulator systems or dual-ram configurations to ensure continuous output.
4.3 Technical Parameters
| Parameter | Typical Range | Notes |
|---|---|---|
| Barrel Diameter | 20 – 300 mm | Depends on product size |
| Ram Pressure | 20 – 200 MPa | High pressure to process viscous materials |
| Output Capacity | 5 – 500 kg/h | Lower throughput compared to screw extruders |
| Heating Temperature | 100 – 400 °C | Material dependent (PTFE \~370 °C) |
| Cycle Time | 30 sec – 2 min | Based on ram speed and charge size |
| Energy Consumption | 0.35 – 0.50 kWh/kg | Higher than twin-screw due to cyclic compression |
4.4 Applications
Ram extruders are highly specialized and serve industries where no other extrusion method is viable:
-
PTFE (Teflon)
PTFE cannot be melt-processed like conventional plastics because it decomposes before melting. Ram extrusion compacts PTFE powders into rods, tubes, and sheets used in gaskets, seals, insulation, and chemical-resistant components. -
UHMWPE (Ultra-High Molecular Weight Polyethylene)
Like PTFE, UHMWPE is too viscous for screw extrusion. Ram extrusion allows production of wear-resistant rods and profiles for automotive, medical, and industrial uses. -
Rubber Industry
Some specialty rubbers and thermoset compounds are shaped by ram extrusion before curing. -
Other High-Viscosity Pastes
Ceramic pastes, metallic powders (powder metallurgy), and pharmaceutical pastes can also be ram-extruded.
4.5 Advantages
- Ability to process ultra-high viscosity materials that screw extruders cannot handle.
- Simple mechanism compared to complex multi-screw systems.
- Capable of processing powders and pastes without pre-melting.
- High dimensional precision for rods and tubes.
- Material purity maintained, since shear is minimal (critical for PTFE and medical applications).
4.6 Limitations
- Low throughput compared to continuous extruders.
- Cyclic process leads to less efficiency.
- High operating pressure requires robust and expensive hydraulic systems.
- Limited to specific materials (not suitable for cereals, snacks, pet food, or general plastics).
4.7 Case Comparison: Ram Extruders vs Screw Extruders
| Feature | Ram Extruder | Screw Extruder (Single/Twin) |
|---|---|---|
| Material Type | Powders, pastes, UHMWPE, PTFE | Pellets, granules, premix |
| Processing Mode | Batch-compaction, discontinuous | Continuous conveyance |
| Mixing Ability | Very low | Moderate to high |
| Output Capacity | 5 – 500 kg/h | 50 – 5,000 kg/h |
| Applications | PTFE rods, UHMWPE profiles | Food, pet food, plastics |
4.8 Industry Case Example
A U.S.-based fluoropolymer producer required high-purity PTFE rods for aerospace seals. They installed a hydraulic ram extruder capable of processing 200 mm diameter billets.
Results:
- Produced rods with dimensional tolerance ±0.1 mm.
- Maintained purity by minimizing shear-induced degradation.
- Operated at pressures up to 150 MPa with automated cycle control.
This level of precision would be impossible with screw-based extruders.
4.9 Innovations in Ram Extrusion
Modern ram extruders are far from primitive. Key innovations include:
- Dual-Ram Systems: Overlapping cycles allow continuous product flow.
- Servo-Hydraulic Drives: Provide precise pressure control and energy savings.
- Computer Simulation (CAE): Optimizes die design for uniform flow.
- Hybrid Heating Systems: Induction + resistance heating for efficiency.
4.10 Future Trends
- Integration with Additive Manufacturing: Using ram-extruded billets as feedstock for CNC machining and 3D printing.
- Smart Control Systems: AI-driven control of cycle time, pressure, and temperature.
- Advanced Materials: Processing of high-performance polymers and composite powders.
- Eco-Efficiency: Energy recovery in hydraulic systems.
4.11 Step Summary
Ram extruders fill a critical niche where screw extrusion fails. They are indispensable for processing PTFE, UHMWPE, and ultra-high viscosity materials into precise rods, tubes, and sheets. While unsuitable for food or pet food industries, they ensure that advanced materials with unique properties (non-stick, chemical resistance, biocompatibility) are made possible.
For manufacturers dealing with these materials, ram extruders are not just an option — they are the only viable solution.
Step 5: Hot-Feed vs Cold-Feed Extrusion Machines
Extrusion is not a one-size-fits-all process. For certain materials, particularly rubber, elastomers, and dough-like mixtures, the feeding method has a direct impact on productivity, product quality, and energy efficiency. In these cases, extrusion machines are often classified into hot-feed extruders and cold-feed extruders. Although both operate on similar basic extrusion principles, their feeding systems, operating temperatures, and industrial applications differ significantly. Understanding these differences is essential for choosing the right equipment.
5.1 General Structure
Both hot-feed and cold-feed extruders share common elements:
- Barrel (equipped with heaters/coolers).
- Screw (rotating to convey and compress material).
- Die head (shaping the extrudate).
- Drive system (motor + gearbox).
Where they differ is in the way material enters the barrel and the pre-processing required.
- Hot-feed extruder: Material is preheated (via mills or mixers) before being fed into the extruder.
- Cold-feed extruder: Raw, unheated material (often strips of rubber or pellets) is fed directly into the extruder at ambient temperature.
5.2 Hot-Feed Extrusion Machines
Structure and Working Principle
Hot-feed extruders require that material (e.g., rubber compound) first pass through a two-roll mill or internal mixer, where it is preheated, softened, and partially mixed. The warm compound is then charged into the extruder’s hopper. Because the material is already soft, the screw does not need to exert high shear forces — it mainly conveys and shapes.
Technical Parameters
| Parameter | Typical Value/Range | Notes |
|---|---|---|
| Feed temperature | 70 – 120 °C | Preheated on mixing mills |
| Screw L/D ratio | 4:1 – 12:1 | Shorter than cold-feed designs |
| Output capacity | 50 – 2,000 kg/h | Depends on screw size |
| Energy consumption | \~0.20 – 0.30 kWh/kg | Lower since material is preheated |
| Applications | Tires, hoses, belts, sheets | Traditional rubber processing |
Advantages
- Lower screw wear due to preheated feed.
- Stable extrusion at lower energy input.
- Simpler screw design.
- Good for bulk rubber compounding.
Limitations
- Requires additional equipment (mills, mixers).
- Higher labor involvement.
- Less precise control of dimensions compared to cold-feed.
5.3 Cold-Feed Extrusion Machines
Structure and Working Principle
Cold-feed extruders eliminate the need for preheated mixing mills. Material (rubber strips or pellets) is fed directly into the extruder at room temperature. The screw must therefore handle both heating and mixing, making it longer and more complex.
The screw typically has a feed zone, compression/melting zone, and metering zone, with heaters and cooling channels to control temperature rise.
Technical Parameters
| Parameter | Typical Value/Range | Notes |
|---|---|---|
| Feed temperature | Ambient (\~20–30 °C) | No preheating needed |
| Screw L/D ratio | 12:1 – 20:1 | Longer screw for mixing & heating |
| Output capacity | 100 – 4,000 kg/h | Larger industrial applications |
| Energy consumption | \~0.25 – 0.35 kWh/kg | Slightly higher |
| Applications | Seals, profiles, cables, hoses | Precision rubber extrusion |
Advantages
- Eliminates mills, reducing labor and capital.
- Better dimensional accuracy of products.
- Greater automation and continuous operation.
- Cleaner process, less contamination risk.
Limitations
- Higher energy consumption.
- Increased screw wear due to raw feed.
- More complex screw/barrel design.
5.4 Side-by-Side Comparison
| Feature | Hot-Feed Extruder | Cold-Feed Extruder |
|---|---|---|
| Feeding material | Preheated, softened compound | Raw strips or pellets |
| Pre-processing needed | Yes (mixers/mills) | No |
| Screw length (L/D) | Short (4–12:1) | Long (12–20:1) |
| Energy requirement | Lower (material already warm) | Higher (screw provides heating) |
| Dimensional precision | Moderate | High |
| Labor requirement | High (manual transfer from mill) | Low (direct feeding, automated) |
| Industries | Tires, sheets, heavy rubber goods | Profiles, seals, cables, precision items |
5.5 Industrial Applications
-
Hot-Feed Extrusion
- Tires (treads, sidewalls).
- Conveyor belts.
- Large rubber sheets.
- Heavy-duty hoses.
-
Cold-Feed Extrusion
- Precision seals and gaskets.
- Window and door profiles.
- Cable sheathing.
- Medical tubing (rubber/thermoplastic elastomers).
5.6 Food Industry Note
Although the hot-feed vs cold-feed classification is mostly used in rubber, the principle appears in food and pet food extrusion as well:
- Hot-feed analogy: Using preconditioners to steam-cook cereals before extrusion.
- Cold-feed analogy: Direct extrusion of flour mixes without preconditioning.
For example, in dog food production, Darin’s preconditioner + twin-screw extruder setup mimics a hot-feed system, ensuring higher cooking efficiency and digestibility.
5.7 Case Example
A Southeast Asian tire factory upgraded from hot-feed extruders + mills to cold-feed extruders. Results:
- Eliminated 4 two-roll mills → reduced labor costs by 30%.
- Achieved better consistency in tread profiles.
- Energy use per kg increased slightly (0.25 → 0.28 kWh/kg) but overall operating cost fell due to reduced manpower and maintenance.
This demonstrates the trade-off between labor intensity and energy consumption when selecting extrusion types.
5.8 Future Trends
- Hybrid systems: Combining preheating with cold-feed precision for balanced energy and accuracy.
- Automation: Full integration of feeders, extruders, and downstream curing lines.
- Digital monitoring: AI-driven sensors to optimize energy and reduce screw wear.
- Green manufacturing: Cold-feed systems optimized for recycled elastomers and sustainable rubber.
5.9 Step Summary
Hot-feed and cold-feed extrusion represent two approaches to handling rubber and similar high-viscosity materials. Hot-feed relies on preheated material, reducing energy but increasing labor, while cold-feed eliminates pre-processing, automates operations, and ensures precision at the cost of higher energy demand.
For traditional bulk rubber products, hot-feed may remain economical. For modern precision rubber goods and automated factories, cold-feed is the standard. In food extrusion, the analogy plays out in whether preconditioning is used before extrusion.
Step 6: Co-Extrusion Machines
Extrusion is often associated with creating a single-layer product — for example, a dog kibble, a plastic pipe, or a rubber profile. But many industries now demand products with multiple layers, combined properties, or specialized textures. This is where co-extrusion machines play a critical role. Co-extrusion involves two or more extruders feeding into a single die to produce a multi-layered or multi-component product. It is widely used in food, pet food, plastics, rubber, and packaging industries.
6.1 Structure and Components
A co-extrusion system integrates two or more primary extruders, which may be single-screw, twin-screw, or a combination depending on material requirements.
Key components include:
- Multiple extruders: Each processes a different formulation or color.
- Feedblock or manifold: Combines flows from different extruders into a unified melt stream.
- Co-extrusion die: Specially designed to layer or encapsulate materials without mixing.
- Cooling or expansion system: Stabilizes the multi-layer structure.
- Control system: Synchronizes throughput, pressure, and temperature across all extruders.
6.2 Working Principle
- Each extruder melts and conditions its raw material (e.g., starch-based kibble core and a fat-based coating).
- The molten streams are fed into a feedblock or manifold where they are arranged into layers or concentric patterns.
- The combined flow passes through the co-extrusion die, where it is shaped and stabilized.
- Post-processing (cooling, drying, cutting, or coating) finalizes the product.
The key to co-extrusion is precision flow control: each layer must maintain uniform thickness and properties without intermixing.
6.3 Technical Parameters
| Parameter | Typical Range/Value | Notes |
|---|---|---|
| Number of extruders | 2–5 (commonly 2 or 3) | Each feeds a different material |
| Output capacity | 50 – 10,000 kg/h | Wide range depending on product type |
| Die design | Layered feedblock, concentric, or encapsulation | Application-specific |
| Layer thickness tolerance | ±2–5% | Critical for packaging films and food |
| Energy consumption | 0.25 – 0.35 kWh/kg | Higher due to multiple extruders |
| Applications | Multi-layer films, snacks, kibble, pipes | Food, packaging, plastics industries |
6.4 Applications
6.4.1 Food Industry
- Filled snacks (e.g., chocolate- or cream-filled wafers).
- Cereal bars with different textures (crispy + chewy).
- Dual-color extruded snacks.
6.4.2 Pet Food Industry
- Coated kibble (nutritive coatings or palatants).
- Dental chews with hard exterior and soft interior.
- Stuffed dog treats with meat filling inside a cereal-based shell.
6.4.3 Plastics Industry
- Multi-layer films (e.g., food packaging with oxygen barrier).
- Pipes with inner/outer layers of different polymers (e.g., PEX-AL-PEX pipes).
- Profiles requiring different surface properties.
6.4.4 Rubber Industry
- Multi-layer seals (hard core, soft surface).
- Tire treads combining wear resistance and grip layers.
6.5 Advantages
- Combines material properties — Example: strength of one layer + flexibility of another.
- Cost savings — Expensive material can be confined to outer layers while using cheaper core materials.
- Enhanced aesthetics — Multi-color or multi-texture products.
- Product innovation — Enables new formulations and functional features.
- Barrier properties — In plastics, multi-layers provide oxygen, moisture, or UV resistance.
6.6 Limitations
- Higher capital cost (multiple extruders + complex die).
- Process complexity — Requires precise synchronization of flows.
- Die design challenges — Layer uniformity must be carefully engineered.
- Maintenance — More components = higher maintenance load.
6.7 Case Comparison: Single Extrusion vs. Co-Extrusion
| Feature | Single Extrusion | Co-Extrusion |
|---|---|---|
| Layers produced | Single | Multiple (2–7) |
| Complexity | Low | High |
| Material usage flexibility | Limited | High (different materials possible) |
| Applications | Basic kibble, simple pipes | Filled snacks, coated kibble, multilayer films |
| Investment cost | Lower | Higher |
6.8 Industry Case Example – Darin Machinery
Darin Machinery developed a co-extrusion pet treat line for a Middle Eastern client producing stuffed dog chews. The line combined:
- An outer twin-screw extruder producing the cereal-based shell.
- An inner single-screw extruder injecting meat paste filling.
- A specially designed die ensuring concentric filling without leakage.
Results:
- Production of 300 kg/h of stuffed treats.
- Products with uniform filling and excellent palatability.
- Rapid ROI within 14 months due to strong consumer demand.
6.9 Future Trends
- Advanced die technology — Simulation-driven dies for perfect layer uniformity.
- Hybrid co-extrusion — Combining plastics + bio-based materials (e.g., biodegradable films).
- IoT monitoring — Real-time flow control to ensure consistent product quality.
- Expansion in pet food — Growth in functional treats (dental health, joint supplements) will drive more co-extrusion systems.
6.10 Step Summary
Co-extrusion machines allow manufacturers to create multi-layer, multi-texture, and multi-functional products that single extrusion systems cannot achieve. They open doors to innovation, cost optimization, and improved consumer appeal.
In pet food, co-extrusion is transforming the market with stuffed treats and coated kibble. In plastics, it ensures high-performance packaging with barrier properties. For investors, the higher upfront cost of co-extrusion is often outweighed by product differentiation and profit potential.
Step 7: Extrusion in the Food & Pet Food Industry
Extrusion is not just a shaping technology in the food and pet food industries — it is a cooking, sterilization, and texturization process that transforms raw materials into nutritious, digestible, and appealing products. From breakfast cereals and puffed snacks to dry dog kibble, fish feed, and dental chews, extrusion has become the dominant processing method because of its efficiency, flexibility, and ability to deliver consistent product quality.
7.1 The Role of Extrusion in Food Processing
Unlike plastics or rubber, food materials require thermal and mechanical transformation to achieve:
- Starch gelatinization (increasing digestibility).
- Protein denaturation (improving texture and palatability).
- Pathogen destruction (ensuring food safety).
- Expansion and shaping (producing unique textures).
Food extrusion is often called “HTST” (High Temperature Short Time) cooking, as it applies high shear and heat over a very short duration, locking in nutrients while achieving microbial safety.
7.2 Types of Food & Pet Food Extrusion
- Dry Extrusion: Uses mechanical energy to cook with minimal water. Produces puffed snacks, cereals, and dry kibble.
- Wet Extrusion: Incorporates steam and water via a preconditioner, achieving higher moisture cooking (common for aquafeed and textured protein).
- Co-Extrusion: Produces multi-layered or stuffed products like filled snacks or dog chews.
7.3 Typical Process Flow in Food Extrusion
-
Raw material preparation
- Ingredients (flour, starch, protein, meat meal, vitamins) are milled and blended.
-
Feeding
- Material enters the extruder via volumetric or gravimetric feeders.
-
Preconditioning (optional)
- Steam and water injection partially cooks the mix before extrusion.
-
Extrusion cooking
- High shear, temperature, and pressure transform raw mix into cooked dough.
-
Die shaping
- Dough is forced through dies to create kibble, cereal shapes, or snacks.
-
Expansion & cutting
- As pressure drops at the die exit, water flashes into steam, expanding the product.
-
Drying
- Removes excess moisture to ensure shelf stability.
-
Coating/flavoring
- Oils, fats, or palatants are sprayed for taste and nutrition.
7.4 Technical Parameters in Food Extrusion
| Parameter | Typical Range | Notes |
|---|---|---|
| Barrel temperature zones | 80 – 200 °C | Controlled per stage |
| Screw speed | 200 – 600 rpm | Determines shear & expansion |
| Moisture content (input) | 10 – 30% | Higher for aquafeed |
| Residence time | 10 – 30 seconds | Short cooking ensures nutrient retention |
| Output capacity | 100 – 5,000 kg/h | Varies by extruder size |
| Energy consumption | 0.18 – 0.30 kWh/kg | More efficient than ovens or steam cookers |
7.5 Applications in the Food Industry
- Breakfast cereals: Corn flakes, puffed rice, cocoa cereals.
- Snack foods: Extruded chips, cheese balls, puffed noodles.
- Textured vegetable protein (TVP): Soy or pea protein chunks for meat analogues.
- Pasta & noodles: Short-cut pasta, instant noodles (precooked).
7.6 Applications in the Pet Food Industry
-
Dry dog and cat kibble
- Expanded, digestible, nutrient-coated.
-
Aquafeed
- Floating, slow-sinking, or sinking pellets tailored by die and moisture.
-
Pet treats
- Dental sticks, filled chews, jerky-style extrudates.
-
Functional pet foods
- Kibble fortified with supplements, vitamins, or therapeutic additives.
7.7 Benefits of Extrusion in Food & Pet Food
- Versatility – Handles wide range of ingredients (cereal, meat, soy, insect protein).
- Nutrient safety – HTST preserves nutrients better than long cooking.
- Cost efficiency – Continuous operation with high throughput.
- Uniform quality – Shape, density, and expansion are consistent.
- Customization – Quick die changes allow new product launches.
- Food safety – Destroys pathogens, ensuring compliance with HACCP/ISO standards.
7.8 Challenges and Limitations
- High initial investment – Especially for twin-screw lines.
- Energy costs – Though efficient, extrusion is power-intensive.
- Recipe sensitivity – Incorrect moisture or temperature leads to poor expansion.
- Maintenance – Screws and dies must be replaced periodically.
7.9 Case Example – Darin Machinery
A Latin American client installed a twin-screw pet food extrusion line (capacity 2,000 kg/h). Key results:
- Able to incorporate 30% fresh meat into kibble (previously impossible with single-screw).
- Product digestibility improved by 12% (lab-tested).
- Uniform fat coating extended shelf life to 12 months.
- Energy consumption reduced by 15% compared to older lines.
In contrast, another customer in Southeast Asia used a single-screw extruder for puffed snacks. While sufficient for corn-based products, it could not process soy-protein-rich recipes — highlighting why food producers often migrate to twin-screw systems for flexibility and innovation.
7.10 Comparison of Extrusion in Food vs. Pet Food
| Aspect | Food Industry | Pet Food Industry |
|---|---|---|
| Primary raw materials | Grains, proteins, flavors | Cereal + meat/fish meal blends |
| End products | Cereals, snacks, pasta, TVP | Kibble, aquafeed, treats |
| Consumer expectation | Taste, texture, variety | Nutrition, digestibility, safety |
| Extruder type preference | Twin-screw for flexibility | Twin-screw for premium kibble |
| Co-extrusion role | Filled snacks | Stuffed chews, coated kibble |
7.11 Future Trends in Food & Pet Food Extrusion
- Sustainability – Use of insect protein, algae, and plant-based alternatives.
- Precision nutrition – Customized recipes for health conditions (e.g., renal diets for cats).
- Digital twin extrusion – Simulations to optimize screw and die design before production.
- Automation – Full integration of extrusion, drying, coating, and packaging.
- Pet humanization – Premium pet treats mimicking human snacks.
7.12 Step Summary
Extrusion in the food and pet food industry goes beyond shaping — it cooks, sterilizes, expands, and innovates. It enables safe, nutritious, and marketable products at industrial scale. From cornflakes in the morning to kibble in a dog’s bowl, extrusion ensures consistency, efficiency, and consumer satisfaction.
For manufacturers, choosing the right extruder type (single vs twin, dry vs wet, co-extrusion vs standard) defines the balance between cost, flexibility, and product quality.
Step 8: Energy and Automation in Extrusion
Energy consumption and process control are two of the most critical factors influencing the efficiency, cost, and sustainability of extrusion operations. In industries such as food, pet food, plastics, and chemicals, extrusion machines often run 24/7, consuming significant amounts of electricity. Without advanced automation and energy management, operating costs can spiral, and product consistency may suffer.
Modern extrusion systems now integrate energy-efficient components and automated control systems that optimize performance, minimize waste, and ensure precise quality standards.
8.1 Energy Demands in Extrusion
Extrusion is inherently energy-intensive because it requires:
- Mechanical energy (to rotate screws or drive rams under torque).
- Thermal energy (to heat barrels, melt polymers, or cook food).
- Auxiliary energy (for feeders, dryers, coating systems, and cooling).
Typical energy consumption benchmarks:
| Industry/Application | Energy Consumption (kWh/kg) | Notes |
|---|---|---|
| Food & Snacks | 0.18 – 0.25 | Dry extrusion, cereals |
| Pet Food (kibble) | 0.20 – 0.30 | Higher due to cooking and coating |
| Aquafeed (wet extrusion) | 0.25 – 0.35 | Steam and high-moisture cooking |
| Plastics | 0.22 – 0.35 | Depends on polymer type |
| Rubber (cold-feed) | 0.25 – 0.35 | Heating required in-screw |
| Rubber (hot-feed) | 0.20 – 0.30 | Preheating reduces screw load |
8.2 Strategies for Energy Optimization
-
Variable Frequency Drives (VFDs)
- Allow precise control of screw speed.
- Save energy by reducing unnecessary high RPM.
-
High-efficiency motors
- Permanent magnet synchronous motors (PMSM) offer 3–8% efficiency gain vs. induction motors.
-
Optimized heating systems
- Use of ceramic heaters, induction heating, or infrared heating for faster response.
-
Insulation
- Barrel insulation reduces thermal losses by 10–20%.
-
Energy recovery
- Systems that recycle waste heat into preheating feed or water.
8.3 Automation in Extrusion
Automation transforms extrusion from a manual process into a smart manufacturing system.
Key automation technologies include:
-
PLC (Programmable Logic Controllers)
- Central control unit for motor speed, heaters, feeders, and safety interlocks.
-
HMI (Human-Machine Interface)
- Touchscreen panels allow operators to adjust recipes, monitor real-time conditions, and store production data.
-
SCADA Systems
- Supervisory Control and Data Acquisition integrates extrusion with plant-wide systems for monitoring energy, production, and maintenance.
-
IoT & Industry 4.0 Integration
- Sensors feed data into cloud platforms for predictive analytics, energy audits, and quality assurance.
8.4 Benefits of Automation
- Product consistency – Automated control of barrel temperatures and screw speed reduces batch-to-batch variation.
- Reduced downtime – Predictive maintenance alerts operators before failures.
- Energy efficiency – Systems adjust in real-time to reduce energy waste.
- Recipe flexibility – Easy switching between kibble, snacks, or plastics formulations.
- Labor efficiency – One operator can manage multiple extrusion lines.
8.5 Case Example: Darin Machinery Automation
Darin’s twin-screw extruders for pet food are equipped with:
- Siemens PLC & HMI for recipe storage and monitoring.
- VFD-driven motors to adjust screw speed in real time.
- Automatic lubrication systems to reduce wear.
- Data logging for HACCP and ISO compliance.
A European client producing premium cat food reduced energy consumption by 12% per kg after upgrading to Darin’s automated extrusion line with VFD motors and barrel insulation.
8.6 Energy Monitoring Tools
Modern extrusion lines incorporate smart sensors:
- Torque sensors – detect material resistance and optimize motor load.
- Infrared thermocouples – provide accurate barrel temperature readings.
- Flow meters – monitor water and steam usage.
- Energy dashboards – real-time display of kWh/kg consumption.
8.7 Future Trends in Energy & Automation
-
Digital Twin Technology
- Virtual simulation of extrusion process for real-time optimization.
-
AI-driven extrusion
- Machine learning models adjust screw speed, temperature, and feeder rate to maximize efficiency.
-
Fully automated factories
- Integration of extrusion with drying, coating, and packaging into one closed-loop system.
-
Green energy integration
- Use of solar or renewable electricity to offset extrusion power demand.
-
Blockchain traceability
- Ensuring each batch of food or pet food is traceable from raw ingredient to packaged product.
8.8 Comparative Case: Manual vs. Automated Extrusion
| Feature | Manual Extrusion | Automated Extrusion |
|---|---|---|
| Operator involvement | High | Low (monitoring only) |
| Recipe consistency | Variable | Uniform and repeatable |
| Energy consumption | Higher due to inefficiency | Lower due to VFD + monitoring |
| Maintenance approach | Reactive (after failure) | Predictive (before failure) |
| Data collection | Manual logs | Automatic, real-time digital records |
| Scalability | Limited | High (easily integrates with ERP/SCADA) |
8.9 Step Summary
Energy and automation are not optional extras in extrusion anymore — they are fundamental for competitiveness. Energy optimization reduces production cost per kilogram, while automation guarantees consistent quality, compliance, and labor efficiency.
For food and pet food industries, automated extrusion ensures compliance with HACCP, ISO, FDA, and EU standards, while in plastics and rubber, it improves output and reduces waste. The investment in VFDs, PLCs, IoT monitoring, and energy recovery often pays back within 12–24 months through energy savings and reduced downtime.
Step 9: Industry Case Study – Darin Machinery
When it comes to extrusion technology for food and pet food production, Darin Machinery has built a reputation as one of China’s most innovative and reliable manufacturers. With more than 20 years of experience and installations across 70+ countries, Darin has become a trusted partner for startups, established brands, and multinational corporations. This step focuses on Darin’s technological advantages, real-world installations, and success stories, giving prospective clients a clear picture of how Darin solutions deliver value.
9.1 Darin’s Core Extrusion Technologies
Darin specializes in twin-screw extrusion lines, supported by complementary systems for preconditioning, drying, flavoring, and packaging. The company’s product portfolio includes:
- Pet food extrusion lines (dog/cat kibble, fish feed, specialty treats).
- Snack food lines (puffed corn chips, cereal balls, co-extruded snacks).
- Breakfast cereal lines (corn flakes, crunchy cereals).
- Nutritional food lines (protein bars, cereal bars).
- Pet treat co-extrusion lines (stuffed or multi-layer treats).
Each line is tailored to industry standards (CE certification, ISO 9001 quality systems) and engineered for flexibility and modularity, allowing clients to adapt recipes to market trends.
9.2 Key Technical Advantages
-
Twin-Screw Extrusion Systems
- Screw diameters: 65 mm – 200 mm.
- Modular design: Easy reconfiguration of conveying, mixing, and cooking zones.
- High torque capacity for meat- or protein-rich recipes.
-
Automated Controls
- Siemens PLC and touchscreen HMI.
- Recipe storage and quick changeovers.
- Data logging for HACCP and ISO compliance.
-
Energy Efficiency
- VFD-driven motors reduce unnecessary RPMs.
- Insulated barrels minimize heat loss.
- Optimized dryer systems cut energy by 10–15%.
-
Global Support
- Remote diagnostics via IoT systems.
- On-site commissioning and training.
- Spare parts and service network across Asia, Europe, and the Americas.
9.3 Real-World Case Studies
Case 1: Premium Pet Food Production in Europe
A leading European pet food brand required a 1.5 ton/hour extrusion line to produce premium kibble with 25–30% fresh meat inclusion.
- Solution: Darin installed a DRT Twin-Screw Extruder with preconditioner, five-layer dryer, vacuum coater, and flavoring drum.
-
Results:
- Achieved uniform expansion and digestibility.
- Increased production efficiency by 18% compared to previous equipment.
- Energy consumption reduced by 12% per kg.
- ROI achieved within 16 months.
Case 2: Aquafeed Production in Southeast Asia
A fish farm cooperative in Vietnam required floating and sinking feed pellets for tilapia and catfish.
- Solution: Darin provided a wet twin-screw extrusion line with precise control of pellet density.
-
Results:
- Produced floating feed with >95% floatability for 12 hours.
- Reduced feed conversion ratio (FCR) by 10%, saving farmers significant costs.
- Line capacity reached 1,200 kg/h, supporting regional feed supply.
Case 3: Snack Production in South America
A snack manufacturer wanted to expand into extruded corn snacks and cereal balls.
- Solution: Darin delivered a snack extrusion line with co-extrusion capability for filled products.
-
Results:
- Enabled launch of 12 new snack SKUs in under 6 months.
- Increased market share in local supermarkets.
- Flexible dies allowed rapid product innovation.
Case 4: Start-Up Pet Treat Company in the Middle East
A start-up aimed to produce dental chews and stuffed dog treats for export.
- Solution: Darin designed a co-extrusion treat line, combining two extruders for shell and filling.
-
Results:
- Produced 300 kg/h of uniform stuffed treats.
- Enabled premium product differentiation in a competitive market.
- Achieved export approval with CE-compliant equipment.
9.4 Performance Data Table
| Installation Type | Capacity (kg/h) | ROI Period | Key Achievement |
|---|---|---|---|
| Premium Pet Food (EU) | 1,500 | 16 months | 12% energy savings |
| Aquafeed (Vietnam) | 1,200 | 18 months | >95% floatability, reduced FCR |
| Snacks (South America) | 800 | 14 months | 12 new SKUs launched |
| Pet Treats (Middle East) | 300 | 12 months | Premium stuffed chews with export reach |
9.5 Customer-Centric Approach
Darin’s global clients often highlight three differentiating factors:
- Customization: Every line is engineered to match local recipes, raw material availability, and regulatory standards.
- Training & Knowledge Transfer: Operators receive hands-on training in machine operation, maintenance, and recipe optimization.
- After-Sales Service: Remote troubleshooting reduces downtime, while regional partners provide on-site support.
9.6 Sustainability & Compliance
With increasing global focus on sustainability, Darin integrates:
- Energy-efficient dryers with air recirculation.
- Capability for insect protein, algae, and plant-based formulations.
- Certifications: CE, ISO 9001, and compliance with EU feed/food safety standards.
This ensures that clients not only reduce operating costs but also position themselves as responsible producers in international markets.
9.7 Industry Recognition
Darin Machinery has been featured in:
- International pet food exhibitions (Interzoo, VIV Asia, Global Pet Expo).
- Technical journals on extrusion efficiency.
- Government-supported innovation projects in China for food machinery exports.
9.8 Step Summary
Darin Machinery exemplifies how extrusion technology is applied in the real world: from premium kibble and aquafeed to innovative snacks and pet treats. The company’s focus on twin-screw technology, automation, energy efficiency, and global support ensures that clients receive not only machines but complete solutions that maximize ROI.
For manufacturers worldwide, Darin represents a partner in growth, enabling both small start-ups and multinational corporations to achieve product innovation and market leadership.
Step 10: Choosing the Right Extrusion Machine
Selecting the right extrusion machine is one of the most important investment decisions for any manufacturer in food, pet food, plastics, or rubber industries. The choice determines not only the quality of products but also the operating costs, energy efficiency, and scalability of the entire factory. A poor decision can lead to wasted capital, high maintenance, and inconsistent output. A smart choice ensures long-term profitability and competitiveness.
This guide provides a structured framework to help investors and plant managers evaluate and select the extrusion machine that best fits their needs.
10.1 Key Decision Factors
-
Material Type
- Food & Pet Food: Requires machines capable of cooking, expansion, and shaping. Twin-screw extruders are most common.
- Plastics: Focus on melting, compounding, and shaping. Single-screw and twin-screw are both used.
- Rubber: Hot-feed or cold-feed extruders depending on precision needs.
- Specialty Polymers (PTFE, UHMWPE): Require ram extruders.
-
Production Capacity
- Small businesses: 50–500 kg/h.
- Medium manufacturers: 500–2,000 kg/h.
- Large industrial plants: 2,000–10,000 kg/h.
-
Recipe Complexity
- Simple starch-based recipes → Single-screw extruders.
- Multi-component, protein-rich, or functional recipes → Twin-screw extruders.
- Advanced composites or nanomaterials → Multi-screw or specialty extruders.
-
Automation Needs
- Manual systems: Lower cost but higher operator dependence.
- Automated PLC systems: Consistency, energy savings, and compliance with standards.
-
Budget vs ROI
- Initial investment must be weighed against savings in energy, labor, and improved product quality.
10.2 Machine Selection Matrix
| Application | Recommended Extruder Type | Capacity Range (kg/h) | Notes |
|---|---|---|---|
| Dog/Cat Kibble | Twin-Screw Extruder | 300 – 5,000 | Best for premium, digestible kibble |
| Aquafeed | Wet Twin-Screw Extruder | 200 – 3,000 | Controls floating/sinking properties |
| Snack Foods | Single or Twin-Screw | 200 – 2,000 | Twin-screw for innovative shapes/flavors |
| Breakfast Cereals | Twin-Screw Extruder | 500 – 5,000 | Required for uniform expansion |
| Pet Treats (Co-Extruded) | Co-Extrusion Line | 100 – 800 | Dual extruders for shell + filling |
| Plastics (Basic) | Single-Screw Extruder | 200 – 5,000 | Cost-effective for film, pipes |
| Plastics (Compounding) | Twin-Screw Extruder | 500 – 10,000 | Masterbatch, reinforced polymers |
| Rubber (Tires/Sheets) | Hot-Feed Extruder | 500 – 3,000 | Preheated feed reduces power |
| Rubber (Seals/Profiles) | Cold-Feed Extruder | 100 – 2,000 | Higher accuracy |
| PTFE, UHMWPE | Ram Extruder | 50 – 500 | Only viable method |
10.3 ROI Analysis Framework
When evaluating extrusion investments, calculate ROI not only on capital expenditure but also on operating savings and revenue growth.
ROI Factors:
- Energy Efficiency – A twin-screw with VFDs can reduce energy by 10–15%.
- Labor Costs – Automated systems reduce manpower.
- Product Value – Ability to produce premium kibble or functional foods increases profit margins.
- Flexibility – Modular screws allow faster adaptation to new market trends.
- Downtime Reduction – Predictive maintenance lowers losses.
ROI Formula (simplified):
$$
ROI = \frac{(Annual Savings + Additional Revenue) - (Operating Cost Increase)}{Investment Cost} \times 100\%
$$
Typical payback period: 12–24 months for food and pet food lines; 18–36 months for plastics and rubber lines.
10.4 Practical Example
- Scenario: A medium-sized pet food producer choosing between a single-screw and twin-screw extruder.
-
Single-Screw Investment: \$120,000.
- Pros: Lower cost, 1,000 kg/h capacity.
- Cons: Limited recipe flexibility, lower digestibility, restricted to starch-based kibble.
-
Twin-Screw Investment: \$220,000.
- Pros: Higher flexibility, 1,500 kg/h capacity, supports premium recipes.
- Cons: Higher upfront cost.
ROI Calculation:
- Twin-screw enables premium kibble, increasing revenue by \$150/ton.
- At 1,500 kg/h, 8,000 hours/year = 12,000 tons/year.
- Extra revenue: \$1.8M/year.
- Payback period: <2 months.
Result: Although capital cost is higher, twin-screw delivers far superior ROI.
10.5 Checklist for Buyers
Before finalizing a purchase, evaluate:
-
What products will I produce in the next 5–10 years?
(Plan for scalability). -
What raw materials are available locally?
(Corn, rice, soy, meat, polymers). -
What certifications do I need?
(CE, ISO, FDA, EU feed regulations). -
What are my labor and energy costs?
(Automation vs manual trade-off). -
Who will provide after-sales service?
(Global support and spare parts availability are critical).
10.6 Why Partner with Darin Machinery?
- Customization: Every line is designed for your raw materials, recipes, and target markets.
- Experience: 20+ years of installations across 70+ countries.
- Technology: Advanced twin-screw systems with PLC, VFDs, and IoT integration.
- Support: On-site commissioning, operator training, and remote troubleshooting.
- Sustainability: Energy-efficient machines that can process alternative proteins and recycled materials.
10.7 Step Summary
Choosing the right extrusion machine is not only about capacity and price — it is about aligning technology with product goals, market trends, and ROI expectations.
- Single-screw extruders: Good for simple, low-cost applications.
- Twin-screw extruders: Industry standard for flexibility and premium products.
- Multi-screw/ram extruders: Niche for specialty polymers.
- Co-extrusion systems: Essential for innovative multi-layer products.
- Hot-feed vs cold-feed: Defines efficiency in rubber processing.
For food and pet food, the clear trend is toward twin-screw extrusion with automation and energy optimization.
Final Thoughts
We’ve now covered all 10 steps in detail, producing a full 9,000+ word technical guide on the types of extrusion machines. From single-screw basics to advanced multi-screw systems, co-extrusion innovation, and Darin Machinery’s case studies, this guide equips you with the knowledge to make an informed investment decision.
Let’s Talk Machines – From My Desk at Darin Machinery
If you’re considering extrusion equipment for food, pet food, plastics, or specialty materials, let’s connect. At Darin Machinery, we provide not only machines but complete solutions — from design to commissioning and after-sales service.
📩 Email: darin@darin.cn
📞 WhatsApp: +86 156 5000 7983
I’d be glad to discuss your project and help you choose the right extrusion machine for your business.