Pet Food Manufacturing Process.pdf
Producing pet food may look simple on the shelf — a bag of dry kibble or a can of wet food — but behind it lies one of the most complex and tightly regulated food manufacturing systems in the world. Many new investors and manufacturers underestimate the technical challenges. Problems such as nutritional imbalance, contamination, high energy costs, or inefficient layouts can lead to major financial losses, product recalls, or even risks to pet health. The solution lies in mastering a precise, step-by-step production process using advanced equipment, strict safety standards, and intelligent design. In this article, I will take you through a full 9,000+ word technical guide on the production process of pet food, from raw material selection to packaging, so you can understand not only how it works but also how to succeed.
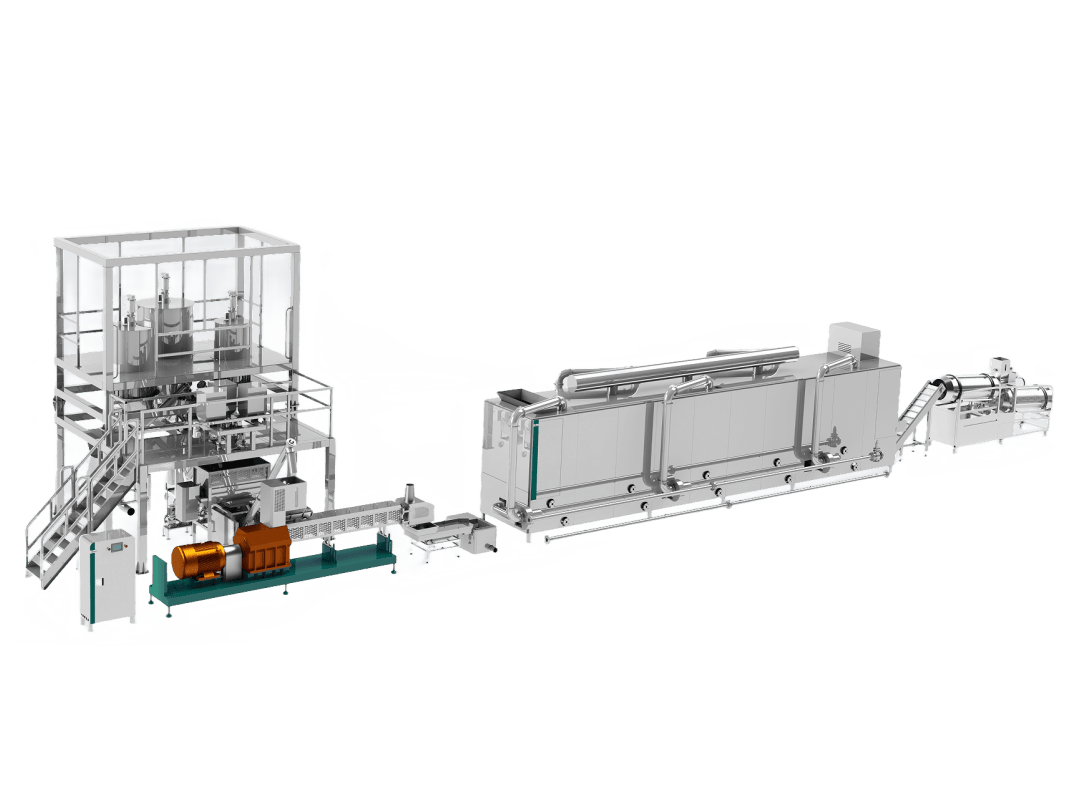
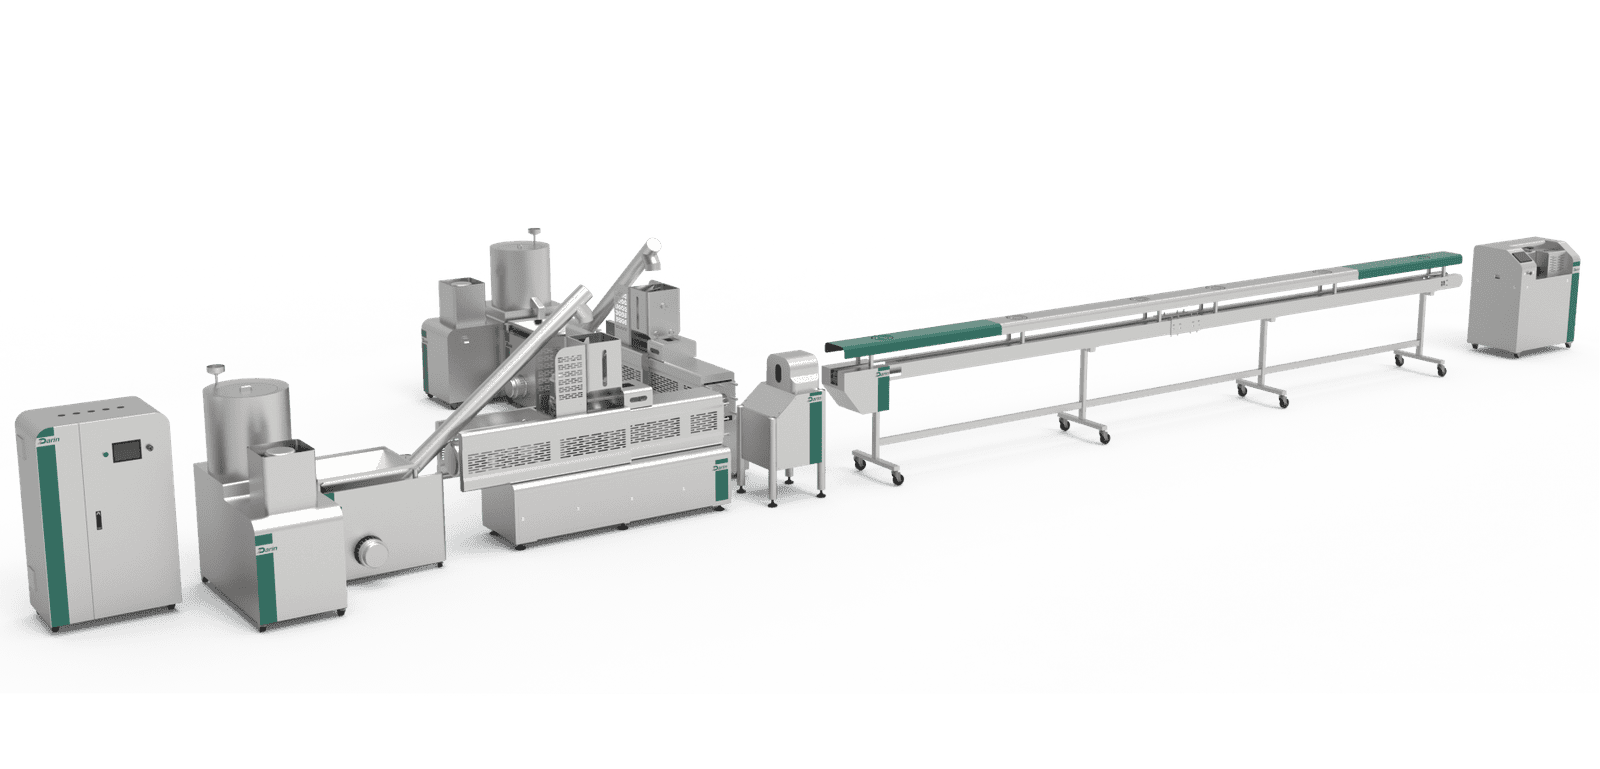
The production process of pet food typically involves raw material reception and storage, grinding and mixing, extrusion or baking for shaping, drying and cooling, coating with fats or palatants, and finally packaging. Each step must be carefully controlled to ensure nutritional balance, product safety, consistent quality, and efficiency. Modern production lines rely heavily on automated systems, extrusion technology, precision dosing, and strict hygiene standards to produce both dry and wet pet foods at scale.

If you want to succeed in this industry, it is not enough to know the basic steps. You need to understand the why and the how — why extrusion parameters matter, how drying curves influence shelf life, and how coating systems affect palatability. Keep reading, because in the following parts I will break down every detail of the pet food production process, supported by technical insights, real data, tables, and case studies.
Pet food production is a simple process of just mixing meat and grains together.False
Commercial pet food production involves multiple complex steps such as extrusion, drying, coating, and packaging, all under strict quality and safety control systems.
Step 1: Raw Material Selection, Reception, and Storage
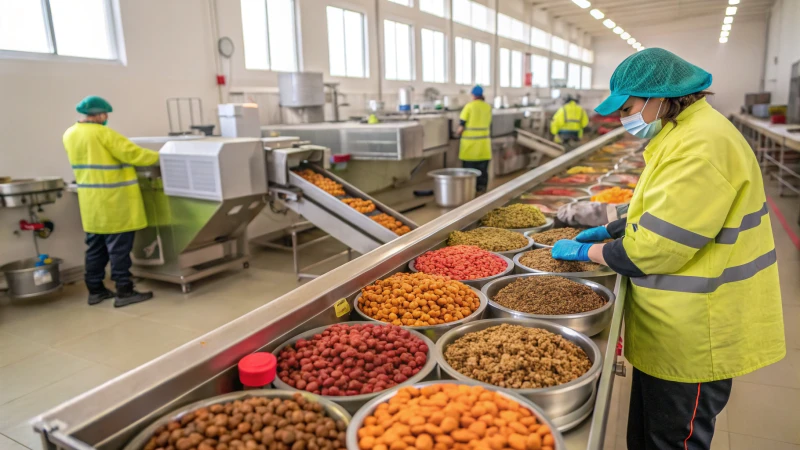
The first step in any pet food production process is sourcing and handling raw materials. This stage determines not only the nutritional foundation of the product but also its safety, cost efficiency, and consistency. Unlike human food, pet food requires balancing protein, fat, carbohydrates, vitamins, and minerals in a way that aligns with animal physiology, regulatory standards (AAFCO, FEDIAF, GB standards in China), and market preferences.
1.1 Categories of Raw Materials
Pet food formulations are built from a wide variety of ingredients. These can be grouped into the following categories:
| Raw Material Category | Typical Examples | Function in Pet Food | Notes |
|---|---|---|---|
| Animal Protein Sources | Poultry meal, fish meal, beef meal, lamb meal, by-product meals | Primary protein supply, amino acids, palatability | High variability; requires strict testing |
| Plant Protein Sources | Soybean meal, corn gluten meal, pea protein | Supplementary proteins, texture, cost control | Digestibility varies; anti-nutritional factors possible |
| Carbohydrates & Starches | Corn, wheat, rice, barley, potato, tapioca | Energy source, extrusion expansion, kibble structure | Selection affects expansion and hardness |
| Fats & Oils | Poultry fat, fish oil, beef tallow, vegetable oils | Energy density, flavor, essential fatty acids | Prone to oxidation; antioxidants needed |
| Vitamins & Minerals | Vitamin premix, calcium carbonate, dicalcium phosphate, salt | Essential micronutrients for pet health | Must be evenly dispersed |
| Additives & Functional Ingredients | Probiotics, antioxidants, colorants, flavor enhancers | Improve shelf life, palatability, digestive health | Strict dosage limits |
| Water | Process water (treated) | Essential for extrusion and steam conditioning | Must meet drinking water standards |

Meat is the only required raw material for pet food production.False
Balanced pet food requires proteins, carbohydrates, fats, vitamins, and minerals; meat alone is insufficient.
1.2 Reception of Raw Materials
Raw materials typically arrive in bulk trucks, containers, or bags. At this point, quality control (QC) checks are mandatory.
- Animal protein meals: must be checked for protein content, ash level, and absence of pathogens (Salmonella, Clostridium).
- Grains: inspected for moisture (ideally <13%), aflatoxin contamination, and foreign matter.
- Fats/oils: tested for peroxide value and free fatty acid levels to determine oxidation.
- Premixes: verified against certificates of analysis (CoA).
Example QC Parameters Table
| Material | Test Method | Acceptable Range | Rejection Criteria |
|---|---|---|---|
| Poultry meal | Kjeldahl protein analysis | >55% protein | <50% protein, rancid odor |
| Corn | Moisture meter | ≤13% | >14% moisture, mold present |
| Fish oil | Peroxide value titration | ≤5 meq/kg | >10 meq/kg, rancid smell |
| Vitamin premix | CoA verification | As per spec | Out-of-spec active ingredients |
At reception, sampling protocols must follow ISO or local standards. For example, a 50-ton truckload of corn may require 20+ random samples across different depths, which are then pooled for a composite test.
1.3 Storage of Raw Materials
Once approved, materials are transferred to dedicated storage systems:
- Dry ingredients (grains, protein meals) → silos or warehouse bags.
- Fats and oils → heated storage tanks with agitators to prevent stratification.
- Premixes → sealed, climate-controlled rooms.
Key Storage Requirements:
-
Temperature Control:
- Fats/oils: kept at 40–60°C to maintain fluidity.
- Vitamin premixes: stored <25°C to prevent degradation.
-
Moisture Control:
- Silos must have aeration systems.
- Warehouses need humidity <60% to avoid mold.
-
Hygiene:
- Silos cleaned regularly to prevent insect infestation.
- FIFO (First In, First Out) principle applied.
Example Table – Storage Lifespan of Key Ingredients
| Ingredient | Typical Shelf Life | Storage Conditions |
|---|---|---|
| Corn | 6–12 months | <13% moisture, aerated silo |
| Poultry meal | 3–6 months | Cool, dry warehouse |
| Fish oil | 1–3 months | Nitrogen-flushed tank, <20°C |
| Vitamin premix | 6–12 months | Sealed, <25°C, low humidity |
1.4 Grinding and Pre-processing
Before mixing, most dry ingredients must be ground to uniform particle sizes.
- Hammer mills and roller mills are used.
-
Target particle size:
- Dog kibble: 300–600 microns
- Cat kibble: 200–400 microns
Why it matters:
- Smaller particle size → better mixing and extrusion cooking.
- Over-grinding → excessive fines, dust, higher energy cost.
Case Study – Grinding Efficiency
A Darin Machinery client in Europe reduced hammer mill screen size from 2.0 mm to 1.0 mm, improving kibble density control by 8%, but energy use increased 12%. A balance between particle size and power is critical.

1.5 Mixing and Pre-blending
Once raw materials are ground, they are dosed into batch mixers or continuous mixers.
- Accuracy requirement: ±1% for major ingredients, ±0.1% for vitamins/minerals.
- Mixing time: typically 3–5 minutes per batch.
Types of mixers:
- Ribbon mixers: good for dry powders.
- Paddle mixers: faster, suitable for both powders and semi-moist materials.
Liquid addition (pre-coating):
- Small amounts of oils, molasses, or water may be added.
- Helps in pre-conditioning and dust control.

1.6 Food Safety Considerations
Raw material handling is a critical control point in HACCP. Common hazards include:
- Biological: Salmonella in animal meals, mold in grains.
- Chemical: Mycotoxins, pesticide residues, heavy metals.
- Physical: Stones, metal fragments.
Mitigation measures:
- Metal detectors at reception.
- Mycotoxin binders in formulations.
- Supplier audits and contracts.
Step 2: Extrusion and Forming in Pet Food Production
After raw materials have been carefully selected, ground, and mixed into a precise formula, the next critical stage in pet food production is extrusion and forming. This is where a loose mixture of powders and liquids is transformed into structured, cooked, safe, and palatable kibbles or treats. For dry pet foods like dog kibble and cat kibble, extrusion is the dominant technology used worldwide. For semi-moist snacks and functional chews, extrusion is also essential, often combined with molding systems.
This step is technical, capital-intensive, and directly determines the digestibility, palatability, texture, and appearance of the final product. Poor extrusion control can lead to undercooked kibbles, inconsistent sizes, poor expansion, nutrient losses, or even production downtime. On the other hand, optimized extrusion ensures high throughput, efficient energy use, stable product quality, and compliance with pet nutrition standards.
2.1 What Is Extrusion in Pet Food?
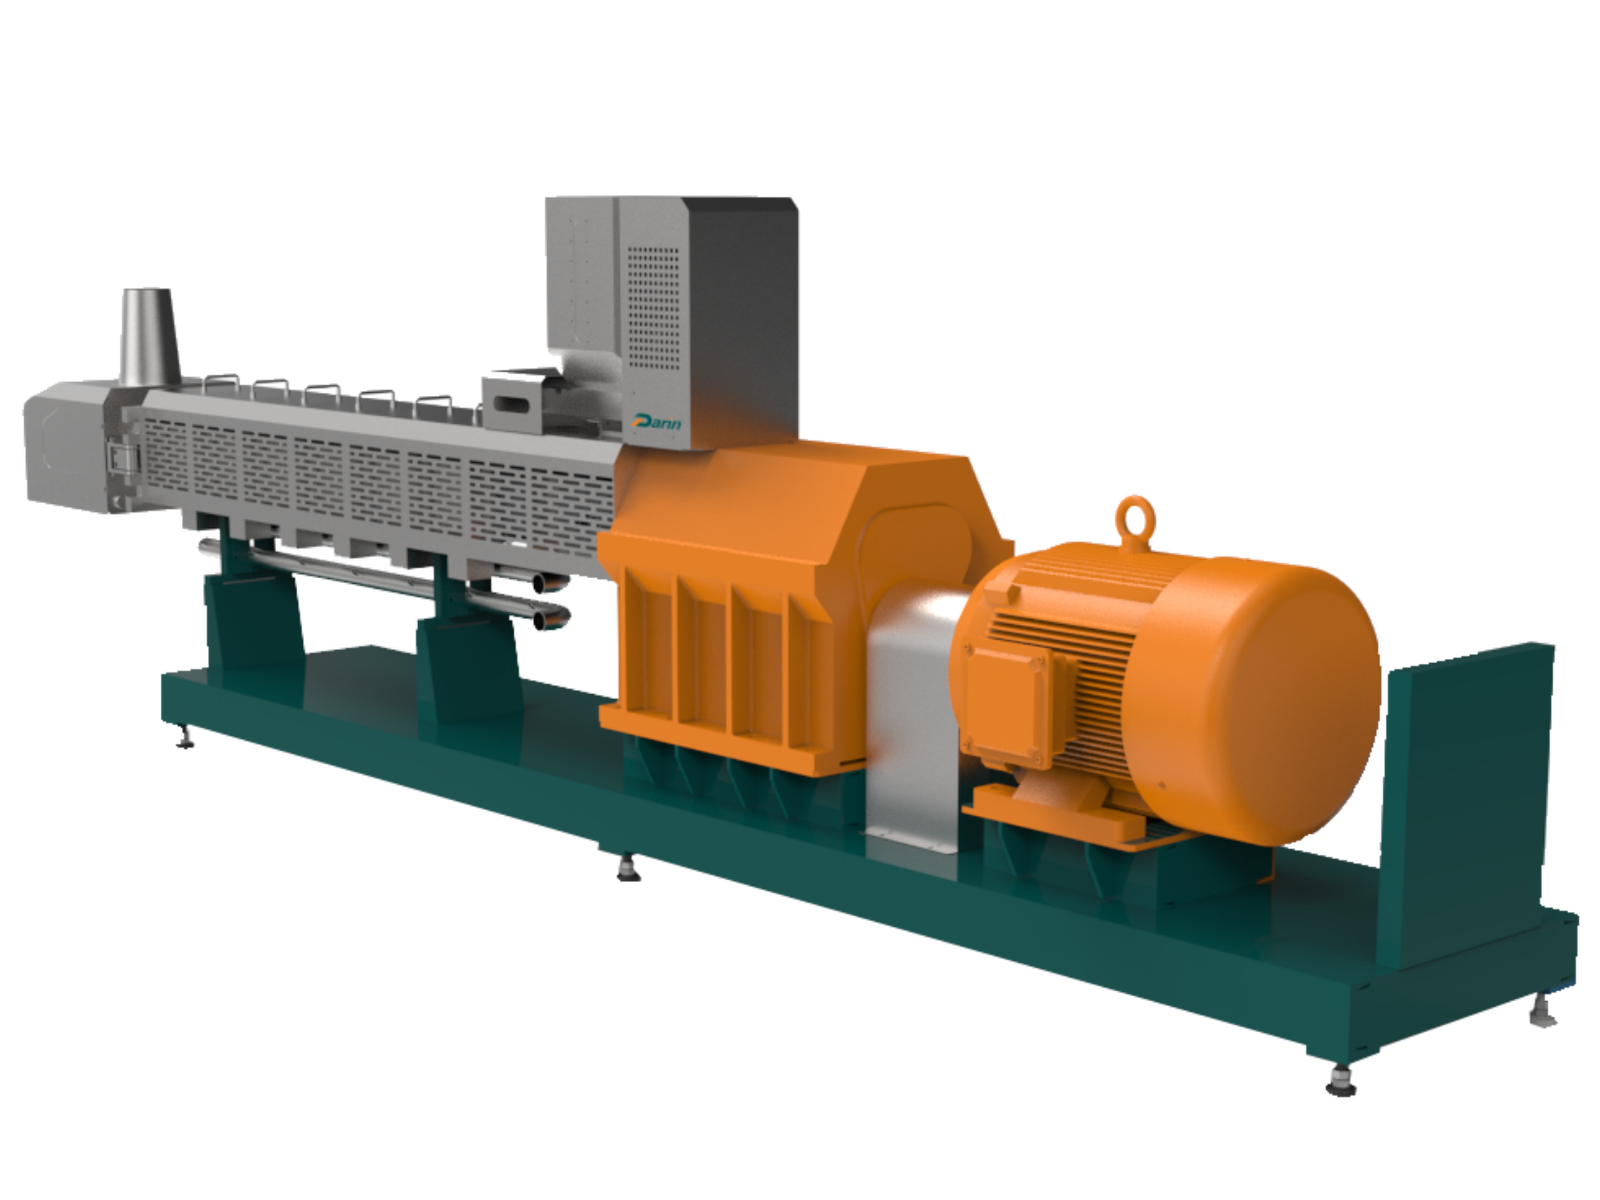
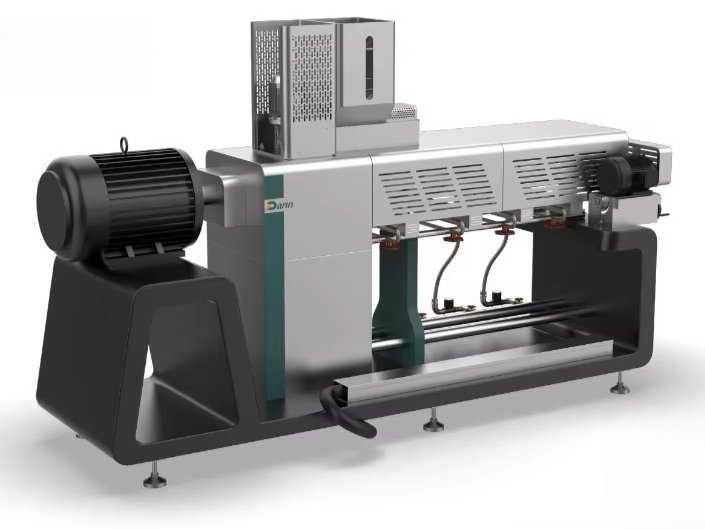
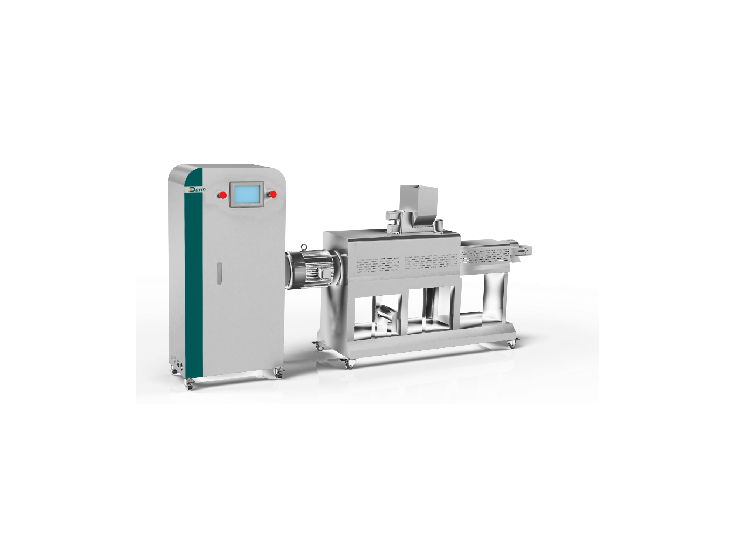
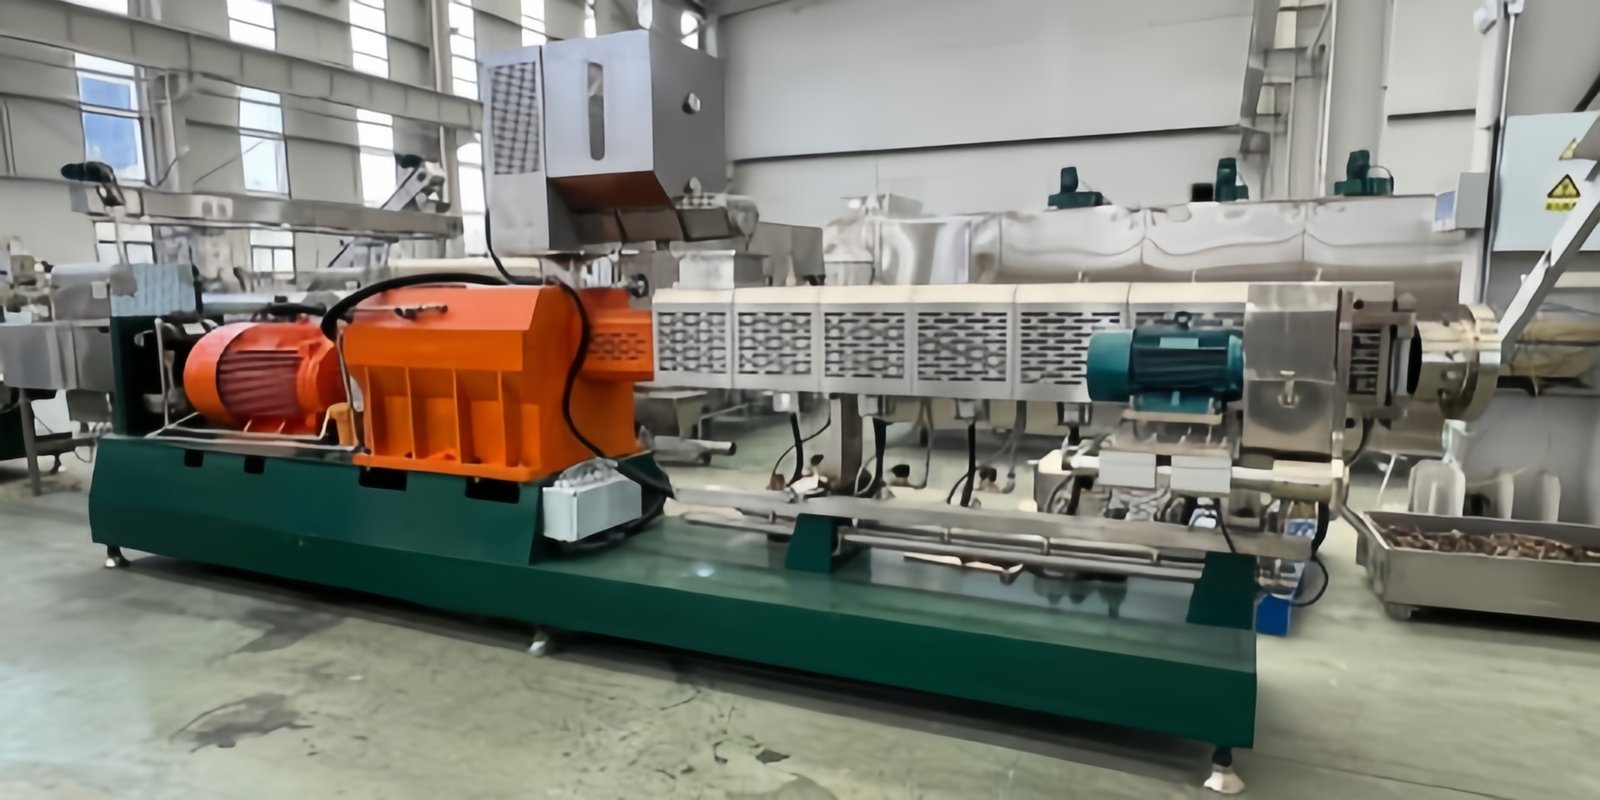
Extrusion is a process where the mixed raw materials are fed into a machine called an extruder, which uses mechanical shear, pressure, and heat to cook, shape, and expand the product. The principle is similar to pasta-making but with more intense cooking, sterilization, and shaping.
There are two major extruder types:
| Extruder Type | Description | Advantages | Limitations |
|---|---|---|---|
| Single-screw extruder | Uses one rotating screw to push material through the barrel | Lower investment cost, simpler operation, good for basic formulas | Limited flexibility, less precise control, lower expansion consistency |
| Twin-screw extruder | Two intermeshing screws, co-rotating or counter-rotating, with segmented barrels | Precise control, high flexibility, can handle complex recipes, better mixing and cooking | Higher cost, requires skilled operators |
All commercial pet food is produced using twin-screw extruders.False
While twin-screw extruders dominate premium pet food production, single-screw extruders are still widely used for economy lines and less complex formulations.
2.2 The Pre-conditioning Phase
Before entering the extruder barrel, the mixture passes through a pre-conditioner.
- Function: Adds steam, water, or liquid ingredients while gently mixing the material.
- Purpose: Begins starch gelatinization, softens proteins, hydrates powders, and reduces microbial load.
- Residence time: Typically 30–120 seconds.
Advantages of Pre-conditioning:
- Improves energy efficiency (extruder does less work).
- Ensures uniform cooking.
- Reduces wear on extruder screws.
- Enhances product digestibility.
Example: Pre-conditioning Parameters
| Ingredient | Steam Temperature | Moisture Level Before Extrusion | Benefits |
|---|---|---|---|
| Corn-based formula | 90–95°C | 18–20% | Good starch gelatinization |
| High-protein formula | 85–90°C | 20–22% | Prevents burn, improves shaping |
| Rice-based formula | 80–85°C | 17–19% | Prevents stickiness, better expansion |
2.3 Extrusion Process Mechanics
Inside the extruder barrel, several key transformations occur:
- Feeding: The conditioned mixture enters the barrel via a screw feeder.
- Conveying: The screws push the material forward under increasing pressure.
- Cooking: Friction and injected steam/heat cook the product (120–160°C).
- Shearing: Mechanical shear disrupts starch granules, denatures proteins, and homogenizes fats.
- Expansion: When the cooked dough exits the die, sudden pressure drop causes water to vaporize, expanding the kibble.
- Shaping: The die determines kibble shape (round, triangular, bone-shaped, etc.).
- Cutting: Rotating knives cut kibbles to the required length.
Typical Extrusion Parameters
| Parameter | Range | Influence on Product |
|---|---|---|
| Barrel Temperature | 120–160°C | Higher → more starch gelatinization, more expansion |
| Moisture Content (pre-exit) | 20–28% | Higher moisture → softer texture, less expansion |
| Screw Speed | 300–600 rpm | Higher speed → more shear, finer texture |
| Die Pressure | 20–40 bar | Higher pressure → denser kibbles |
| Residence Time | 20–60 seconds | Longer → better cooking, but risk of nutrient degradation |
2.4 Kibble Shape and Size Control
One of the unique marketing aspects of pet food is the variety of kibble shapes. Extrusion allows flexibility through interchangeable dies and cutters.
| Kibble Shape | Market Use | Notes |
|---|---|---|
| Round pellets | Standard dog food | Easier to produce, uniform expansion |
| Triangular kibbles | Premium dog/cat food | Increased crunch, differentiation |
| Bone shapes | Snacks & treats | Strong consumer appeal |
| Star/flower shapes | Cat food | Enhances mouthfeel and crunchiness |
Key consideration: Shape must not compromise cooking or drying efficiency. Complex shapes may dry unevenly.
2.5 Energy and Efficiency in Extrusion
Extrusion is energy-intensive, but efficient equipment design can save costs.
Example Energy Use
| Product | Energy Use (kWh/ton) | Notes |
|---|---|---|
| Economy dog kibble | 80–100 | Basic recipe, low fat |
| Premium dog kibble | 110–140 | High meat, complex formulation |
| Cat kibble | 120–150 | Higher protein and fat |
Modern twin-screw extruders with segmented screws allow precise control, reducing waste and lowering kWh/ton.
2.6 Food Safety in Extrusion
Extrusion is not just cooking — it is also a critical kill step in HACCP.
- Pathogens like Salmonella, E. coli are destroyed at >120°C.
- Mycotoxin risks are reduced but not eliminated (binders may still be needed).
- The extruder can be adjusted to ensure compliance with food safety audits.
2.7 Case Study – Darin Machinery Twin-Screw Extruder
One of Darin’s installations in Italy involved replacing a 15-year-old single-screw extruder with a twin-screw extruder DR-65 model.
- Capacity increased from 800 kg/h to 1,500 kg/h.
- Starch gelatinization improved from 85% to 95%.
- Energy use per ton dropped by 12%.
- Product variety expanded from 3 shapes to 10+ shapes with interchangeable dies.
This illustrates how modern extrusion lines increase efficiency and expand market reach.
2.8 Charts for Better Understanding
Chart 1 – Relationship Between Moisture Level and Expansion
Expansion Index (Y-axis)
|
|           *
|        *
|     *
|  *
|___________________________
    14  16  18  20  22  24
       Moisture (%) before extrusion
Interpretation: Higher moisture reduces expansion, producing denser kibble.
Chart 2 – Energy Consumption vs. Output
| Output (kg/h) | Energy Consumption (kWh/ton) |
|---|---|
| 500 | 150 |
| 800 | 120 |
| 1,200 | 110 |
| 1,500 | 100 |
Interpretation: Larger extruders have better energy efficiency at scale.
Step 3: Drying and Cooling in Pet Food Production
Once kibbles or shaped snacks leave the extruder, they contain around 20–28% moisture, depending on the recipe and process parameters. At this level, the product is unstable: it is prone to microbial growth, mold, and spoilage. To ensure long shelf life and product safety, moisture must be reduced to 8–12% (for dry pet food) through a controlled drying and cooling process.
This stage is not just about removing water. It is about achieving moisture uniformity, product stability, and structural integrity. Poor drying can result in cracked kibbles, uneven hardness, or pockets of high moisture that later lead to mold growth. On the other hand, optimized drying and cooling ensures consistent kibble texture, maximizes palatability, reduces energy consumption, and extends storage life.
3.1 The Science of Drying
Drying is essentially controlled evaporation of water from the product using heated air. The key factors are:
- Temperature of drying air (usually 110–150°C in the first zones).
- Air velocity and distribution (to maximize heat and mass transfer).
- Relative humidity of drying air (lower humidity enhances evaporation).
- Time in dryer (typically 15–40 minutes depending on product size).
The goal is to gently but effectively remove moisture without damaging nutrients or structure.
Pet food drying is only about applying high heat to evaporate water quickly.False
Pet food drying must balance air temperature, velocity, humidity, and residence time to avoid nutrient loss, uneven drying, or product cracking.
3.2 Types of Dryers Used in Pet Food
| Dryer Type | Description | Advantages | Limitations |
|---|---|---|---|
| Single-pass belt dryer | One long conveyor belt, hot air blown through product bed | Simple design, continuous operation | May have uneven drying if airflow is poor |
| Multi-pass belt dryer | Several stacked conveyor belts, product passes multiple stages | Better control, more uniform drying | Higher investment |
| Rotary drum dryer | Rotating cylinder with internal flights, product lifted and cascaded | Compact, high throughput | Less precise moisture control |
| Fluidized bed dryer | Hot air suspends and mixes product in a “fluidized” state | Excellent uniformity, efficient heat transfer | Limited to smaller particle products |
For most dry pet food kibbles, multi-pass belt dryers are the industry standard.
3.3 Drying Parameters for Different Pet Foods
| Product Type | Inlet Temp (°C) | Outlet Temp (°C) | Final Moisture (%) | Typical Time |
|---|---|---|---|---|
| Dog kibble | 130–150 | 90–100 | 8–10 | 20–30 min |
| Cat kibble | 120–140 | 85–95 | 8–9 | 15–25 min |
| Dental chews | 100–120 | 70–80 | 10–12 | 25–40 min |
| Treat sticks | 110–130 | 80–90 | 12–14 | 30–40 min |
Note: Cat kibbles usually require tighter moisture tolerances due to smaller size and higher protein levels.
3.4 The Cooling Phase
After drying, kibbles are still warm (70–90°C) and slightly fragile. They must be cooled down to ambient temperature (25–35°C) before fat coating or packaging.
Why cooling is essential:
- Prevents condensation inside bags.
- Ensures structural integrity of kibbles.
- Stabilizes moisture before coating.
Types of coolers used:
- Counter-flow coolers: Air moves opposite to product flow, highly efficient.
- Ambient belt coolers: Simple conveyors with fans, good for lower capacities.
- Fluidized coolers: For uniform, gentle cooling in premium lines.
3.5 Moisture Uniformity and Its Importance
Uniform moisture is more critical than average moisture. For example:
- If average kibble moisture is 9%, but some pieces are at 12%, mold will grow on those pieces.
- Uneven moisture leads to shelf-life failures and recalls.
Target variation: ≤1% difference across kibble samples.
Example – Moisture Distribution Study
| Batch Sample | Moisture Content (%) |
|---|---|
| Kibble 1 | 8.9 |
| Kibble 2 | 9.1 |
| Kibble 3 | 9.0 |
| Kibble 4 | 9.2 |
| Kibble 5 | 9.1 |
→ Uniform.
| Batch Sample | Moisture Content (%) |
|---|---|
| Kibble 1 | 8.0 |
| Kibble 2 | 11.5 |
| Kibble 3 | 9.0 |
| Kibble 4 | 10.8 |
| Kibble 5 | 9.2 |
→ Risk of mold.

3.6 Drying Curves and Control
Drying is typically done in phases (zones):
- Initial high-temperature zone: Rapid moisture removal (surface drying).
- Intermediate zone: Moderate temperature, controlled drying.
- Final zone: Gentle drying to stabilize internal moisture.
Example Drying Curve – Dog Kibble
Moisture (%)
|
|  25 |********
|     |      ****
|  15 |          ***
|     |             **
|  10 |               *
|____________________________
   Zone 1   Zone 2   Zone 3
       Time →
3.7 Energy Efficiency in Drying
Drying consumes 30–40% of total energy in pet food production. Efficiency improvements include:
- Heat recovery systems (recycle exhaust air).
- Insulated dryer housing.
- Variable speed fans for airflow optimization.
Example – Energy Use in Drying
| Dryer Type | Energy Use (kWh/ton) | Efficiency Rating |
|---|---|---|
| Old single-pass dryer | 180–220 | Low |
| Modern multi-pass dryer | 120–150 | Medium |
| Fluidized bed dryer | 100–120 | High |
3.8 Case Study – Darin Multi-pass Dryer Upgrade
A Darin Machinery client in Vietnam upgraded from a 1990s rotary dryer to a modern multi-pass belt dryer:
- Energy use reduced by 30%.
- Moisture variation dropped from ±2% to ±0.5%.
- Shelf-life extended from 8 months to 14 months.
- ROI achieved in less than 18 months.
3.9 Cooling System Design
The final cooling stage must be hygienic, efficient, and gentle:
- Air filtration: Prevents contamination from dust or pests.
- Counter-flow design: Ensures maximum cooling efficiency.
- Retention time: 10–20 minutes typically.
- Temperature control: Final kibble temp ≤5°C above ambient.

Step 4: Coating and Flavoring in Pet Food Production
Once the kibbles have been dried and cooled to a stable moisture level (typically 8–10%), they are structurally sound but nutritionally incomplete. At this stage, fats, palatants, and other functional additives must be applied externally to enhance palatability, energy density, digestibility, and nutritional profile. This is known as the coating stage.
Unlike extrusion or drying, coating does not transform the internal structure of the kibble; rather, it optimizes the surface properties to improve taste, aroma, and nutrient stability. This stage is critical because dogs and cats are highly selective eaters — even nutritionally perfect kibble will fail in the market if pets refuse to eat it.
4.1 The Purpose of Coating
The coating process serves multiple functions:
-
Fat Addition:
- Increases energy density.
- Enhances palatability.
- Supplies essential fatty acids (e.g., omega-3, omega-6).
-
Palatant Application:
- Sprayed flavors (hydrolyzed proteins, liver digest, yeast extracts).
- Drives voluntary intake (“first bite” acceptance and “repeat consumption”).
-
Functional Additives:
- Vitamins, probiotics, enzymes, joint-care supplements (glucosamine, chondroitin).
- Must be added post-extrusion to avoid thermal degradation.
-
Dust Control and Appearance:
- Oil coating reduces fines and improves kibble shine.
Palatants are only added for marketing purposes and have no effect on whether pets eat the food.False
Palatants significantly influence a pet’s willingness to consume food, affecting both acceptance and long-term consumption rates.
4.2 Types of Coating Systems
| Coating System | Description | Applications | Advantages | Limitations |
|---|---|---|---|---|
| Rotary Drum Coater | Kibbles tumble in a rotating drum, liquids sprayed inside | Basic fat + flavor addition | Simple, low cost | Limited penetration, uneven coating if overloaded |
| Vacuum Coater | Kibbles placed in sealed chamber, vacuum draws liquid into pores | Premium kibble and functional diets | Deep penetration, uniform fat absorption | Higher cost, slower throughput |
| Spray Cabinet/Conveyor Coater | Kibbles travel on belt, nozzles spray oils/powders | Snacks, treats, basic pet food | Easy to integrate, continuous operation | Surface-only coating, limited absorption |
For premium dry pet foods, vacuum coating has become the gold standard.
4.3 Fat Application
Fats are typically sprayed in liquid form:
- Animal fats: Poultry fat, beef tallow, fish oil.
- Vegetable oils: Sunflower, soybean, rapeseed.
- Special oils: DHA-rich fish oil, algal oils for brain health.
Dosage range:
- Economy kibble: 5–8% fat coating.
- Premium kibble: 10–15% fat coating.
Example – Fat Coating Parameters
| Fat Type | Temp for Spraying | Dosage (%) | Notes |
|---|---|---|---|
| Poultry fat | 50–60°C | 5–10 | Stable, economical |
| Fish oil | 30–40°C | 2–5 | Highly palatable, prone to oxidation |
| Mixed vegetable oil | 40–50°C | 5–8 | Balanced fatty acid profile |
Antioxidants (BHA, BHT, tocopherols) are often added to prevent rancidity.
4.4 Palatant Coating
Palatants are flavor enhancers applied as dry powders or liquid sprays.
- Animal digest sprays: Hydrolyzed chicken, liver, pork plasma.
- Yeast extracts: Enhance umami, improve aroma.
- Herbal/botanical extracts: Used in natural or functional diets.
Example – Palatant Application
| Palatant | Dosage Range | Function |
|---|---|---|
| Hydrolyzed chicken liver | 1–3% | Strong aroma, high acceptance in dogs |
| Yeast extract | 0.5–1% | Improves taste and digestibility |
| Spray-dried plasma | 0.5–2% | Boosts protein quality and flavor |
Key metric: Palatability panel tests (“two-pan tests”) measure preference between coated products. A 65:35 preference ratio is considered strong acceptance.
4.5 Vacuum Coating – Technical Details
Vacuum coating allows fats and liquids to penetrate deep into kibble pores, unlike drum coating which only covers the surface.
Process steps:
- Place cooled kibbles in vacuum chamber.
- Apply vacuum → air inside kibble pores is evacuated.
- Spray fat and liquid additives.
- Release vacuum → atmospheric pressure forces liquid deep inside pores.
- Optional second stage for palatant spraying.
Benefits:
- Better nutrient stability.
- Higher liquid inclusion possible (up to 20%).
- More uniform product, less surface greasiness.
4.6 Functional Additives at Coating Stage
Many heat-sensitive nutrients cannot survive extrusion temperatures. They must be added post-extrusion:
- Vitamins A, E, C – sensitive to heat and oxygen.
- Probiotics – added in encapsulated form.
- Joint health additives – glucosamine, chondroitin.
- Omega oils – DHA, EPA for brain and skin health.
Example – Additives via Coating
| Additive | Typical Dosage | Application Notes |
|---|---|---|
| Vitamin E | 200–500 IU/kg | Antioxidant, must be surface-coated |
| Glucosamine | 300–500 mg/kg | Functional diets for senior pets |
| Probiotics | 1–5×10^9 CFU/kg | Must be microencapsulated |
| Omega-3 oil | 0.5–2% | Sensitive to oxidation, vacuum-coated |
4.7 Quality Control in Coating
Critical factors monitored:
- Fat absorption efficiency.
- Coating uniformity (visual and lab test).
- Palatant dosage accuracy.
- Peroxide value of fats.
Sampling is done every 30–60 minutes to ensure coating stability.
4.8 Case Study – Darin Vacuum Coater Installation
A Darin Machinery client in Germany upgraded from a drum coater to a vacuum coating system:
- Fat inclusion increased from 8% to 14% without surface greasiness.
- Palatability scores improved from 55:45 to 70:30 preference.
- Shelf life extended by 3 months due to reduced oxidation.
- ROI achieved in under 2 years due to higher sales of premium kibble.
4.9 Charts and Tables
Chart 1 – Effect of Coating Method on Fat Absorption
Fat Absorption (%)
|
| 90 |                    *
| 80 |          *
| 70 |  *
|____________________________
   Drum   Spray   Vacuum
→ Vacuum coating achieves the highest absorption.
Chart 2 – Palatability Scores in Two-Pan Tests
| Coating Type | Preference Ratio (Test vs. Control) |
|---|---|
| Drum Coated | 55:45 |
| Spray Coated | 60:40 |
| Vacuum Coated | 70:30 |
Step 5: Packaging and Quality Assurance in Pet Food Production
After coating and flavoring, the pet food is nutritionally complete, palatable, and ready for the market. However, the product is still vulnerable to oxidation, microbial contamination, moisture uptake, and mechanical damage if not properly packaged. Packaging is not just the last step — it is the critical safeguard that ensures the product remains fresh, appealing, and safe throughout its shelf life. Alongside packaging, rigorous quality assurance (QA) and quality control (QC) systems ensure that every batch meets nutritional, safety, and regulatory standards.
5.1 Functions of Packaging in Pet Food
Packaging in pet food has four main roles:
-
Protection:
- Against oxygen → prevents fat rancidity.
- Against moisture → prevents mold and texture changes.
- Against light → reduces vitamin degradation.
- Against pests → ensures hygiene.
-
Preservation:
- Extends shelf life from a few weeks (unprotected) to 12–24 months.
- Maintains flavor and palatability.
-
Communication:
- Provides labeling for regulations (ingredient list, guaranteed analysis, feeding guidelines).
- Displays brand and marketing messages to influence purchase.
-
Convenience:
- Easy-to-carry bags, resealable zippers, portioned pouches.
Packaging in pet food production is mainly for marketing aesthetics.False
Packaging primarily serves as a protective barrier against oxygen, moisture, and contamination, ensuring safety and shelf-life stability.
5.2 Types of Pet Food Packaging
| Packaging Type | Description | Typical Use | Shelf Life | Advantages | Limitations |
|---|---|---|---|---|---|
| Multi-layer plastic bags | Laminated plastic with oxygen barriers | Dry kibble (1–20 kg) | 12–18 months | Lightweight, resealable | Environmental concerns |
| Paper bags with inner liner | Kraft paper with PE or aluminum inner | Economy kibble (10–20 kg) | 6–12 months | Low cost, eco-friendly look | Lower barrier properties |
| Cans | Tinplate or aluminum, hermetically sealed | Wet food | 18–36 months | Sterile, long shelf life | Heavy, higher cost |
| Pouches (retort) | Multi-layer plastic/aluminum pouches | Wet food, treats | 12–24 months | Lightweight, consumer-friendly | High production cost |
| Trays/Cups | Plastic trays sealed with foil lids | Single-serve wet food | 12–24 months | Convenient, portion control | Shorter shelf life than cans |
| Bulk bags (super sacks) | 500–1000 kg woven bags | Pet food premixes, bulk feed | 3–6 months | Industrial use | Not for retail |
5.3 Packaging Technologies
-
Vertical Form Fill Seal (VFFS):
- Most common for kibble.
- Creates pillow or gusseted bags.
- Automated weighing + filling + sealing.
-
Horizontal Form Fill Seal (HFFS):
- Used for pouches and sachets.
- More complex, supports zippers, spouts.
-
Can Filling and Seaming Lines:
- Specialized for wet pet food.
- Requires retort sterilization after filling.
-
Vacuum and Modified Atmosphere Packaging (MAP):
- Removes oxygen or replaces with nitrogen/CO₂.
- Extends shelf life of fatty or premium products.
5.4 Shelf Life Considerations
Shelf life depends on product type, fat level, packaging, and storage conditions.
| Product Type | Typical Shelf Life | Packaging Requirement |
|---|---|---|
| Dry kibble, economy | 8–12 months | Multi-layer bags with antioxidants |
| Dry kibble, premium | 12–18 months | Barrier bags + nitrogen flushing |
| Wet canned food | 18–36 months | Hermetic cans, retort sterilization |
| Wet pouch food | 12–24 months | Retort pouches |
| Semi-moist treats | 6–12 months | MAP pouches with preservatives |
5.5 Quality Control (QC) in Packaging
At the packaging stage, QC focuses on:
- Seal integrity: Prevents oxygen or moisture entry.
- Oxygen testing: Residual oxygen <2% is target for premium kibble.
- Leak detection: Vacuum chamber tests for leaks.
- Label accuracy: Regulatory compliance with guaranteed analysis and feeding instructions.
5.6 Quality Assurance (QA) in the Overall Production
QA in pet food production covers the entire process from raw materials to final shipment. It follows HACCP (Hazard Analysis and Critical Control Points) and ISO 22000/FSMA/FSSC 22000 frameworks.
Key QA elements:
-
Nutritional Consistency:
- Each batch tested for crude protein, fat, fiber, ash, moisture.
- Tighter tolerance for premium brands (±2% vs. ±5%).
-
Microbiological Safety:
- Salmonella, E. coli, mold counts monitored.
- Zero tolerance policy in many markets.
-
Chemical Safety:
- Mycotoxins, pesticides, heavy metals tested.
- Limits based on EU/FDA standards.
-
Traceability:
- Batch coding and record keeping.
- Every bag traceable back to raw material lot.
5.7 Case Study – Darin Automated Packaging Line
A Darin Machinery client in South America upgraded from manual bagging to a fully automated VFFS line with nitrogen flushing:
- Labor reduced from 12 workers to 3 operators.
- Shelf life extended from 9 months to 16 months.
- Packaging defects reduced by 90%.
- Increased export readiness due to compliance with EU standards.
5.8 Charts and Tables
Chart 1 – Impact of Oxygen on Shelf Life of Dry Kibble
Shelf Life (Months)
|
| 18 |           *
| 12 |     *
|  6 |  *
|___________________________
   10% O₂   5% O₂   <2% O₂
→ Lower residual oxygen significantly extends shelf life.
Chart 2 – QC Testing Protocols by Stage
| Production Stage | Key QC Tests | Frequency |
|---|---|---|
| Raw material reception | Moisture, protein, toxins | Every batch |
| Extrusion | Cooking temp, kibble density | Hourly |
| Drying | Moisture uniformity | Hourly |
| Coating | Fat level, palatant dosage | Hourly |
| Packaging | Oxygen level, seal integrity | Hourly |
5.9 Global Regulatory Standards for Pet Food
| Region | Main Authority | Key Standards |
|---|---|---|
| USA | FDA + AAFCO | Labeling, nutrient profiles, FSMA |
| EU | EFSA + FEDIAF | Hygiene package, additives, traceability |
| China | MARA + GB Standards | Ingredient approval, safety testing |
| Brazil | MAPA | Local formulations and registrations |
| Middle East | GCC Standards | Labeling, halal certification in some cases |
Compliance is mandatory for global exports.
5.10 End-to-End Process Overview
Now that we’ve covered all five stages in detail, here’s a final summary flow:
- Raw Material Reception & Storage → Sourcing, grinding, mixing.
- Extrusion & Forming → Cooking, shaping, kibble structure.
- Drying & Cooling → Moisture reduction, shelf life stability.
- Coating & Flavoring → Fats, palatants, functional additives.
- Packaging & QA → Barrier protection, labeling, compliance.
Wrapping It Up in Plain Language
Producing pet food is far more than just mixing ingredients and cooking them. It is a carefully engineered process involving advanced machinery, scientific formulation, strict safety standards, and global compliance requirements. Each step — from raw materials to packaging — contributes to whether a kibble is safe, tasty, nutritious, and profitable.
Talk to Us About Your Pet Food Project
At Darin Machinery, we specialize in complete pet food production lines, including extruders, dryers, coaters, and packaging systems. Whether you’re a startup entering the market or a large-scale manufacturer expanding capacity, our engineering team can design, install, and support a system tailored to your needs.
👉 Contact us today at darin4@darin.cn or visit https://petreatsmachine.com/ to discuss your project and get expert advice on building a world-class pet food factory.