
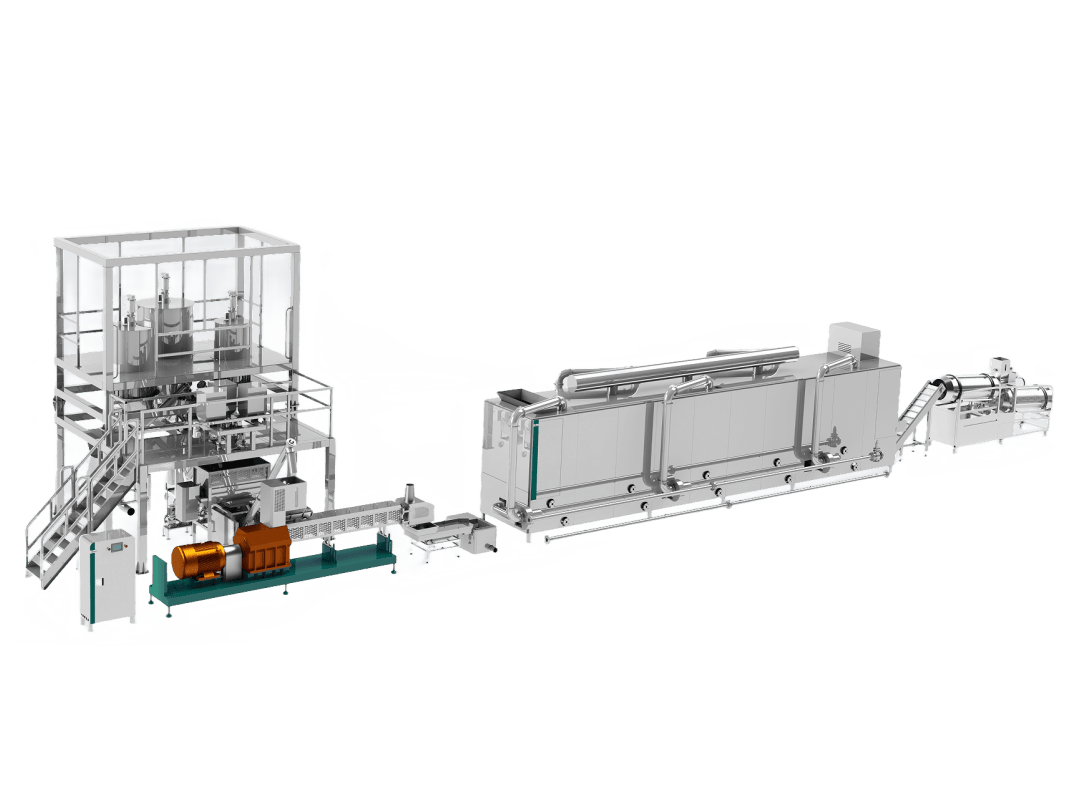
Making dog kibble may appear straightforward, but it is in fact a highly controlled industrial process. Many pet food startups face problems such as unstable product quality, poor digestibility, contamination risks, or high production costs. These issues can quickly erode profits and damage brand reputation. The solution lies in adopting a systematic, step-by-step production process with the right machinery, nutritional formulations, and quality control standards. By doing so, manufacturers can produce consistent, safe, and nutritionally balanced kibble that meets both regulatory requirements and consumer expectations.
Dog kibble is made by selecting high-quality raw ingredients, grinding and mixing them into a balanced formula, cooking and shaping them through extrusion, drying to the correct moisture level, and finally coating and packaging them for shelf stability and palatability.
This guide provides a detailed, technical, and practical roadmap for manufacturers who want to enter or expand within the pet food industry. Each step reflects the expertise of Darin Machinery, a leading global supplier of dog kibble production lines, and is backed by real industry data, process control standards, and customer success cases.
Dog kibble is just baked flour and meat shaped into pellets.False
Dog kibble requires extrusion cooking under controlled temperature and pressure to gelatinize starch, denature proteins, and eliminate pathogens, which simple baking cannot achieve.
Before we dive into equipment and automation, we must start with the foundation: ingredient selection and preparation. Without the right raw materials, no technology can produce high-quality kibble.
Step 1: Ingredient Selection and Preparation
The nutritional quality, safety, and market acceptance of dog kibble begin with the ingredients chosen. This step is crucial because it determines not only the final product’s taste and digestibility but also compliance with global standards such as AAFCO (Association of American Feed Control Officials), FEDIAF (European Pet Food Industry Federation), and national feed regulations.
1.1 Core Ingredient Categories
| Ingredient Type | Examples | Function in Kibble | Typical Inclusion Rate (%) |
|---|---|---|---|
| Protein Sources | Chicken meal, beef meal, fish meal, soybean meal, pea protein | Builds muscle, supports immune system | 20–35% |
| Carbohydrates & Starches | Corn, wheat, rice, potato, cassava | Energy source, extrusion expansion | 30–50% |
| Fats & Oils | Poultry fat, fish oil, vegetable oil | Energy, palatability, essential fatty acids | 8–18% |
| Fiber Sources | Beet pulp, cellulose, pea fiber | Digestive health, stool quality | 2–8% |
| Vitamins & Minerals | Premixes (Ca, P, Zn, Fe, vitamins A–E) | Balance nutritional requirements | <2% |
| Additives & Palatants | Flavors, probiotics, antioxidants | Improve taste, shelf-life, gut health | 0.1–1% |
1.2 Protein Selection
High-quality protein is the cornerstone of dog nutrition. Animal proteins such as chicken meal or fish meal are highly digestible and biologically appropriate, while plant proteins like soy and pea protein are often added for cost efficiency. Darin Machinery’s clients often blend both sources to balance amino acid profiles and cost control.
- Key Specification: Crude protein content should be 20–30% minimum.
- Digestibility Index: Aim for >80% true digestibility for premium kibble.
1.3 Carbohydrates and Starch Role
Carbohydrates are not just “fillers.” In extrusion, starch acts as the structural backbone. When gelatinized, it expands and creates the crunchy kibble texture. Without sufficient starch, extrudate expansion is limited, leading to hard or dense kibble.
- Target Gelatinization: 80–95% for optimal expansion.
- Preferred Sources: Rice (digestibility), corn (availability), cassava (cost efficiency).
1.4 Fat and Oil Management
Fats contribute to taste, energy, and nutrient absorption. They are usually added both in the premix and after extrusion during coating. However, fat oxidation is a risk. Manufacturers must use antioxidants (natural: tocopherols; synthetic: BHA/BHT) and apply nitrogen flushing in packaging.
1.5 Fiber and Functional Ingredients
Fiber helps regulate digestion and stool consistency. Prebiotics (FOS, MOS) and probiotics may be added for gut health. Functional additives such as glucosamine or omega-3 are common in premium kibble for joint and skin support.
1.6 Ingredient Quality Control
To ensure consistency, manufacturers implement raw material testing upon arrival:
| Test | Purpose | Method | Acceptance Range |
|---|---|---|---|
| Moisture | Prevent spoilage | Oven drying | <12% |
| Protein | Nutritional value | Kjeldahl/Infrared | As per formulation |
| Aflatoxin | Safety | HPLC/Rapid test kits | <20 ppb |
| Salmonella | Safety | Culture/PCR | Must be absent |
Dog kibble can use any type of raw material without testing.False
Every ingredient must pass strict quality control tests for moisture, protein, toxins, and pathogens to ensure safety and compliance with feed standards.
1.7 Ingredient Storage and Handling
Raw materials must be stored in a clean, dry, pest-free warehouse with temperature control. Protein meals are prone to rancidity, so first-in-first-out (FIFO) inventory management is critical.
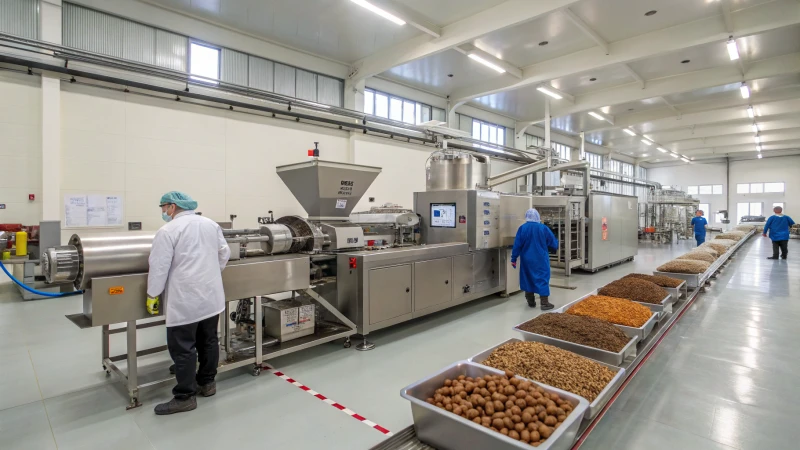
After selecting and preparing raw materials, the next critical step is grinding and mixing. This stage ensures uniform particle size, proper blending of nutrients, and optimal conditions for extrusion. Many small-scale manufacturers underestimate this step, leading to inconsistent kibble texture, nutrient segregation, and lower digestibility.
Grinding and mixing in dog kibble production involves reducing raw ingredients into fine, uniform particles using a hammer mill or pulverizer, then blending them in high-capacity mixers to achieve a homogeneous feed mix before extrusion.
By mastering this stage, manufacturers can guarantee stable kibble expansion, palatability, and nutritional consistency in every batch.
Dog kibble ingredients can be used directly without grinding.False
Large or uneven particles cause poor mixing, blockages in the extruder, and inconsistent kibble quality. Grinding ensures uniform particle size and improved digestibility.
Step 2: Grinding and Mixing
2.1 Grinding – Particle Size Reduction
The grinding stage uses hammer mills, pin mills, or pulverizers to crush raw materials (grains, proteins, fibers) into uniform powder.
- Target Particle Size: 0.2–0.6 mm for grains, 0.3–0.8 mm for proteins.
-
Importance:
- Enhances starch gelatinization in extrusion.
- Improves digestibility (smaller particles expose more surface area).
- Prevents segregation during mixing.
- Energy Efficiency: Finer grinding consumes more energy; balance between efficiency and functionality is key.
| Equipment | Typical Capacity | Key Features | Advantages |
|---|---|---|---|
| Hammer Mill | 1–10 T/h | High-speed rotating hammers | Robust, versatile |
| Pin Mill | 0.5–5 T/h | Pins and plates | Fine, consistent particles |
| Pulverizer | 0.3–2 T/h | Ultra-fine grinding | Premium kibble formulas |
Case Insight: Darin Machinery recommends hammer mills for standard kibble and pulverizers for specialized diets (e.g., puppy or medical kibble) where very fine particles are essential.
2.2 Mixing – Achieving Homogeneity
Once ground, ingredients are transferred to horizontal ribbon mixers, paddle mixers, or double-shaft mixers.
- Mixing Uniformity: Coefficient of Variation (CV) should be ≤5% for premium kibble.
- Mixing Time: Typically 2–5 minutes depending on capacity.
- Moisture Addition: Up to 3% water or steam can be added during mixing to aid extrusion later.
| Mixer Type | Batch Capacity | Mixing Accuracy | Application |
|---|---|---|---|
| Ribbon Mixer | 500–3000 kg/batch | CV ≤ 7% | General kibble production |
| Paddle Mixer | 250–2000 kg/batch | CV ≤ 5% | High accuracy, premium kibble |
| Double-Shaft Mixer | Continuous flow | CV ≤ 3% | Large-scale automation |
Mixing longer always results in better kibble quality.False
Over-mixing can cause ingredient segregation, nutrient degradation, and energy waste. Optimal mixing time is carefully controlled.
2.3 Pre-conditioning (Optional but Recommended)
In advanced kibble plants, a pre-conditioner may be installed before extrusion. This allows controlled addition of steam and liquids to the mixed formula, starting starch gelatinization and protein denaturation early.
-
Benefits:
- Increases extruder efficiency.
- Improves kibble expansion and texture.
- Enhances digestibility and palatability.
Typical Parameters:
- Moisture addition: 5–10%
- Steam pressure: 1–3 bar
- Retention time: 30–120 seconds
2.4 Process Flow for Grinding & Mixing
Raw Materials → Hammer Mill → Ground Powder → Mixer → Homogeneous Mix → Pre-conditioner (optional) → Extruder2.5 Quality Control in Grinding & Mixing
To guarantee uniformity, the following tests are performed:
| Test | Method | Target Standard |
|---|---|---|
| Particle Size Distribution | Sieve Analysis | 90% passing 0.6 mm sieve |
| Mixing Homogeneity | Salt Marker Test | CV ≤ 5% |
| Moisture Content | Oven Drying | 8–12% before extrusion |
Practical Tip from Darin Engineers: Always calibrate mixer load cells and perform homogeneity testing weekly to avoid “hidden variability” in production.
Once the raw materials are ground and mixed, they are ready for extrusion cooking—the critical process that transforms powdered feed mix into fully cooked, expanded, and shaped kibble. This stage is often called the “engine room” of a pet food factory because it determines texture, density, digestibility, safety, and even shelf life.
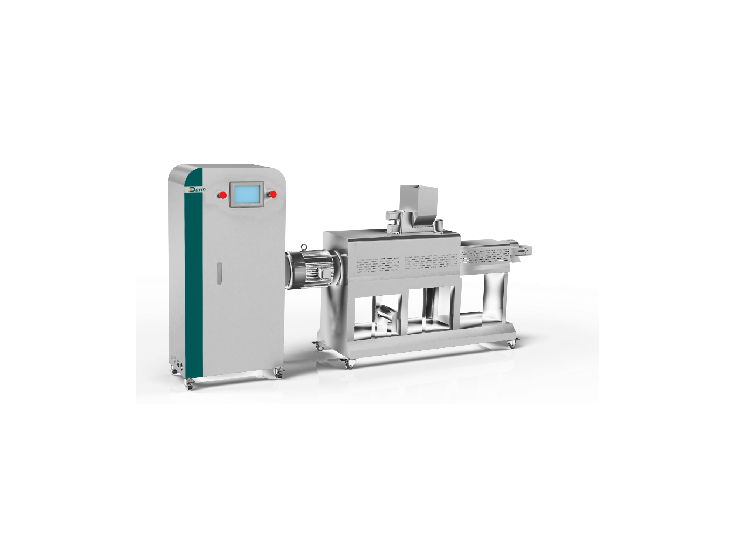
Extrusion in dog kibble manufacturing involves cooking the ingredient mix under controlled heat, pressure, and mechanical shear inside a twin-screw extruder, shaping it through a die plate, and cutting it into uniform kibble sizes.
By mastering extrusion, manufacturers can control kibble expansion, density, and palatability while ensuring food safety and compliance with nutritional standards.
Dog kibble extrusion is only for shaping and not for cooking.False
Extrusion simultaneously cooks, sterilizes, gelatinizes starch, and denatures protein, ensuring both nutritional quality and food safety.
Step 3: Extrusion Cooking
3.1 Extrusion Principle
In extrusion, the mixed powder enters the extruder barrel, where rotating screws convey it forward. As it moves:
- Friction, pressure, and steam injection rapidly heat the material.
- Starch gelatinization (80–95%) occurs, which creates structure and expansion.
- Protein denaturation improves digestibility.
- Microbial kill step eliminates Salmonella and other pathogens.
- The hot mass is forced through a die plate, cut by rotating knives into kibble shapes.
3.2 Extruder Types
| Extruder Type | Features | Advantages | Applications |
|---|---|---|---|
| Single-Screw Extruder | One rotating screw, simpler design | Lower cost, lower maintenance | Small-scale production, limited formula flexibility |
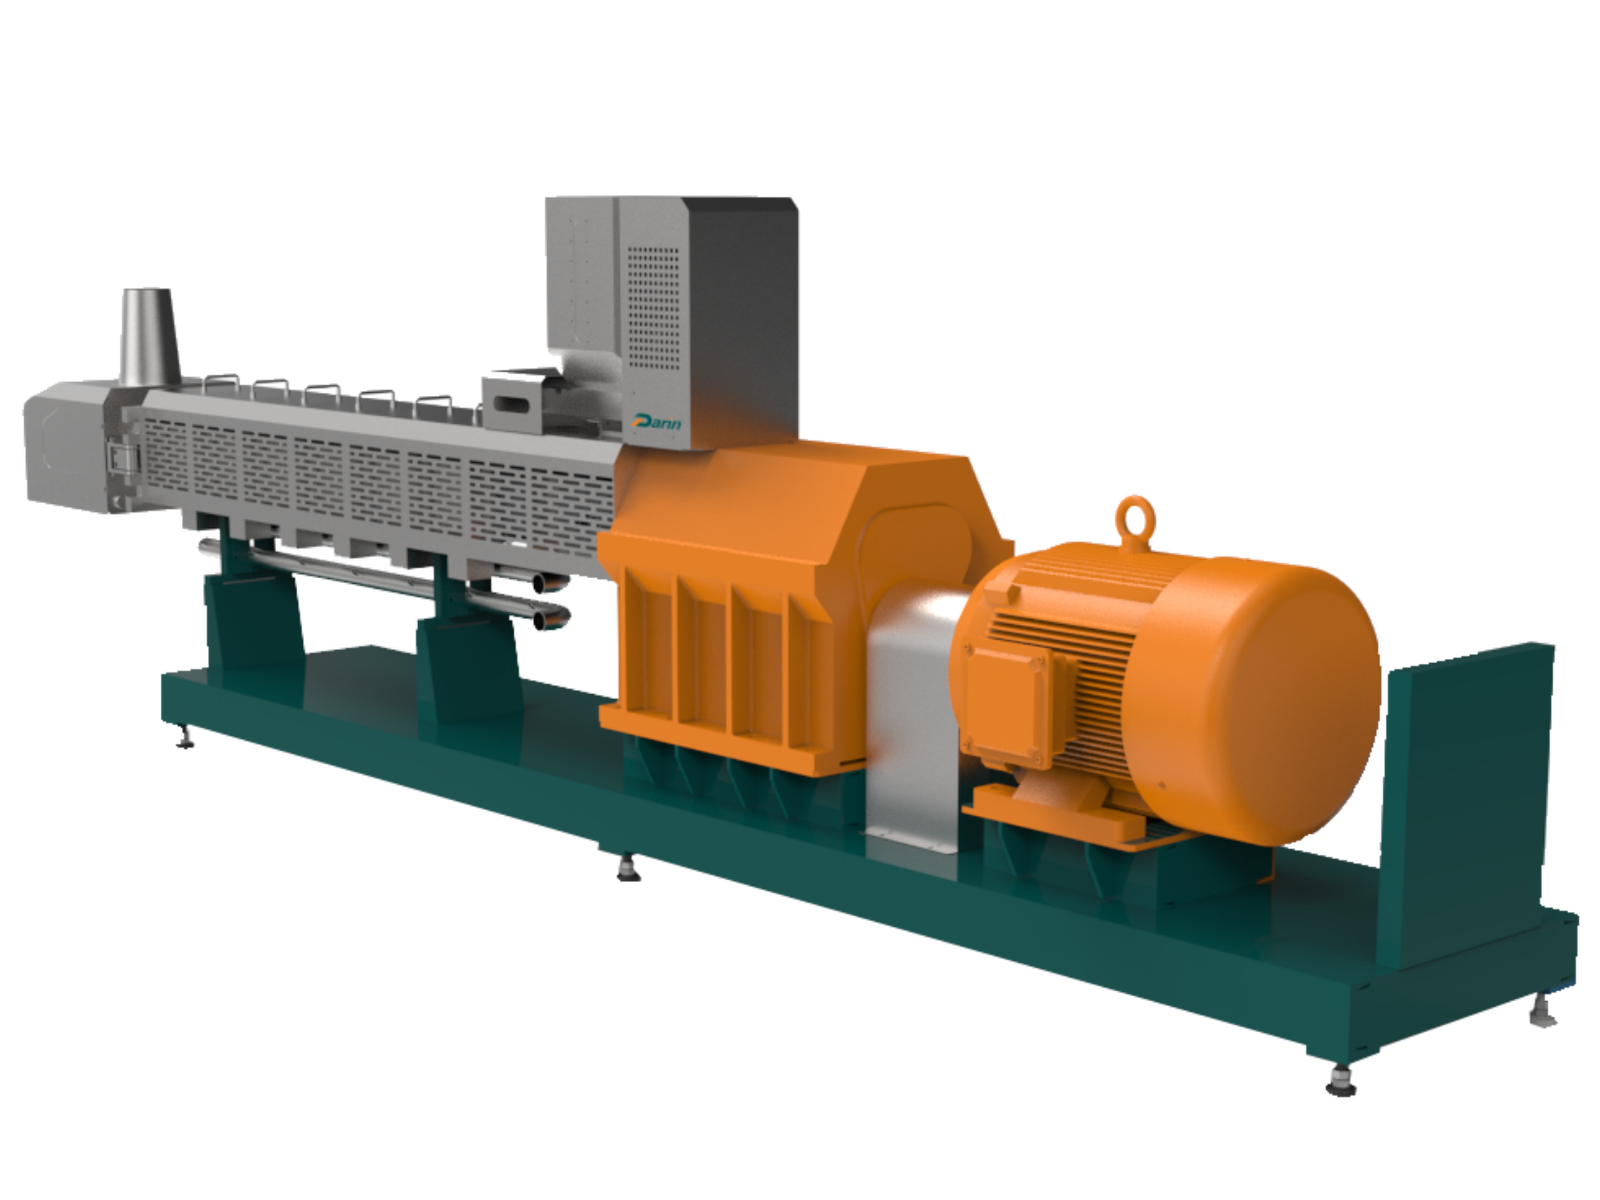
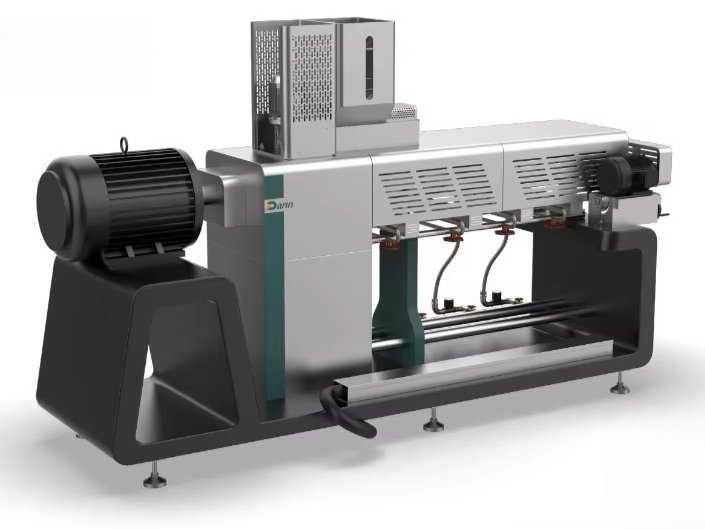
| Twin-Screw Extruder | Two intermeshing screws, co-rotating | High flexibility, better mixing, wider recipes, consistent quality | Medium to large-scale kibble factories, premium pet food |
Darin Machinery primarily recommends twin-screw extruders for kibble due to their versatility, efficiency, and superior product quality.
3.3 Key Extrusion Parameters
Precise control of parameters is crucial:
| Parameter | Typical Range | Effect on Kibble |
|---|---|---|
| Barrel Temperature | 90–160°C | Higher = more cooking, softer texture |
| Pressure | 20–40 bar | Controls expansion and density |
| Screw Speed | 200–500 rpm | Influences mixing, shear, throughput |
| Moisture Content | 20–30% | Balances expansion and shape |
| Retention Time | 20–60 sec | Ensures complete cooking |
Golden Rule: High starch diets require higher temperatures, while high-protein diets demand more controlled cooking to prevent nutrient loss.
3.4 Kibble Shaping
The extruder die determines the shape and size of kibble. Shapes include:
- Round
- Triangular
- Bone-shaped
- Multi-hole (for smaller dogs/puppies)
Die design considerations:
- Hole diameter (5–15 mm depending on dog size)
- Hole geometry (cylindrical vs tapered)
- Knife speed (controls kibble length)
3.5 Extruder Output and Capacity
| Machine Model | Screw Diameter | Throughput (kg/h) | Application |
|---|---|---|---|
| DR-65 | 65 mm | 150–250 kg/h | Startups, pilot plants |
| DR-70 | 70 mm | 250–400 kg/h | Small-medium factories |
| DR-85 | 85 mm | 500–1000 kg/h | Medium-large production |
| DR-95 | 95 mm | 1,000–2,000 kg/h | Large-scale commercial plants |
Data example from Darin Machinery’s dog food extruder line.
3.6 Process Flow of Extrusion
Mixer → Pre-conditioner (optional) → Extruder Barrel (twin-screw) → Die Plate → Rotary Cutter → Fresh Kibble3.7 Energy and Efficiency
Extruders are designed for energy-efficient cooking:
- Steam injection reduces electrical heating costs.
- Twin-screw systems provide higher throughput with lower energy per ton.
- Automation allows precise recipe adjustments with minimal downtime.
3.8 Quality Control in Extrusion
| Test | Purpose | Standard |
|---|---|---|
| Starch Gelatinization | Ensures digestibility | >85% |
| Density | Controls float/sink (important for aquatic feeds, sometimes used in dog treats) | 300–450 g/L |
| Pathogen Elimination | Ensures safety | 100% Salmonella-free |
| Shape Consistency | Consumer appeal | >95% uniformity |
Tip from Darin Engineers: Keep a spare die plate and knife set on-site; downtime from wear-and-tear can cost thousands per hour.

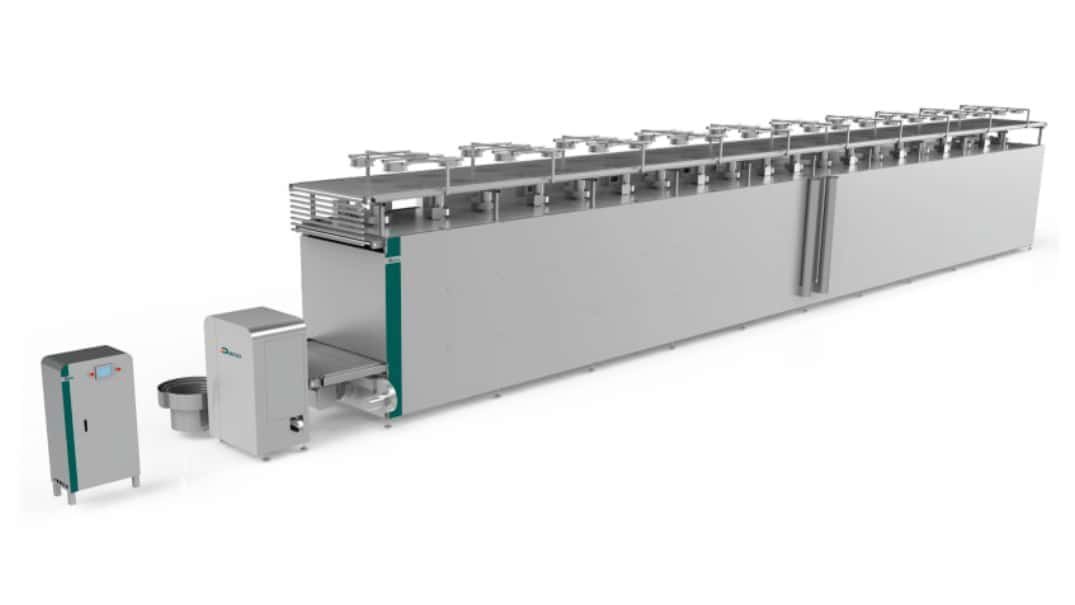
Freshly extruded kibble contains about 20–25% moisture, which makes it unstable and prone to mold growth, rancidity, and microbial contamination. Without proper drying, the kibble cannot be stored, transported, or sold safely. Many pet food factories underestimate drying, leading to uneven products—burnt on the outside but damp inside—which results in recalls or consumer complaints.
Drying in dog kibble production involves reducing moisture from 20–25% to a safe level of 8–10% using controlled hot air circulation in multi-layer belt dryers or fluidized bed dryers, ensuring stability, safety, and long shelf life.
This stage is critical for both food safety and economic efficiency, as over-drying wastes energy and reduces palatability, while under-drying risks spoilage.
Dog kibble can be safely stored without drying after extrusion.False
Freshly extruded kibble has high moisture content (20–25%), which promotes microbial growth. Drying to 8–10% moisture is essential for safety and shelf stability.
Step 4: Drying
4.1 Purpose of Drying
- Reduce moisture content → Target: 8–10%.
- Inhibit microbial growth → Mold, Salmonella, and bacteria thrive in moist conditions.
- Extend shelf life → Dry kibble lasts 12–18 months when packaged correctly.
- Improve handling → Dry kibble flows better during coating, cooling, and packaging.
4.2 Dryer Types for Dog Kibble
| Dryer Type | Description | Advantages | Limitations |
|---|---|---|---|
| Multi-Layer Belt Dryer | Continuous dryer with several mesh layers where kibble moves slowly under hot air | High efficiency, large capacity, even drying | Large footprint, higher initial cost |
| Single-Pass Conveyor Dryer | One-layer conveyor with hot air circulation | Compact, easier cleaning | Less uniform than multi-layer |
| Fluidized Bed Dryer | Kibble floats on hot air, drying quickly | Fast heat transfer, gentle drying | Higher energy consumption |
| Rotary Drum Dryer | Rotating cylinder tumbles kibble while hot air passes through | Robust, flexible | May damage delicate shapes |
Industry Standard: Darin Machinery integrates multi-layer belt dryers into most kibble lines because they ensure consistent drying across large batches.
4.3 Drying Parameters
| Parameter | Typical Range | Effect |
|---|---|---|
| Inlet Air Temperature | 120–160°C | Higher = faster drying, but risk of burning |
| Outlet Air Temperature | 60–80°C | Prevents overdrying at the end |
| Retention Time | 15–45 minutes | Longer time for larger kibble |
| Final Moisture | 8–10% | Shelf-stable and safe |
| Relative Humidity | 10–20% | Controls drying gradient |
Tip: Always dry gradually—rapid drying can cause case hardening (outside hard, inside moist).
4.4 Energy Efficiency in Drying
Drying consumes 30–40% of total energy in kibble production. Modern dryers use:
- Heat recovery systems → recycle hot air.
- Moisture sensors → adjust drying automatically.
- Insulated chambers → minimize heat loss.
Darin Machinery dryers include PLC-controlled airflow and moisture monitoring, ensuring energy savings of up to 15–20% compared to conventional systems.
4.5 Moisture Testing Methods
| Test Method | Equipment | Accuracy | Frequency |
|---|---|---|---|
| Oven Drying | Lab oven | ±0.1% | Daily |
| Infrared Moisture Meter | Infrared analyzer | ±0.2% | Real-time |
| NIR (Near-Infrared) | Inline sensor | ±0.1% | Continuous |
Standard: Final kibble must be 8–10% moisture, with <0.5% batch-to-batch variation.
4.6 Process Flow of Drying
Extruded Kibble → Multi-layer Belt Dryer → Controlled Hot Air → Uniform Moisture Reduction → 8–10% Final Moisture4.7 Troubleshooting Drying Issues
| Issue | Cause | Solution |
|---|---|---|
| Case Hardening | Too high inlet temperature | Lower inlet temp, extend retention time |
| Over-dried Kibble | Long drying time | Reduce air flow or belt speed |
| Uneven Moisture | Poor air circulation | Check fans and layer loading |
| High Energy Cost | Inefficient system | Install heat recovery, upgrade controls |
Over-dried kibble is better because it prevents spoilage completely.False
Over-drying wastes energy, reduces palatability, and makes kibble brittle. Optimal drying is 8–10% moisture.
After extrusion and drying, kibble is stable but still relatively bland and nutritionally incomplete. Dogs are highly selective eaters, and palatability is a key driver of repeat purchases. To meet consumer expectations, kibble undergoes spraying and coating, where fats, oils, vitamins, minerals, and flavor enhancers are applied. This stage is the final opportunity to add sensitive ingredients (like omega-3 oils or probiotics) that cannot survive high-temperature extrusion.
Spraying and coating in dog kibble production involves applying fats, oils, vitamins, minerals, and palatants onto dried kibble using drum coaters or vacuum coaters, improving palatability, energy density, and nutritional value.
By controlling this stage, manufacturers ensure kibble is not only safe and stable but also appealing in taste and smell, which directly impacts sales performance.
Spraying and coating is optional and does not affect dog kibble quality.False
Coating is essential for palatability, energy enrichment, and adding heat-sensitive nutrients like vitamins and probiotics. Without coating, kibble is bland and nutritionally incomplete.
Step 5: Spraying and Coating
5.1 Objectives of Coating
- Enhance palatability → Dogs prefer kibble with surface fats and aromas.
- Increase energy density → Coating oils boost caloric content.
- Deliver heat-sensitive nutrients → Vitamins, probiotics, and omega fatty acids.
- Improve appearance → Uniformly coated kibble looks more premium.
5.2 Coating Methods
| Method | Description | Advantages | Applications |
|---|---|---|---|
| Drum Coating (Atmospheric) | Kibble tumbles in a rotating drum while liquid is sprayed | Simple, cost-effective | Standard kibble lines |
| Vacuum Coating | Kibble placed under vacuum, liquid penetrates into pores | Deep penetration, uniform coating, higher loading | Premium kibble, functional diets |
| Electrostatic Spraying | Uses charged particles to improve coating adhesion | Reduces waste, precise application | Research & specialty lines |
Industry Trend: Vacuum coating is becoming the gold standard for high-quality kibble, especially in export markets, due to its ability to evenly infuse oils and sensitive additives.
5.3 Typical Coating Ingredients
| Category | Examples | Function |
|---|---|---|
| Fats & Oils | Poultry fat, fish oil, flaxseed oil | Energy, palatability, omega fatty acids |
| Vitamins | A, D, E, K, B-complex | Essential micronutrients |
| Minerals | Calcium, zinc, selenium | Health and bone development |
| Palatants | Digest sprays, liver hydrolysates | Aroma and flavor enhancers |
| Functional Additives | Probiotics, glucosamine, antioxidants | Gut health, joint support, shelf stability |
5.4 Coating Parameters
| Parameter | Typical Range | Effect |
|---|---|---|
| Oil Addition | 3–10% of kibble weight | Higher = richer flavor, higher energy |
| Vitamin/Mineral Premix | 0.5–2% | Completes nutritional profile |
| Drum Speed | 3–15 rpm | Uniform coverage |
| Vacuum Pressure (if used) | -0.6 to -0.9 bar | Ensures deep penetration |
| Application Time | 2–5 minutes | Depends on recipe |
Tip: Apply antioxidants (e.g., mixed tocopherols) along with fats to prevent rancidity.
5.5 Process Flow of Coating
Dried Kibble (8–10% moisture) → Drum/Vacuum Coater → Fat & Oil Spraying → Vitamin/Mineral Addition → Palatant Application → Uniformly Coated Kibble5.6 Equipment Examples
| Equipment | Capacity | Features | Suitability |
|---|---|---|---|
| Darin Drum Coater DR-C500 | 500 kg/batch | Stainless steel, PLC control | Small to medium plants |
| Darin Vacuum Coater DR-VC1000 | 1,000 kg/batch | Deep penetration, high accuracy | Premium & export markets |
| Custom Inline Coating System | Continuous | Integrated with conveyor | High-capacity, automated plants |
Vacuum coating is only used for aesthetics, not functionality.False
Vacuum coating ensures oils, vitamins, and palatants penetrate kibble pores, improving nutrition, palatability, and shelf stability beyond aesthetics.
5.7 Quality Control in Coating
| Test | Purpose | Standard |
|---|---|---|
| Fat Content | Ensures correct energy value | ±0.5% target |
| Vitamin Retention | Confirms micronutrient stability | ≥90% of label claim |
| Palatability Trials | Dogs’ acceptance test | ≥80% preference |
| Coating Uniformity | Visual and lab check | Even distribution |
Darin Machinery equips coaters with precision dosing pumps and real-time monitoring to guarantee consistency in every batch.
Once kibble has been dried and coated, it must be cooled and packaged properly to ensure long shelf life and preserve quality. Many manufacturers underestimate this final stage, but poor cooling or packaging can ruin all previous efforts. For example, warm kibble packed too soon can create condensation inside bags, leading to mold growth and product recalls. Packaging mistakes can also reduce palatability and cause customer complaints.
Cooling and packaging in dog kibble production involve reducing product temperature to ambient levels, stabilizing coated fats, and sealing kibble in moisture-proof, oxygen-controlled packaging (often with nitrogen flushing) to ensure shelf stability and market readiness.
Dog kibble can be packaged immediately after coating without cooling.False
Warm kibble causes condensation inside packaging, leading to mold growth and rancidity. Cooling to ambient temperature before packaging is essential.
Step 6: Cooling and Packaging
6.1 Cooling Process
After drying and coating, kibble typically exits at 40–60°C. Cooling is required to:
- Prevent condensation inside bags.
- Stabilize fats and palatants.
- Reduce microbial risk.
- Improve storage and transport safety.
Cooling Methods:
- Counterflow Cooler → Kibble flows downward while cool air moves upward. Ensures gradual, uniform cooling.
- Ambient Cooling Conveyor → Conveyor with fans blowing air. Used in smaller plants.
| Cooler Type | Capacity | Key Advantage |
|---|---|---|
| Counterflow Cooler | 1–10 T/h | High efficiency, uniform cooling |
| Ambient Conveyor Cooler | 0.5–3 T/h | Compact, low cost |
Target: Bring kibble temperature to within 5°C of ambient room temperature.
6.2 Packaging Options
Proper packaging is essential for shelf life and consumer satisfaction.
| Packaging Type | Description | Advantages | Shelf Life |
|---|---|---|---|
| Multi-layer Plastic Bags (PE/PP/PET) | Heat-sealed, 1–25 kg | Cost-effective, moisture barrier | 12–18 months |
| Laminated Pouches | Zipper or resealable | Premium feel, convenience | 12–18 months |
| Bulk Packaging (25–50 kg bags) | Large industrial sacks | For B2B distribution | 6–12 months |
| Cans or Tubs | Rigid containers | Niche, high-end brands | 18–24 months |
Key Functions of Packaging:
- Oxygen barrier (slows fat oxidation).
- Moisture barrier (prevents mold).
- Aroma retention (enhances consumer perception).
- Branding & labeling (regulatory compliance).
6.3 Nitrogen Flushing and Modified Atmosphere
To prevent oxidation of coated fats and oils, many manufacturers use nitrogen flushing:
- Air is displaced with nitrogen during sealing.
- Oxygen reduced to <2%.
- Extends shelf life by 3–6 months.
Premium brands often use Modified Atmosphere Packaging (MAP) with nitrogen + CO₂ for additional protection.
6.4 Packaging Line Automation
Modern kibble factories use fully automated bagging and palletizing systems:
- Weighing System → Ensures accurate filling (±0.2% tolerance).
- Form-Fill-Seal (FFS) Machines → Create, fill, and seal bags in one unit.
- Metal Detectors & Checkweighers → Final safety check.
- Robotic Palletizers → Stack bags for efficient logistics.
Darin Machinery’s packaging solutions integrate seamlessly with cooling lines and can handle small pouches to 50 kg bulk bags, depending on customer needs.
6.5 Labeling and Regulatory Compliance
Every packaged kibble must meet legal labeling requirements:
| Region | Mandatory Labeling |
|---|---|
| AAFCO (USA) | Guaranteed analysis (protein, fat, fiber, moisture), ingredient list, net weight, feeding instructions |
| FEDIAF (EU) | Analytical constituents, additives, lot number, best-before date |
| China/Asia | Similar to AAFCO, plus production license number |
Failure to comply can lead to import rejections or fines.
6.6 Process Flow of Cooling & Packaging
Coated Kibble (40–60°C) → Counterflow Cooler → Ambient Temperature Kibble → Weighing → Packaging (Nitrogen Flush) → Metal Detection → Sealed Bags → Palletizing → Distribution6.7 Common Issues and Solutions
| Problem | Cause | Solution |
|---|---|---|
| Moisture condensation in bags | Insufficient cooling | Extend cooling time, improve airflow |
| Rancid smell in products | Oxidation of fats | Add antioxidants, use nitrogen flushing |
| Broken bags during transport | Poor packaging material | Switch to laminated or reinforced bags |
| Inconsistent bag weights | Faulty weighing system | Calibrate and maintain equipment |
Paper bags without barrier layers are sufficient for dog kibble packaging.False
Dog kibble requires packaging with moisture and oxygen barriers, typically multi-layer plastic or laminated film. Plain paper bags allow spoilage and rancidity.
Even if kibble is produced with the best machinery and processes, the product cannot succeed without strict quality control (QC) and proper storage. This step ensures consistency, safety, and compliance with international regulations. A single quality failure can lead to costly recalls, brand damage, or export rejections.
Quality control and storage in dog kibble production involve continuous testing of raw materials and finished products, compliance with AAFCO/FEDIAF standards, HACCP protocols, and proper warehouse management to maintain freshness and prevent contamination.
Once kibble is packaged, there is no need for further quality testing.False
Finished kibble must undergo regular laboratory testing for nutrients, pathogens, and toxins to ensure safety, compliance, and consumer confidence.
Step 7: Quality Control and Storage
7.1 Laboratory Testing of Finished Kibble
Every batch of dog kibble must undergo nutritional and safety testing.
| Test | Method | Standard |
|---|---|---|
| Moisture | Oven drying | 8–10% |
| Crude Protein | Kjeldahl / NIR | As per recipe (e.g., 20–30%) |
| Crude Fat | Soxhlet extraction | Matches formulation |
| Fiber & Ash | Lab analysis | Consistency with claim |
| Aflatoxins | HPLC / ELISA | <20 ppb |
| Salmonella | Culture / PCR | Must be absent |
| Mycotoxins (DON, ZEA) | Chromatography | Within legal limits |
Tip from Darin Engineers: Install inline NIR analyzers for real-time protein and fat monitoring during production—reduces lab backlog and ensures batch consistency.
7.2 HACCP and Food Safety Protocols
Dog kibble factories must follow HACCP (Hazard Analysis and Critical Control Points):
- CCP 1: Raw Material Testing → Mycotoxins, pathogens.
- CCP 2: Extrusion → Critical kill step for pathogens.
- CCP 3: Drying → Ensures moisture stability.
- CCP 4: Packaging → Prevents recontamination.
Many Darin Machinery clients integrate metal detectors, sieves, and magnets to eliminate foreign objects at multiple stages.
7.3 Shelf-Life Studies
Manufacturers conduct accelerated shelf-life testing under controlled humidity and temperature. This ensures kibble maintains its nutritional label claims and palatability until the best-before date.
- Standard shelf life: 12–18 months for properly packaged dry kibble.
- Accelerated testing simulates 6–12 months storage in just weeks.
7.4 Storage and Warehouse Management
Even with perfect packaging, poor warehouse practices can destroy product quality.
Best Practices:
- Store at <25°C and <65% relative humidity.
- Use pallets to avoid contact with floors.
- Implement FIFO (First In, First Out) inventory rotation.
- Regular pest control and sanitation.
| Storage Issue | Cause | Prevention |
|---|---|---|
| Mold Growth | High humidity | Climate-controlled warehouse |
| Insect Infestation | Poor sealing, hygiene | Fumigation, airtight packaging |
| Bag Damage | Rough handling | Automated palletizing, reinforced bags |
Storing dog kibble in open containers is acceptable if the room is clean.False
Dog kibble must be stored in sealed, moisture-proof packaging to prevent contamination and nutrient loss.
7.5 Regulatory Compliance and Certification
To access global markets, manufacturers must comply with local and international regulations:
- AAFCO (USA): Ingredient definitions, guaranteed analysis.
- FEDIAF (EU): Nutritional guidelines, additives, labeling.
- China Feed Law: Production license, safety testing.
- ISO 22000 / HACCP Certification: International food safety standards.
- BRC / IFS Certification: Often required by European retailers.
Darin Machinery assists clients in aligning equipment and processes with these compliance frameworks.

By now, we’ve covered each technical stage in detail: from ingredient selection to quality control. In this section, we will consolidate all steps into a clear production roadmap, add cost-capacity insights, and provide real-world case studies from Darin Machinery installations.
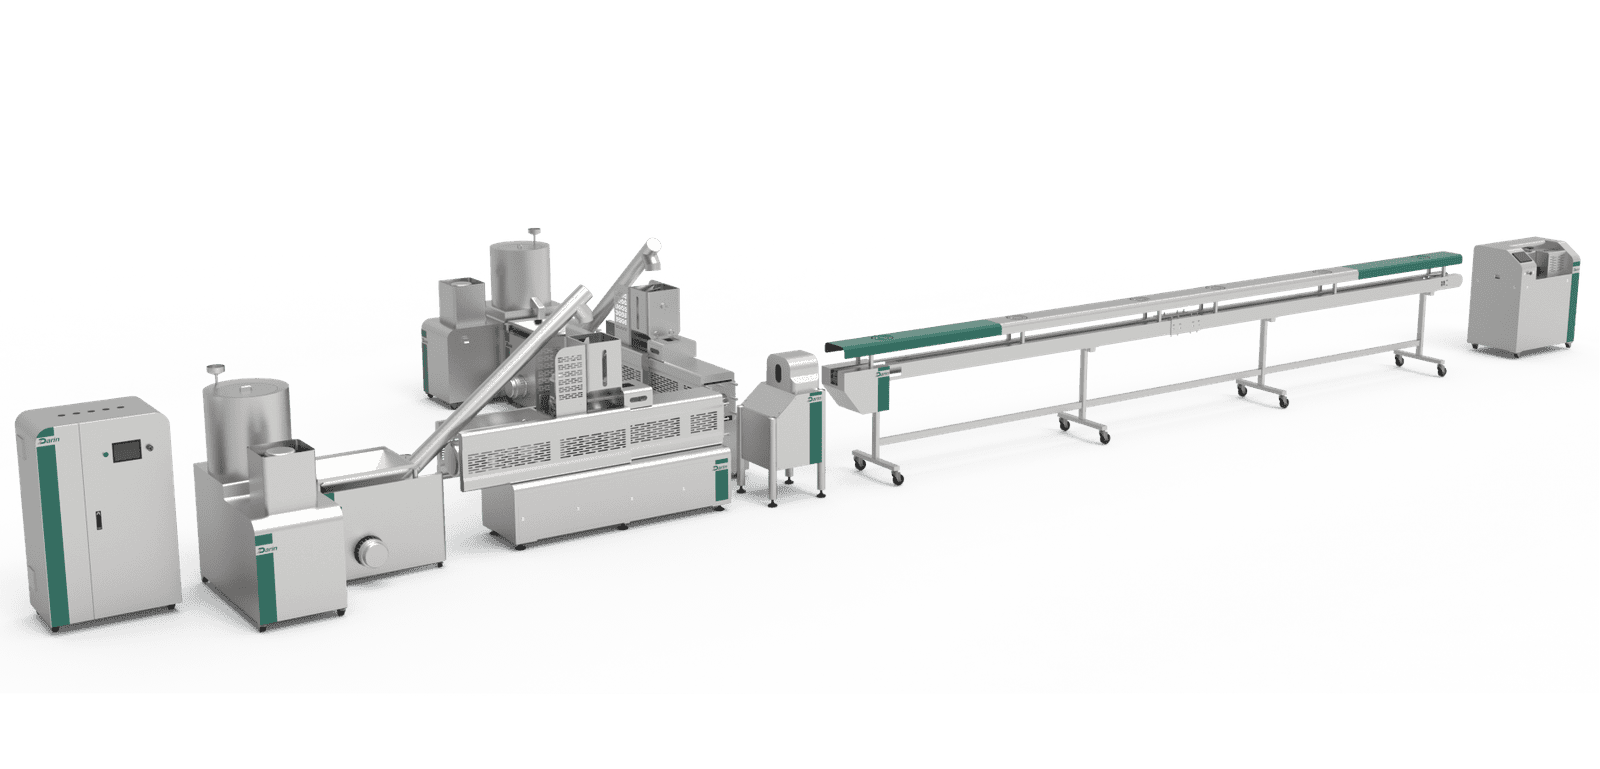
The full dog kibble production process includes ingredient preparation, grinding, mixing, extrusion, drying, coating, cooling, packaging, and storage, forming a continuous automated system that ensures consistent, safe, and high-quality products.
Dog kibble production lines are identical across all manufacturers.False
While the process flow is similar, equipment design, automation level, capacity, and quality control systems vary significantly between manufacturers.
8.1 Complete Dog Kibble Production Flow
Raw Materials → Grinding (Hammer Mill) → Mixing (Ribbon/Paddle Mixer) → Pre-conditioning (Optional) →
Extrusion (Twin-Screw Extruder) → Cutting & Shaping → Drying (Multi-Layer Belt Dryer) →
Spraying & Coating (Vacuum/Drum Coater) → Cooling (Counterflow Cooler) →
Packaging (Nitrogen Flush) → Quality Control → Storage & Distribution
8.2 Process Overview Table
| Step | Equipment | Key Parameter | Output |
|---|---|---|---|
| Ingredient Prep | Storage Silos | Moisture <12% | Safe raw stock |
| Grinding | Hammer Mill | 0.2–0.6 mm | Uniform powder |
| Mixing | Ribbon Mixer | CV ≤ 5% | Homogeneous blend |
| Extrusion | Twin-Screw Extruder | 90–160°C, 20–40 bar | Cooked, shaped kibble |
| Drying | Multi-layer Dryer | Final 8–10% moisture | Shelf-stable product |
| Coating | Vacuum Coater | Oil 3–10%, vitamins | Palatable kibble |
| Cooling | Counterflow Cooler | Ambient ±5°C | Stable, safe kibble |
| Packaging | Form-Fill-Seal | Nitrogen flushing | Sealed bags |
| QC & Storage | Lab + Warehouse | HACCP standards | Market-ready kibble |
8.3 Capacity–Cost Analysis
Investors often ask: What does it cost to set up a dog kibble factory?
Here’s an industry-average analysis:
| Production Line Capacity | Typical Extruder Model | Estimated Investment (USD) | Daily Output (8h) | Target Market |
|---|---|---|---|---|
| 150–250 kg/h | DR-65 Twin-Screw | \$80,000 – \$120,000 | 1.2–2 tons | Startups, pilot plants |
| 300–500 kg/h | DR-70 Twin-Screw | \$120,000 – \$180,000 | 2.4–4 tons | Small-medium factories |
| 800–1200 kg/h | DR-85 Twin-Screw | \$200,000 – \$300,000 | 6.5–10 tons | Regional brands |
| 1500–2000 kg/h | DR-95 Twin-Screw | \$350,000 – \$500,000 | 12–16 tons | Large-scale export plants |
| 3000–5000 kg/h | Custom Line | \$600,000 – \$1,000,000+ | 24–40 tons | Global brand suppliers |
Note: Costs include extruder, dryer, coater, cooler, packaging system, and auxiliary equipment. Land, utilities, and raw materials not included.
8.4 Case Studies from Darin Machinery Clients
Case 1: Italy – Premium Pet Food Startup
- Line Capacity: 300 kg/h (DR-70 Twin-Screw)
- Focus: Grain-free kibble with salmon and potato.
- Result: Production scaled to 2.5 tons/day, achieving premium exports to Germany.
Case 2: Germany – Established Pet Brand
- Line Capacity: 1200 kg/h (DR-85 Twin-Screw + Vacuum Coater)
- Focus: Functional kibble with glucosamine for joint health.
- Result: Expanded shelf presence in 8 EU countries, extended shelf life by 4 months.
Case 3: Brazil – Mid-Sized Factory Expansion
- Line Capacity: 2000 kg/h (DR-95 Twin-Screw + Multi-layer Dryer)
- Focus: Affordable kibble for domestic market.
- Result: Lowered production cost/ton by 18% compared to imported machinery.
Case 4: China – Large Export-Oriented Plant
- Line Capacity: 5000 kg/h (Custom Line with robotics)
- Focus: High-volume, multi-formula production.
- Result: Supplies kibble to Southeast Asia and Middle East with fully automated QC.
8.5 ROI Consideration
Dog kibble is a high-demand, recurring market. On average:
- Raw material cost share: 60–70% of production cost.
- Energy + labor: 15–20%.
- Packaging + logistics: 10–15%.
- Net profit margin: 8–15% (higher for premium brands).
Payback Period:
- Small plants: 1.5–2 years.
- Large plants: 2–3 years.

Over the past eight sections, we’ve walked step by step through the entire dog kibble manufacturing process — from ingredient selection all the way to packaging and storage. What began as raw proteins, grains, and oils has been systematically transformed into a safe, nutritious, and highly palatable pet food product.
Making dog kibble requires ingredient preparation, grinding, mixing, extrusion cooking, drying, coating, cooling, packaging, and strict quality control, supported by advanced machinery and HACCP compliance to ensure global export standards.
Dog kibble manufacturing is too complex for new businesses to enter.False
With the right machinery, supplier support, and training, even new entrants can establish successful kibble factories. Darin Machinery provides turnkey solutions to reduce technical barriers.
9.1 Key Takeaways from the Guide
- Step 1: Ingredient Selection → Nutritional quality begins with proteins, starches, fats, fibers, vitamins, and minerals.
- Step 2: Grinding & Mixing → Uniform particle size and consistent blending ensure extrusion success.
- Step 3: Extrusion Cooking → The “heart” of kibble production, shaping and sterilizing the product.
- Step 4: Drying → Reduces moisture to 8–10% for safety and shelf stability.
- Step 5: Coating → Adds fats, oils, vitamins, and palatants to boost palatability and nutrition.
- Step 6: Cooling & Packaging → Stabilizes product temperature and locks in freshness with protective bags.
- Step 7: Quality Control & Storage → Laboratory testing, HACCP, and safe warehousing safeguard brand reputation.
- Step 8: Investment & ROI → Scalable capacities from 150 kg/h to 5 T/h, with 1.5–3 year payback periods.
9.2 Why Darin Machinery?
As this guide shows, producing dog kibble is both a science and an engineering challenge. Many companies fail not because of lack of demand, but because of poor process control or unreliable equipment.
Darin Machinery Advantages:
- Full Production Lines: From grinding to packaging, fully integrated systems.
- Global Certification: CE, ISO, HACCP-ready.
- Scalable Capacity: From 150 kg/h for startups to 5,000 kg/h for global exporters.
- Turnkey Support: Recipe development, installation, training, after-sales service.
- Proven Track Record: Clients in Europe, Asia, South America, and the Middle East.
9.3 Final Thought
The pet food market continues to grow rapidly worldwide, driven by the humanization of pets and rising demand for premium, functional foods. Entering this industry with the right partner and technology can position your business for long-term success.
✅ If you’ve made it this far, you now understand every step of how dog kibble is made. The next step is yours — and we at Darin Machinery are ready to walk it with you.
📩 Ready to Build Your Dog Kibble Business?
Contact Darin Machinery today for:
- Free consultation on plant design and capacity planning.
- Customized recipes for different markets (grain-free, functional, premium).
- Complete turnkey solutions for dog kibble production.
📧 Email us at: darin4@darin.cn
🌍 Visit us: petreatsmachine.com
Let’s create high-quality dog kibble together — from raw materials to finished bags on store shelves.