Pet owners today demand far more from cat food than ever before. Cats are obligate carnivores—requiring protein-dense, highly digestible food—and wet cat food fulfills that biological need better than dry kibble. Yet manufacturing it safely, nutritiously, and profitably is no easy task. Without precise temperature control, hygiene design, and sterilization, products can spoil or lose nutritional value. The consequences? Brand recalls, loss of consumer trust, and even risks to animal health.
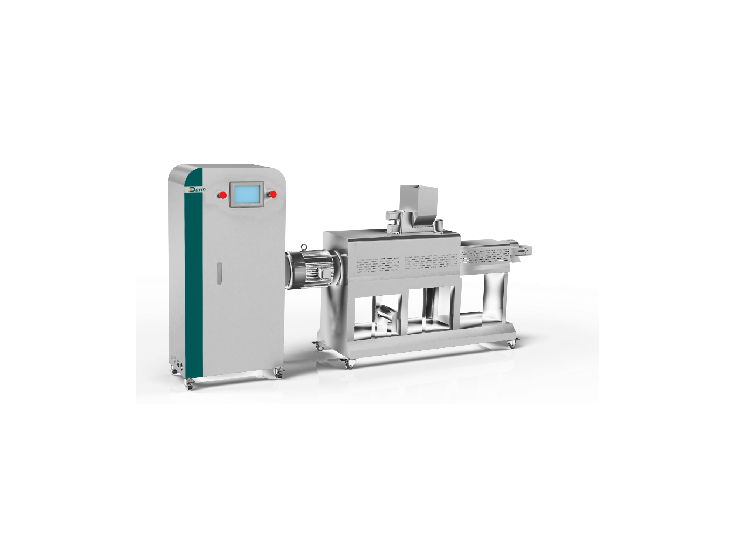
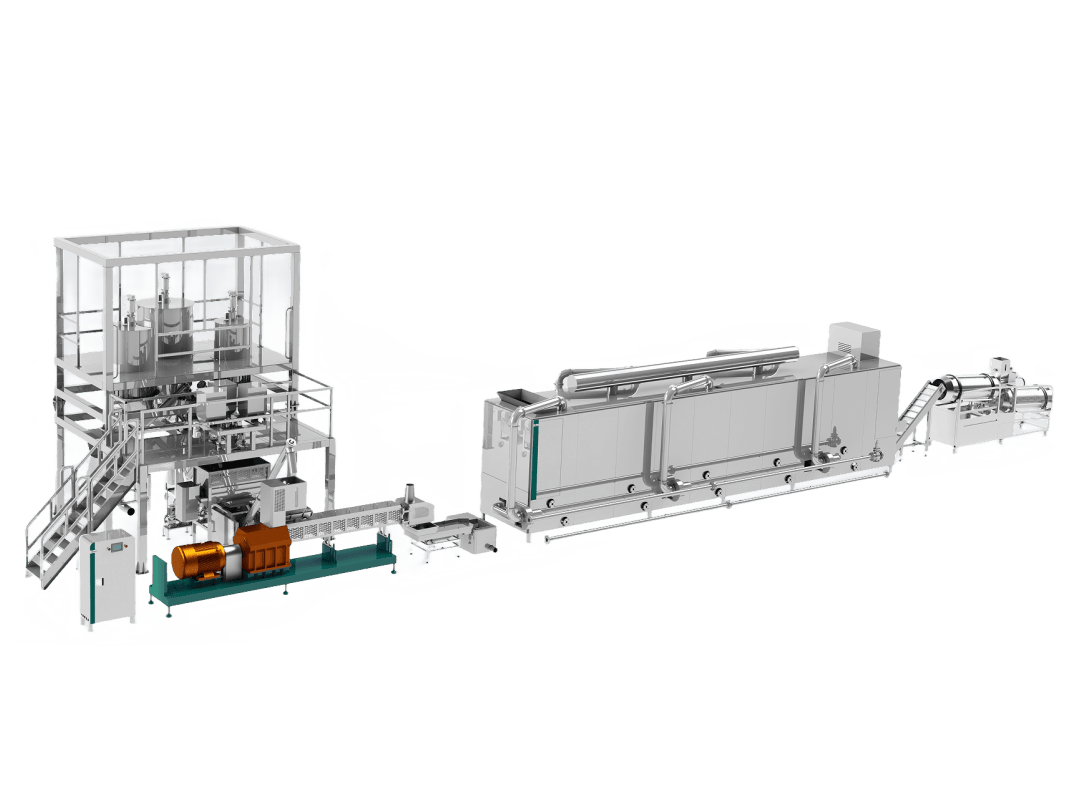
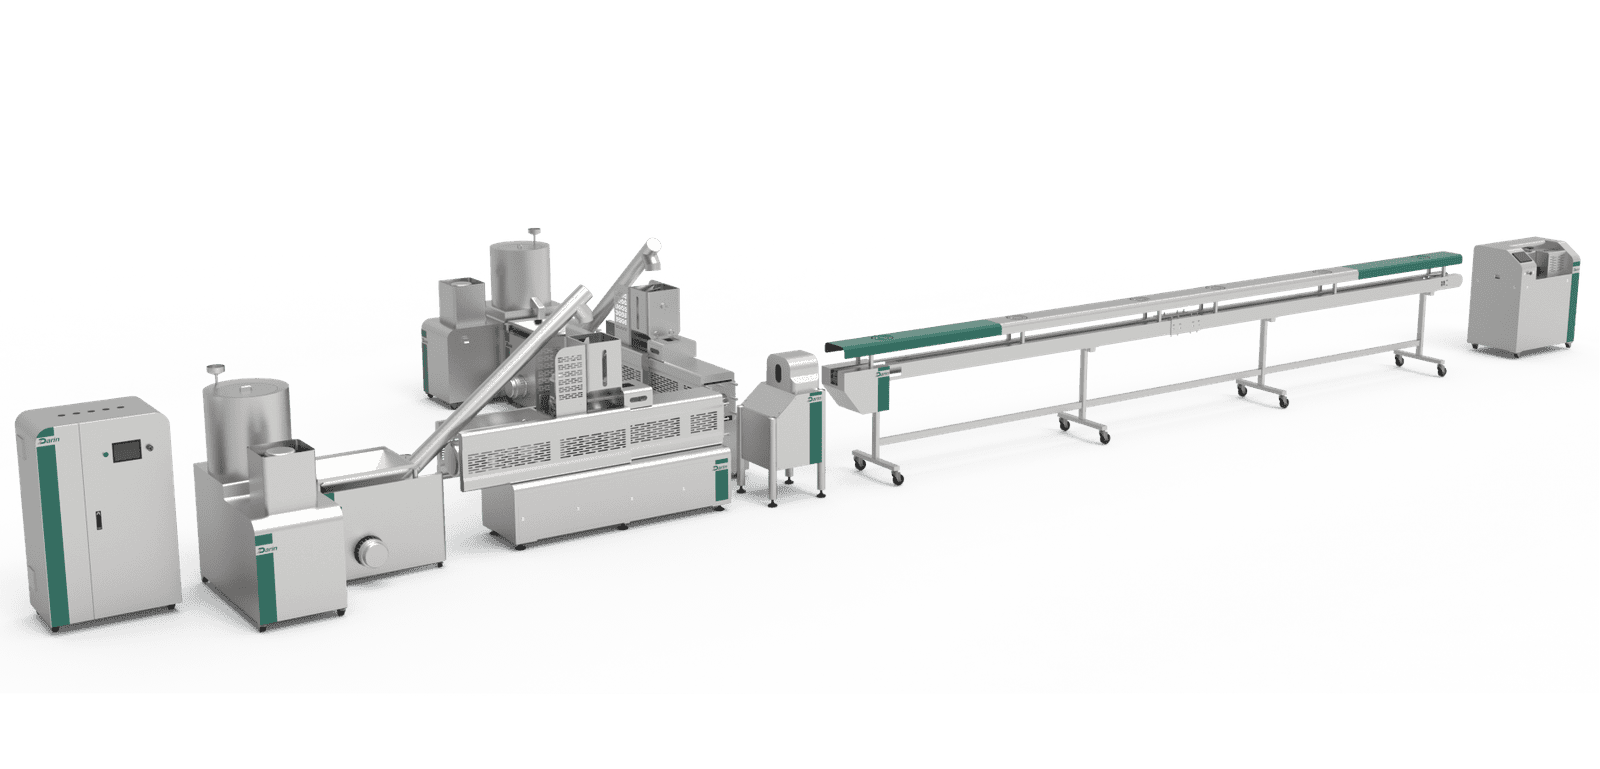
The solution is industrial precision. Modern automated wet cat food production lines, like those engineered by Darin Machinery, integrate grinding, mixing, filling, sealing, sterilization, and cooling into a seamless, hygienic process. Each parameter—temperature, pressure, mixing ratio, viscosity—is controlled to preserve nutrients while guaranteeing sterility and consistent texture.
Wet cat food is produced through a carefully controlled multi-stage industrial process that transforms raw animal and plant ingredients into safe, shelf-stable, and nutritionally complete products. It involves ingredient preparation, grinding, blending, pre-cooking, filling, sealing, retort sterilization, cooling, and packaging. Both pâté and chunk-in-gravy styles use similar core technologies but differ in texture formation, water phase, and filling sequence.
Manufacturers and entrepreneurs entering this market quickly realize that wet cat food production is equal parts food science and mechanical engineering. Every step—from raw meat intake to the precise sealing of cans—affects flavor, shelf life, and production efficiency. In this guide, we’ll take a deep dive into each stage, explaining both pâté and chunk-in-gravy production, industry benchmarks, and the equipment technologies behind successful operations.
Wet cat food can be made without sterilization as long as it is refrigerated.False
Commercial wet cat food must undergo retort sterilization to destroy microorganisms and spores. Refrigeration alone cannot ensure safety or shelf stability.
Both pâté and chunk-in-gravy styles of wet cat food share the same basic processing stages.True
They differ mainly in texture and formulation, but the overall manufacturing framework—grinding, mixing, filling, sealing, and sterilization—remains consistent.
Step 1: Ingredient Sourcing and Quality Control
Wet cat food begins with the selection of raw ingredients that meet strict nutritional and hygienic criteria. Typical recipes include:
| Category | Common Ingredients | Functional Purpose |
|---|---|---|
| Animal Proteins | Chicken, beef, salmon, tuna, turkey, liver, animal by-products | Protein, flavor, amino acids (taurine source) |
| Carbohydrates | Rice, wheat, potato starch, pea flour | Binding agent, energy source |
| Fats and Oils | Poultry fat, fish oil, sunflower oil | Palatability, essential fatty acids |
| Gums and Hydrocolloids | Guar gum, carrageenan, locust bean gum | Texture, viscosity, water retention |
| Micronutrients | Vitamin A, D3, E, B complex, zinc, calcium | Nutritional balance |
| Water or Broth | Fresh water or meat stock | Hydration, palatability |
Raw materials are delivered frozen or chilled and stored under HACCP-controlled conditions. Meat blocks are kept below –18°C to maintain freshness, while dry ingredients like starch or vitamin premixes are stored in humidity-controlled silos.
Every batch undergoes microbiological testing for E. coli, Salmonella, and Listeria, plus sensory inspection for odor and texture. Only materials that meet internal and regulatory standards proceed to processing.
Darin Machinery’s line designs incorporate raw material reception silos and temperature-monitored conveyors, ensuring hygiene compliance per ISO 22000 and FDA CFR Title 21.
Step 2: Grinding and Particle Size Reduction
The next critical step is converting whole or frozen meat blocks into a uniform, processable form. This is achieved using industrial meat grinders equipped with variable screens (3–8 mm).
For pâté-style production, finer particle sizes (around 3 mm) yield smooth emulsions.
For chunk-in-gravy, coarser cuts (up to 12 mm) are used to preserve visible meat texture.
| Grinding Specification | Pâté | Chunk-in-Gravy |
|---|---|---|
| Screen hole diameter | 3–4 mm | 8–12 mm |
| Meat temperature during grinding | ≤ 12°C | ≤ 15°C |
| Oxygen exposure | Minimal | Controlled |
Modern grinders are built from SUS304 or SUS316 stainless steel and feature dual-shaft feeding screws that prevent clogging and maintain steady throughput.
Darin’s DRG-Series grinders, for example, include an auto-feed and discharge system synchronized with the downstream mixing unit, minimizing manual handling and oxidation.
A magnetic separator and metal detector ensure no metallic fragments contaminate the product—an essential safety feature required under HACCP and FEDIAF guidelines.
Step 3: Mixing, Emulsification, and Pre-Heating
Once ground, the meat and secondary ingredients are transferred to large vacuum mixers or emulsifiers, which combine proteins, fats, starches, and water into a stable matrix.
In pâté production, this process creates the creamy texture consumers expect. In chunk-in-gravy, the slurry serves as the “gravy phase,” while separate meat cubes form the “solid phase.”
Key stages of mixing include:
- Pre-mix: All main ingredients (meat, fat, water) are loaded.
- Dry blending: Carbohydrates, binders, and hydrocolloids are added.
- Vacuum deaeration: Removes entrapped air for better density and shelf life.
- Nutrient addition: Vitamins and minerals added last to avoid heat loss.
- Thermal conditioning: Optional heating to 45–60°C for pre-gelatinization.
| Mixing Variable | Control Target |
|---|---|
| Temperature | 45–60°C |
| Mixing Time | 8–15 minutes |
| Vacuum Pressure | –0.08 MPa |
| Viscosity | 2,000–5,000 cP |
| pH | 6.0–6.5 |
High-shear mixing ensures uniform viscosity and eliminates phase separation during sterilization. The final blend is tested for pH, viscosity, and microbiological integrity.
Darin’s DRV Vacuum Mixer includes a CIP system for self-cleaning, preventing cross-contamination between recipes. Optional heating jackets accelerate gelatinization when starch or plant proteins are used as binders.
Step 4: Cooking, Chunk Formation, and Product Differentiation
Here, the process diverges between pâté and chunk-in-gravy styles:
Pâté Production:
- The blended emulsion is transferred directly to a steam-jacketed cooker or twin-screw thermal extruder.
- Thermal treatment (typically 85–95°C) denatures proteins, stabilizes texture, and activates gelling agents.
- The heated mass is pumped directly into the filling machine for can or tray filling.
Chunk-in-Gravy Production:
- The mixture is extruded or molded into meat “chunks” using a former or co-extruder.
- These chunks are pre-cooked via steam tunnel or water blancher to reach internal temperatures of 80–90°C.
- After cooling, the chunks are mixed with a separate gravy phase prepared from the same base slurry.
| Process Parameter | Pâté | Chunk-in-Gravy |
|---|---|---|
| Cook Temperature | 85–95°C | 80–90°C |
| Cook Time | 5–10 min | 3–5 min |
| Product Texture | Smooth | Structured |
| Water Activity (aw) | 0.95–0.97 | 0.96–0.98 |
Forming Equipment Examples (Darin Machinery):
- DRC-300 Co-Extruder: For forming meat chunks at high throughput.
- DRT-200 Steam Tunnel: For continuous pre-cooking of chunks.
- DRM-500 Mixer-Blender: For recombining chunks with gravy in precise ratios (typically 60:40).
The outcome is the distinct visual and textural difference that defines each product category. Both must retain flavor compounds without excessive fat separation or syneresis.
Step 5: Filling and Portioning — Precision Dosing for Product Consistency
After cooking or chunk formation, the semi-liquid mixture (for pâté) or the combination of meat chunks and gravy (for chunk-in-gravy) is conveyed to automatic filling systems. The goal at this stage is precision and hygiene: every can, tray, or pouch must receive the exact programmed amount of product without air entrapment or contamination.
The filling stage is one of the most sensitive steps in wet cat food production because even slight errors in weight or seal integrity can compromise sterilization and shelf stability.
Filling Systems by Product Type
| Product Type | Filling Equipment | Filling Method | Accuracy |
|---|---|---|---|
| Pâté | Piston filler with servo control | Continuous volumetric dosing | ±1 g |
| Chunk-in-Gravy | Dual-phase filling system (chunks + gravy) | Sequential or co-filling | ±2 g |
| Pouch | Rotary pouch filler | Pre-made pouch automatic filling | ±2 g |
Filling machines must be made of SUS316 stainless steel, with CIP (Clean-In-Place) capability and hygienic design (EHEDG standard).
Darin Machinery’s DRF-Series Automatic Filling Line is widely used in mid- and large-scale pet food factories.
- It can handle cans, aluminum trays, or retort pouches.
- Servo motors control dosing pistons for repeatable accuracy.
- The line integrates with nitrogen-flushing systems to reduce oxygen and extend product shelf life.
- Optional dual-hopper design allows alternating between pâté and gravy formulations without downtime.
Control Parameters:
- Fill temperature: 75–85°C (prevents microbial risk)
- Air content: <2%
- Weight deviation: ≤1.5 g/can
- Capacity: 150–300 cans/min (depending on size)
Step 6: Sealing — Creating the Hermetic Barrier
Once filled, containers are immediately sealed to protect against contamination before sterilization. The sealing process differs based on packaging material:
| Container Type | Sealing Technology | Equipment Example | Critical Control |
|---|---|---|---|
| Metal Cans | Double seam sealing | DRZ-100 Can Seamer | Seam integrity, vacuum level |
| Aluminum Trays | Heat sealing with film | DRT-300 Tray Sealer | Film temperature, sealing pressure |
| Retort Pouches | Rotary pouch sealing | DRP-200 Pouch Sealer | Seal width, leakage detection |
Can Sealing Process (For Pâté and Chunk-in-Gravy)
- The can lid is automatically positioned.
- Vacuum or steam flushing removes oxygen.
- The seaming roller folds the lid and flange to create a hermetic double seam.
- Online leak detectors and X-ray scanners check seal integrity.
Darin’s DRZ-100 Seamer uses a dual-station high-speed design synchronized with the filling line and includes inline vision inspection to detect any seam defects.
Key Parameters:
- Vacuum inside can: 50–100 mbar
- Sealing pressure: 0.4–0.6 MPa
- Seam overlap: 50–75%
- Seam thickness: 1.1–1.3 mm
Proper sealing ensures a sterile environment before the retort sterilization process. Any air trapped inside may expand during heating, deforming containers or breaking seals—leading to contamination or product loss.
Step 7: Retort Sterilization — The Heart of Shelf-Stable Wet Cat Food
This is the most critical step for food safety and shelf stability. Retort sterilization uses high-pressure steam to heat the sealed containers to temperatures above 115–121°C (240–250°F). This process eliminates all pathogenic bacteria and spores, ensuring that the product remains safe and stable for up to 36 months at ambient temperature.
Working Principle
Cans or pouches are loaded into retort baskets and transferred into autoclaves (retorts). Once sealed, the system injects saturated steam or a mixture of steam and air, maintaining constant pressure and temperature for a programmed time.
Darin Machinery’s DRR-Series Retort Sterilizers are designed for pet food, featuring PLC-controlled sterilization curves and automatic cooling systems. The PLC system records temperature and pressure data for each batch, satisfying traceability requirements under ISO 22000 and FDA 21 CFR Part 11.
Typical Retort Parameters
| Product | Temperature (°C) | Holding Time (min) | Pressure (bar) | F₀ Value |
|---|---|---|---|---|
| Pâté (200g can) | 121 | 60 | 1.8 | 8–12 |
| Chunk-in-Gravy (400g can) | 118 | 75 | 1.8 | 10–15 |
| Pouch (85g) | 116 | 45 | 1.6 | 7–9 |
F₀ value refers to the sterilization effectiveness at 121°C. For wet pet food, F₀ values typically range between 8 and 15, depending on container type and product density.
Types of Retort Systems
| Retort Type | Description | Typical Use |
|---|---|---|
| Steam Retort | Uses saturated steam; efficient for metal cans | Pâté, high-viscosity products |
| Water Spray Retort | Uses water jets for uniform heat distribution | Retort pouches, trays |
| Rotary Retort | Continuously rotates containers during sterilization | Chunk-in-gravy for improved heat penetration |
| Cascading Water Retort | Energy-efficient with water recirculation | Premium or eco lines |
During sterilization, the core temperature of the product must reach the lethal level long enough to destroy Clostridium botulinum spores. The challenge lies in heating the product thoroughly without degrading texture, color, or nutrient content.
Darin’s DRR-800 Retort Autoclave includes:
- Dual thermocouple monitoring for validation.
- Steam-air mixing to ensure even heat distribution.
- Automatic pressure compensation to prevent can deformation.
- Energy-saving condensate recovery system reducing steam consumption by 25%.
Step 8: Cooling, Drying, and Post-Processing
After sterilization, products are rapidly cooled to below 35°C to prevent overcooking and ensure safe handling. Cooling is typically performed with filtered water sprays or water immersion in the same retort chamber.
Critical Control Points:
- Cooling water must be chlorinated (0.5–1 ppm) or UV-treated.
- Temperature difference between product and cooling water ≤ 15°C (to avoid container deformation).
- Cooling rate: from 121°C → 35°C within 30 minutes.
After cooling, products are dried with air blowers or conveyor dryers. This prevents rusting of metal cans and ensures proper label adhesion later. Containers then move to the post-process inspection area, where they undergo:
- Visual inspection for dents, bulging, or discoloration.
- Leak testing under vacuum.
- Weight verification via checkweighers.
- Coding and labeling preparation.
| Parameter | Standard Target |
|---|---|
| Final product temperature | <35°C |
| Surface moisture | <1% |
| Deformation allowance | 0% |
| Cooling water microbiology | <100 CFU/mL |
This cooling phase may appear simple, but it is vital: improper cooling can trigger post-process contamination or nutrient oxidation.
Equipment Overview – Core Wet Cat Food Line (Darin Machinery)
| Equipment Name | Function | Example Model | Capacity | Key Features |
|---|---|---|---|---|
| Meat Grinder | Particle size reduction | DRG-300 | 500–1000 kg/h | Dual-screw feed, low-temp grinding |
| Vacuum Mixer | Uniform blending | DRV-500 | 800–1200 kg/h | CIP system, jacketed heating |
| Co-Extruder | Chunk formation | DRC-300 | 300–800 kg/h | Adjustable die, texture control |
| Automatic Filler | Portioning into containers | DRF-200 | 200–300 cans/min | Servo control, nitrogen flush |
| Can Sealer | Hermetic closure | DRZ-100 | 200–400 cans/min | Leak detector, auto reject |
| Retort Sterilizer | Thermal sterilization | DRR-800 | 2–6 baskets/batch | PLC curve control, F₀ validation |
| Cooling Conveyor | Post-retort cooling | DRC-600 | Continuous | Filtered spray cooling |
| Labeling & Coding Line | Branding & traceability | DRL-400 | 100–300 units/min | Inkjet/laser coder |
Darin’s systems can be configured for pâté, chunk-in-gravy, or mixed-format production. Fully automatic CIP (Cleaning-In-Place) options enable daily sanitation with minimal labor.
Energy & Water Efficiency Data
| Process Step | Energy Source | Energy Use (kWh/kg) | Water Use (L/kg) |
|---|---|---|---|
| Grinding & Mixing | Electricity | 0.15 | 0.5 |
| Cooking/Extrusion | Steam | 0.35 | 0.3 |
| Retort Sterilization | Steam + Condensate | 0.80 | 1.2 |
| Cooling & Cleaning | Electricity + Water | 0.25 | 2.5 |
| Packaging & Handling | Electricity | 0.10 | 0.1 |
| Total (Average) | — | 1.65 | 4.6 |
Darin’s next-generation retorts and heat exchangers integrate energy recovery systems, which reduce overall steam consumption by up to 30% through condensate recycling. This is a major advantage for factories pursuing ISO 50001 energy management certification or sustainability branding.
Step 9: Quality Control and Laboratory Verification
Wet cat food manufacturing is regulated under stringent global standards such as EU Regulation (EC) No 767/2009, FDA CFR Title 21 Part 507, and FEDIAF (European Pet Food Industry Federation) guidelines. Ensuring that every can or pouch is nutritionally balanced, microbiologically safe, and physically intact is non-negotiable.
Key Quality Control Stages
| QC Stage | Purpose | Analytical Method | Frequency |
|---|---|---|---|
| Raw Material Testing | Verify freshness, composition | Moisture, fat, protein, pH | Every batch |
| In-Process Testing | Monitor uniformity and safety | Temperature, viscosity, pH | Every 30–60 min |
| Post-Retort Sterility | Ensure commercial sterility | Incubation test (35°C/10d) | Every batch |
| Finished Product Testing | Nutrient content verification | Proximate analysis (AOAC) | Weekly |
| Packaging Integrity | Detect leaks or deformation | Vacuum, compression, dye tests | 100% online check |
Analytical Parameters and Target Values
| Parameter | Pâté Style | Chunk-in-Gravy | Tolerance |
|---|---|---|---|
| Moisture (%) | 75–80 | 78–82 | ±1.0 |
| Crude Protein (%) | 9–12 | 8–10 | ±0.5 |
| Crude Fat (%) | 3–6 | 3–5 | ±0.5 |
| Ash (%) | 1.5–2.5 | 1.5–2.5 | ±0.3 |
| pH | 6.0–6.5 | 6.0–6.5 | ±0.1 |
| Water Activity (aw) | 0.96–0.98 | 0.96–0.98 | ±0.01 |
These parameters determine the product’s safety, texture, and flavor.
- Protein affects gel strength and texture.
- Moisture influences mouthfeel and shelf life.
- Fat content contributes to aroma and caloric density.
- pH and aw ensure microbial stability.
Laboratories in pet food factories are equipped with viscometers, spectrophotometers, Kjeldahl analyzers, and texture analyzers. Some advanced plants use inline near-infrared (NIR) sensors for real-time composition monitoring.
Microbiological Testing
| Microorganism | Acceptable Limit | Method |
|---|---|---|
| Total Plate Count | <10³ CFU/g | Plate count agar |
| E. coli | Absent in 1 g | ISO 16649-2 |
| Salmonella spp. | Absent in 25 g | ISO 6579 |
| Clostridium botulinum | Absent | PCR-based assay |
| Yeast & Mold | <100 CFU/g | YGC agar |
Failure in microbiological testing can result in product quarantine, re-sterilization, or destruction. Automated retort data recording systems, like Darin DRR-800’s PLC archive, allow full traceability from ingredient to finished can.
Step 10: Storage, Labeling, and Distribution
Once products pass all QC checks, they are ready for labeling and logistics. Labeling systems apply paper labels, shrink sleeves, or direct printing, depending on packaging type and market requirements.
Labeling Data Required by Regulation
- Product name and composition list
- Guaranteed analysis (protein, fat, fiber, moisture)
- Feeding guidelines
- Manufacturer name, address, contact
- Lot number and best-before date
- Net weight
Labeling precision is vital, especially for export to the EU, USA, or Japan, where pet food labeling is audited regularly.
After labeling, cans and pouches are cartoned, palletized, and wrapped.
- Storage temperature: 15–25°C
- Humidity: <65%
- Stacking height: <6 layers to avoid deformation
- Shelf life: typically 24–36 months
Darin Machinery’s DRL-400 automatic labeling system integrates barcode scanners and printers for batch traceability, linked directly with MES (Manufacturing Execution System) platforms for digital tracking.
Step 11: Palatability and Sensory Evaluation
Even the most nutrient-balanced cat food can fail if cats refuse to eat it. That’s why palatability testing and sensory analysis are core components of R&D.
Cat Palatability Trials
Specialized facilities maintain test panels of 20–50 cats that are offered two or more formulations under controlled conditions. Measurements include:
- First choice rate (which product cats approach first)
- Intake ratio (how much they eat)
- Total consumption time
A typical high-quality formula achieves >70% preference compared to the control sample.
Sensory and Texture Analysis
Human sensory panels (trained analysts) evaluate:
- Aroma intensity and pleasantness
- Appearance and color uniformity
- Consistency and structure
- Gel strength (for pâté)
- Gravy viscosity and chunk integrity (for chunk-in-gravy)
| Attribute | Measurement Tool | Optimal Range |
|---|---|---|
| Texture firmness | Texture Analyzer | 200–400 g/cm² |
| Gravy viscosity | Brookfield viscometer | 2,000–4,000 cP |
| Color L* value | Colorimeter | 50–70 |
| Aroma intensity | GC-MS volatile analysis | >80% retention post-retort |
Palatability improvements are often achieved by using liver hydrolysates, yeast extracts, or fish proteins as natural attractants. These enhance flavor and aroma without artificial additives.
Step 12: Sustainability, Energy Efficiency, and Innovation
The global wet pet food industry is moving rapidly toward sustainable manufacturing, with consumers and governments pushing for carbon-neutral operations, eco-packaging, and minimal waste.
Key Sustainability Focus Areas
| Area | Practice | Benefit |
|---|---|---|
| Energy Efficiency | Heat recovery from retorts, variable steam control | 25–30% less steam use |
| Water Recycling | Condensate recovery and CIP reuse | Up to 40% less water consumption |
| Waste Management | Meat trimmings converted to rendering | Reduces landfill waste |
| Packaging Innovation | Recyclable mono-material pouches, aluminum trays | Improved recyclability |
| Renewable Power | Solar and biogas integration | CO₂ reduction |
| Digital Monitoring | PLC + IoT predictive maintenance | Lower downtime, optimized energy |
Darin Machinery has integrated these principles into its next-generation production lines, which feature:
- Energy recovery boilers and condensate collection loops.
- PLC-controlled steam optimization in DRR retorts.
- Smart CIP systems reducing detergent use by 30%.
- Eco-friendly modular conveyors made from recyclable materials.
These advancements not only lower operational costs but also strengthen the environmental credentials of brands entering export markets, where sustainability is now a competitive advantage.
Comparison of Pâté vs Chunk-in-Gravy Wet Cat Food Production
| Aspect | Pâté | Chunk-in-Gravy |
|---|---|---|
| Texture | Smooth and uniform | Meat pieces in sauce |
| Meat Preparation | Finely ground, emulsified | Coarsely ground, formed chunks |
| Cooking | In-line thermal cooking or pre-pasteurization | Pre-cooking of chunks + separate gravy |
| Filling | Direct piston filling | Dual-phase sequential filling |
| Retort Parameters | 121°C, 60 min | 118°C, 75 min |
| Appearance | Homogeneous | Visually heterogeneous |
| Consumer Preference | Older cats, soft texture | Younger/adult cats, meat texture |
| Equipment Requirement | Mixer + Filler + Retort | Grinder + Former + Dual Filler + Retort |
Both styles demand precision in sterilization and formulation, but chunk-in-gravy requires more complex handling systems and synchronization between solid and liquid phases.
Global Trends in Wet Cat Food Manufacturing
- Premiumization: Human-grade ingredients, traceable sourcing, and low-ash meats are increasingly demanded.
- Grain-Free & High-Protein: Formulations exclude corn or wheat and emphasize fresh meat content.
- Functional Nutrition: Added probiotics, omega-3s, and joint support ingredients.
- Single-Serve Pouches: Rising in popularity for portion control and freshness.
- Automation: From raw intake to palletizing, reducing labor dependence.
- Smart Factories: Integration of IoT and SCADA for real-time monitoring and energy optimization.
Darin Machinery supports these trends with customized modular lines, adaptable to new formulations and packaging types, meeting both economic and ecological goals.
Summary: The Science and Engineering Behind Every Can
Producing wet cat food is both an art of nutrition and a science of process engineering. Each step—from grinding raw meat to sealing sterilized cans—requires precision, hygiene, and technical control.
- Ingredient preparation determines nutritional value and safety.
- Grinding and mixing affect texture and uniformity.
- Cooking and chunk formation shape the final mouthfeel.
- Filling and sealing ensure dosing accuracy and airtightness.
- Retort sterilization guarantees microbial safety and shelf life.
- Cooling, labeling, and QC maintain product consistency and regulatory compliance.
When executed correctly, the result is a nutritionally complete, shelf-stable, and palatable product loved by cats and trusted by pet owners.
Darin Machinery’s end-to-end lines embody these principles: built with stainless-steel hygiene, PLC precision, and turnkey automation, they empower factories worldwide to achieve reliability, efficiency, and world-class quality.
Final Thoughts and Call to Action
If you’re planning to establish or expand a wet cat food production facility, success depends on precision engineering, hygienic design, and process optimization. Partnering with an experienced machinery manufacturer like Darin Machinery means gaining not only equipment but also expertise — from formulation guidance to installation, testing, and training.
With decades of industry experience, Darin helps global clients transition from small-scale operations to fully automated smart factories capable of producing pâté, chunk-in-gravy, or custom wet cat food recipes with export-ready certification (CE, ISO, SGS).
📞 WhatsApp: +86 156 5000 7983
🌐 Website: www.petreatsmachine.com
📧 Email: darin4@darin.cn