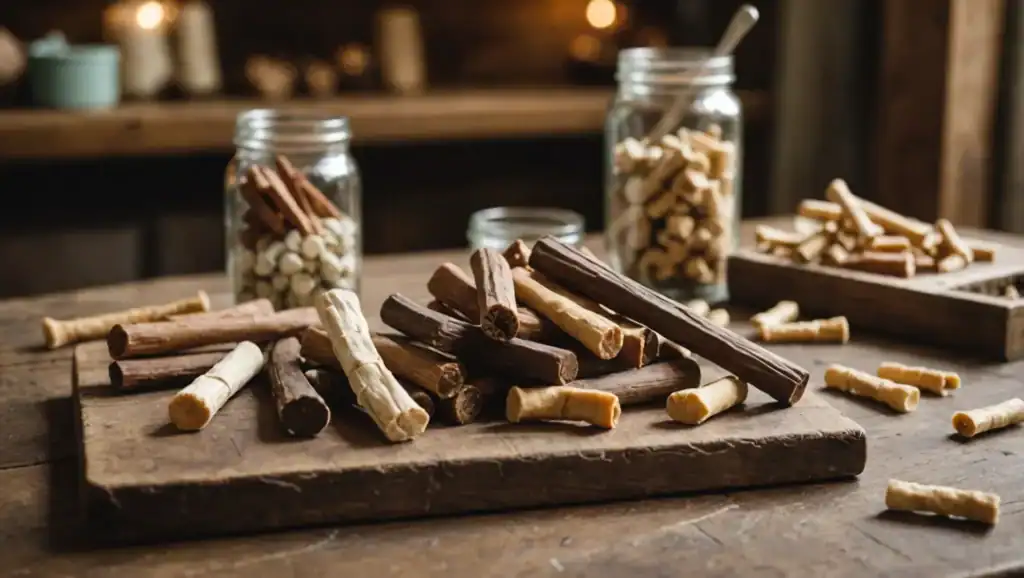
The global pet treat market is growing exponentially, and dog chews—ranging from rawhide bones to starch-based sticks and meaty dental treats—represent a premium, high-margin category. Yet many new investors or pet food processors face the same critical challenge: how to configure a complete, automated dog chew production line that ensures consistent texture, appearance, and nutrition while maintaining efficiency and food safety.
Without proper system integration, issues such as inconsistent moisture, weak bonding, or non-uniform shape can cause product rejection and production loss. Moreover, poor drying control or material selection can lead to microbial contamination or texture failure.
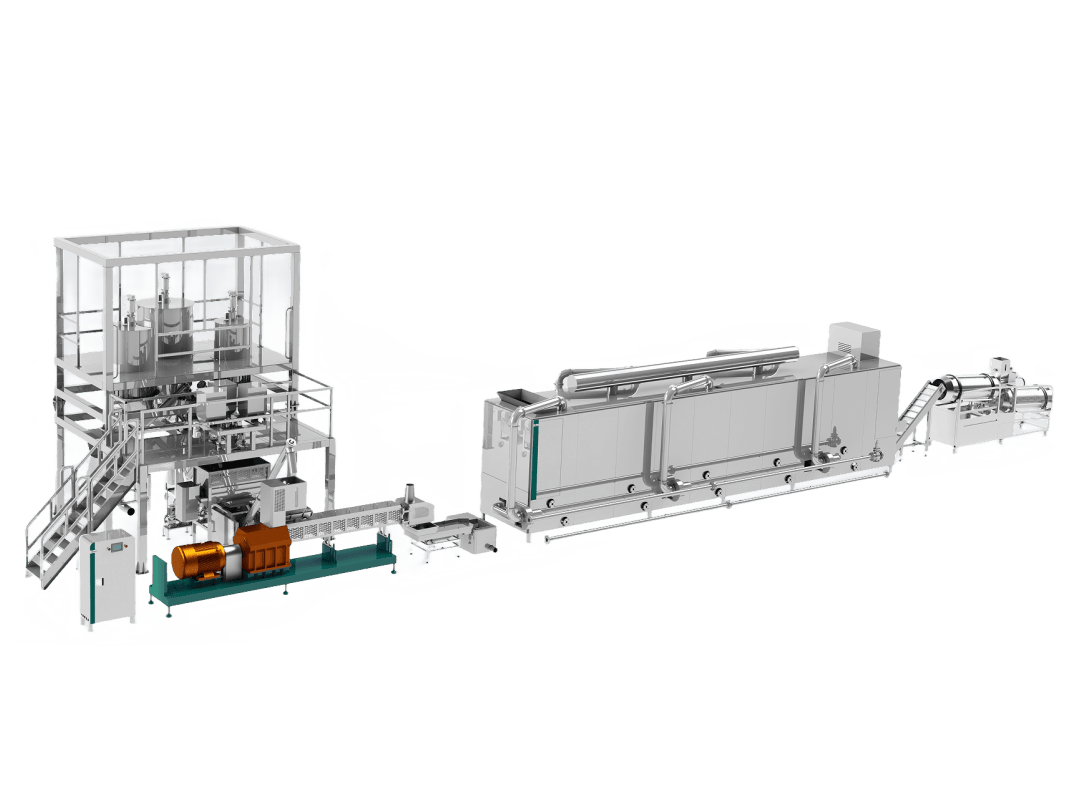
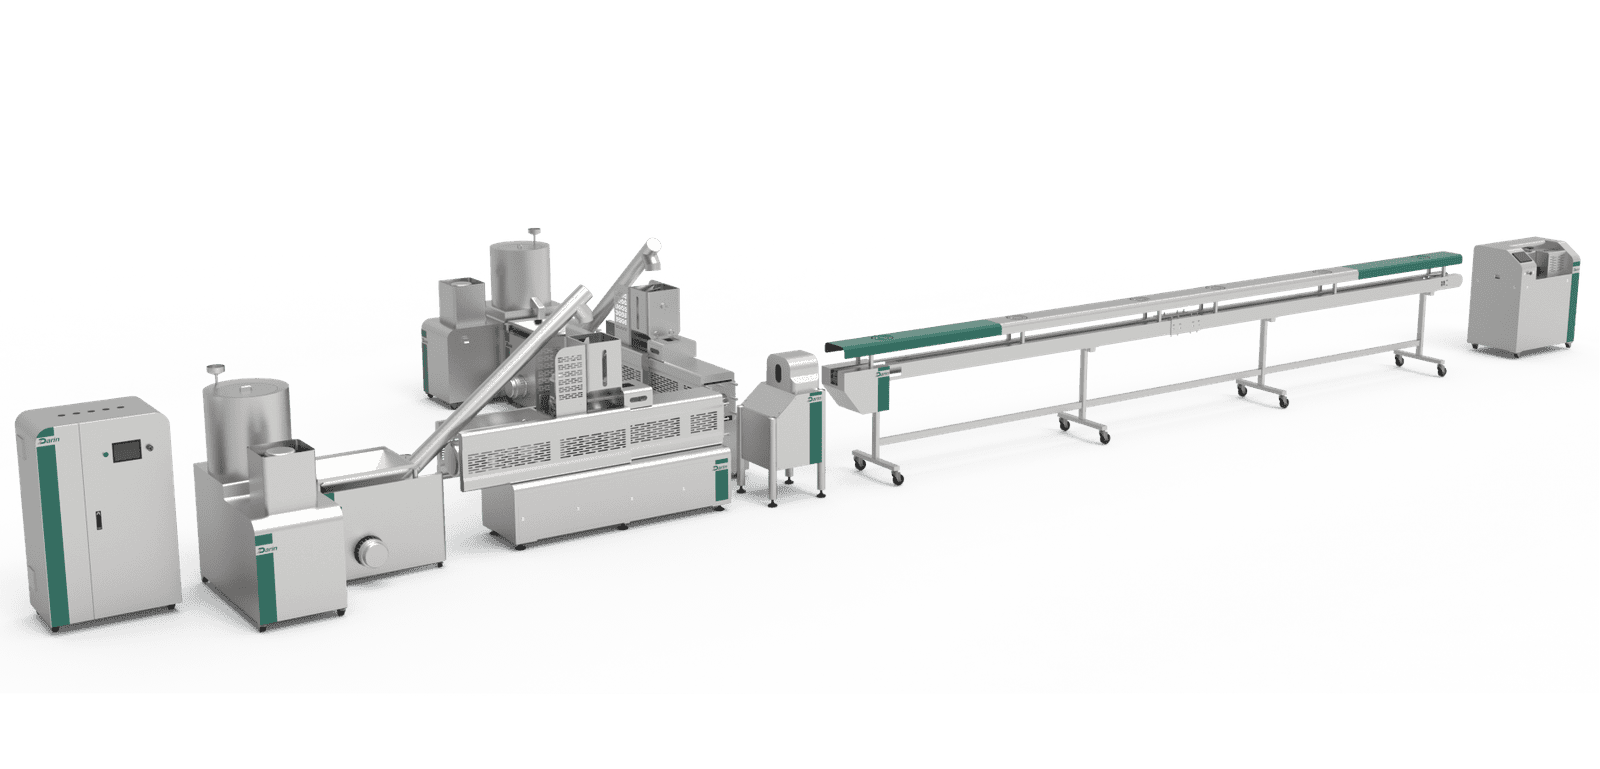
The good news? A well-designed dog chew production line, such as those engineered by Darin Machinery, enables producers to create flexible recipes—from starch-based to co-extruded filled chews—with automated feeding, extrusion, forming, drying, and packaging systems. Each step ensures precise temperature, moisture, and process control to produce consistent high-quality pet treats ready for both domestic and export markets.
A complete dog chew production line integrates several specialized systems—raw material preparation, mixing, extrusion, forming, cutting, drying, cooling, and packaging—each responsible for a specific phase in transforming basic ingredients into finished, safe, and uniform chews. These systems can be adapted for starch-based, rawhide, meat-based, or co-extruded products, enabling flexible production with minimal manual intervention and maximum throughput.
Dog chew products come in various textures and hardness levels depending on their formulation and process design. Whether your goal is a soft, jerky-like treat or a firm, twisted dental stick, understanding how each component contributes to the end quality is key. The next sections will explore every subsystem in technical depth—revealing the underlying engineering, material flow, and process control parameters that define a world-class dog chew line.
A dog chew production line can produce all types of chews using identical parameters.False
Different formulas (starch-based, meat-based, or rawhide) require customized temperature, moisture, and screw configurations to achieve proper texture and bonding strength.
Step 1. Understanding the Product Categories and Formulation Fundamentals
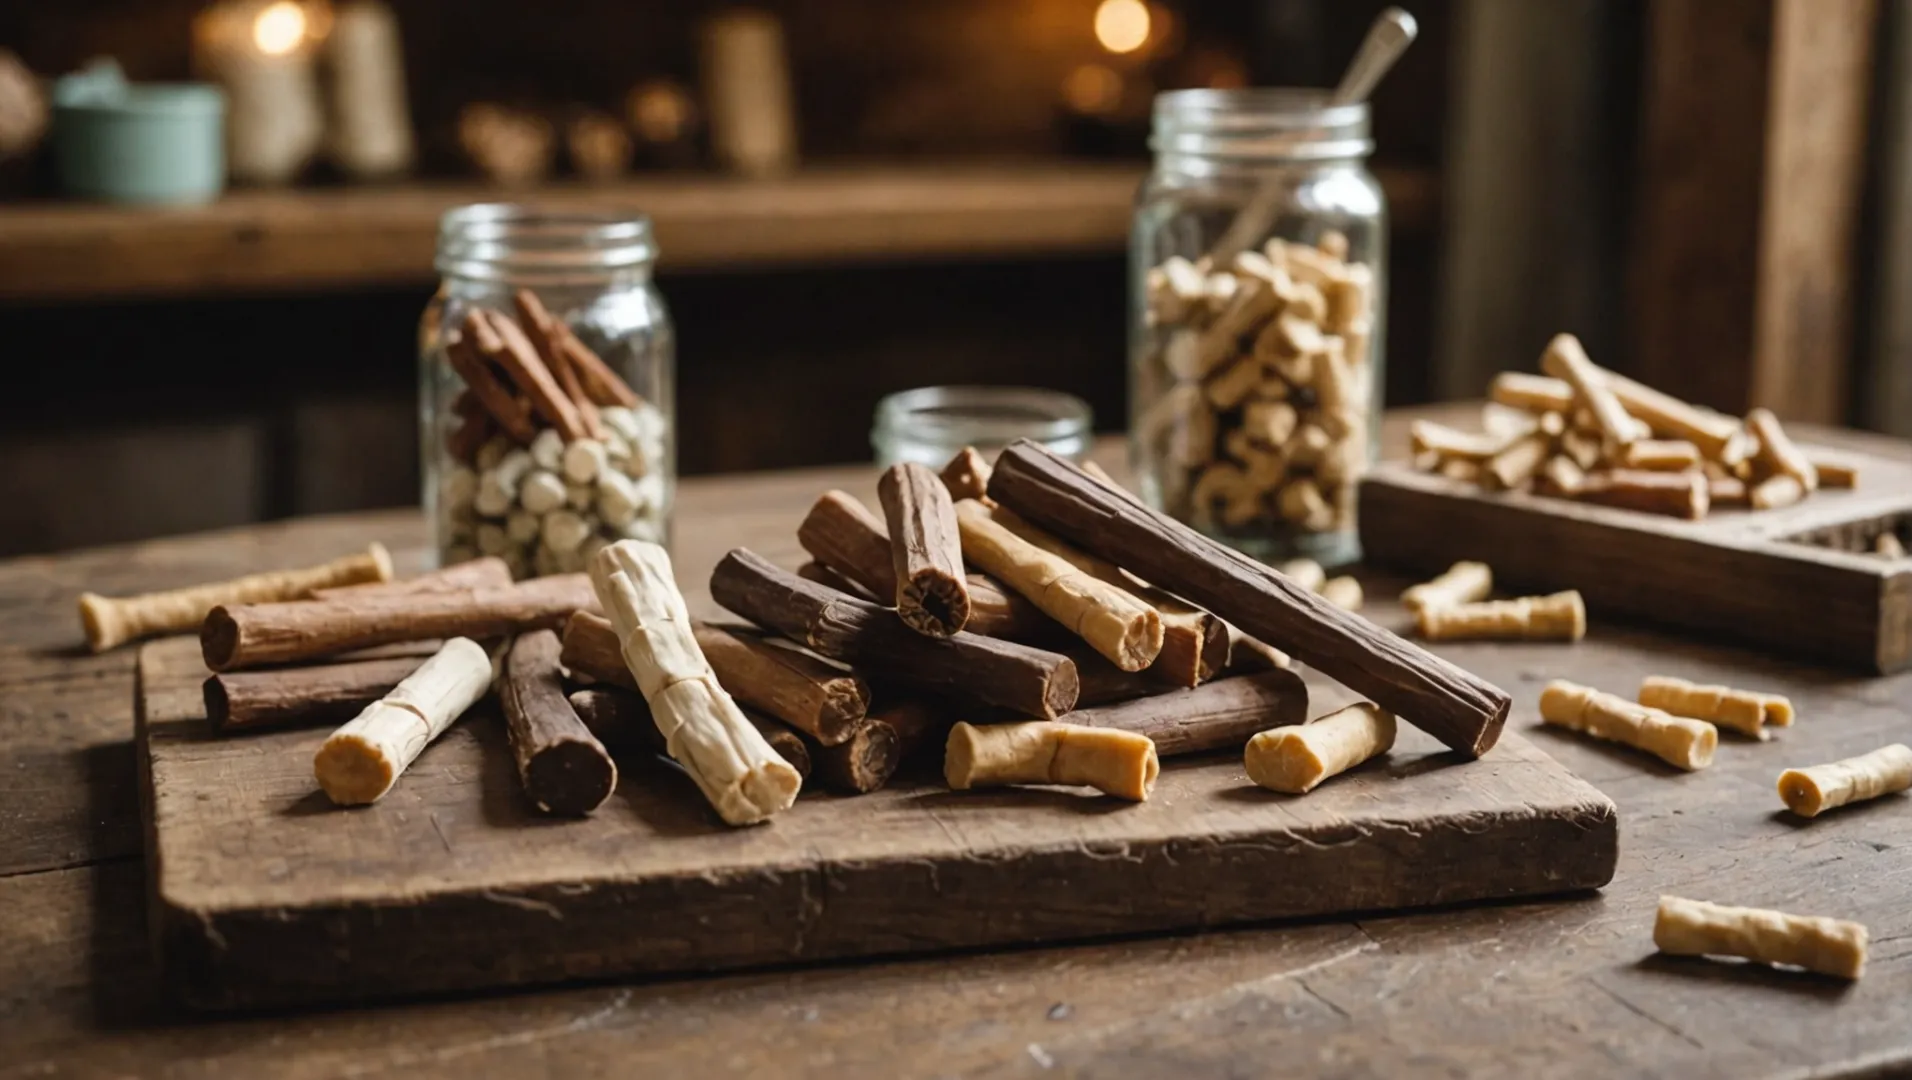
Before selecting machinery, one must define the product category because the formulation directly affects equipment design. Darin Machinery categorizes dog chews into four major process families:
| Dog Chew Type | Main Raw Materials | Processing Method | Texture | Moisture (%) | Typical Shelf Life |
|---|---|---|---|---|---|
| Rawhide Chew | Deproteinized cow/buffalo hide, gelatin, starch binders | Soaking → Cutting → Forming → Drying | Hard, long-lasting | 8–12 | 12–24 months |
| Starch-Based Chew | Corn/potato/tapioca starch, glycerin, protein, colorants | Twin-screw extrusion | Flexible, medium hardness | 8–12 | 12–18 months |
| Meat-Based Chew | Meat meal, starch, collagen, fat | Co-extrusion or forming | Soft, chewy | 12–18 | 6–12 months |
| Dental Stick | Cereal starch, calcium, chlorophyll, mint flavor | Twin-screw extrusion + ridged die | Firm, textured | 8–10 | 12–18 months |
Each type determines not only the extruder configuration but also dryer type, moisture curve, and packaging barrier requirements.
In practical engineering, starch-based lines offer the most automation potential, whereas rawhide lines still require some manual operations in soaking and shaping due to the rawhide’s natural variability.
Step 2. Raw Material Handling System
The efficiency of a dog chew production line starts long before extrusion. It begins with precise raw material handling.
2.1 Ingredient Reception and Storage
Dry powders (starch, flour, proteins) and liquid ingredients (glycerin, flavors, colors) must be stored under hygienic, controlled conditions to prevent contamination and moisture absorption.
| Material Type | Storage Method | Control Parameter | Safety Standard |
|---|---|---|---|
| Powder | SS304 silos with dust filters | Humidity < 55% | HACCP |
| Liquid | SS316 jacketed tanks | Temp 25–30°C | CE / FDA food grade |
| Collagen/gelatin | Refrigerated storage | 2–8°C | ISO 22000 |
Automatic screw conveyors or pneumatic transport systems deliver ingredients to the weighing and mixing stations, reducing human contact and cross-contamination.
2.2 Weighing and Batching
Automated weighing systems ensure formulation accuracy, a key factor in maintaining product consistency.
System Components:
- Multi-hopper batching station
- Load-cell weighing
- PLC control with recipe database
Accuracy: ±0.2% for dry ingredients, ±0.5% for liquids
For high-value ingredients like vitamins or flavors, Darin’s modular batching unit allows micro-dosing up to 0.01 kg increments.
2.3 Grinding and Particle Conditioning
Uniform particle size influences extrusion stability and chew texture. Most formulations require ingredients milled to 60–80 mesh.
Typical equipment: pin mill or hammer mill.
Key Parameters:
| Parameter | Range | Function |
|---|---|---|
| Rotor Speed | 3000–6000 rpm | Determines fineness |
| Screen Size | 0.2–0.6 mm | Controls powder uniformity |
| Airflow | 20–30 m³/h | Reduces temperature rise |
The ground powder is pneumatically conveyed to storage bins for intermediate holding.
Step 3. Mixing and Homogenization
The mixing system transforms raw ingredients into a uniform pre-extrusion blend. Homogeneity is vital; even small differences in moisture or ingredient concentration can lead to inconsistent extrusion torque and product texture.
3.1 Mixing Equipment Options
| Mixer Type | Function | Capacity | Advantages |
|---|---|---|---|
| Ribbon Blender | Dry blending | 100–1000 kg/batch | Fast mixing, low shear |
| Paddle Mixer | Wet blending | 100–800 kg/batch | Gentle motion, ideal for sticky materials |
| Vacuum Mixer | For glycerin, gelatin inclusion | 50–500 kg/batch | Removes air bubbles, improves density |
The process sequence:
- Load dry powders → 2. Mix for 3–5 min → 3. Inject liquids (glycerin/flavor) → 4. Mix 2–3 min → 5. Discharge into feeder.
Darin’s vacuum mixing system achieves CV (Coefficient of Variation) ≤ 5%, ensuring uniformity required for extrusion.
3.2 Preconditioning
A preconditioner can be installed upstream of the extruder to partially gelatinize starch and denature proteins. This improves bonding and reduces extruder energy demand.
Operating Parameters:
- Steam pressure: 0.2–0.4 MPa
- Residence time: 1–3 min
- Moisture after preconditioning: 20–30%
This system provides controlled hydration and preheating before entering the extruder barrel.
Step 4. Extrusion—The Core Transformation
Extrusion is the heart of dog chew production, converting mixed materials into a thermoplastic mass that can be shaped, colored, and cut.
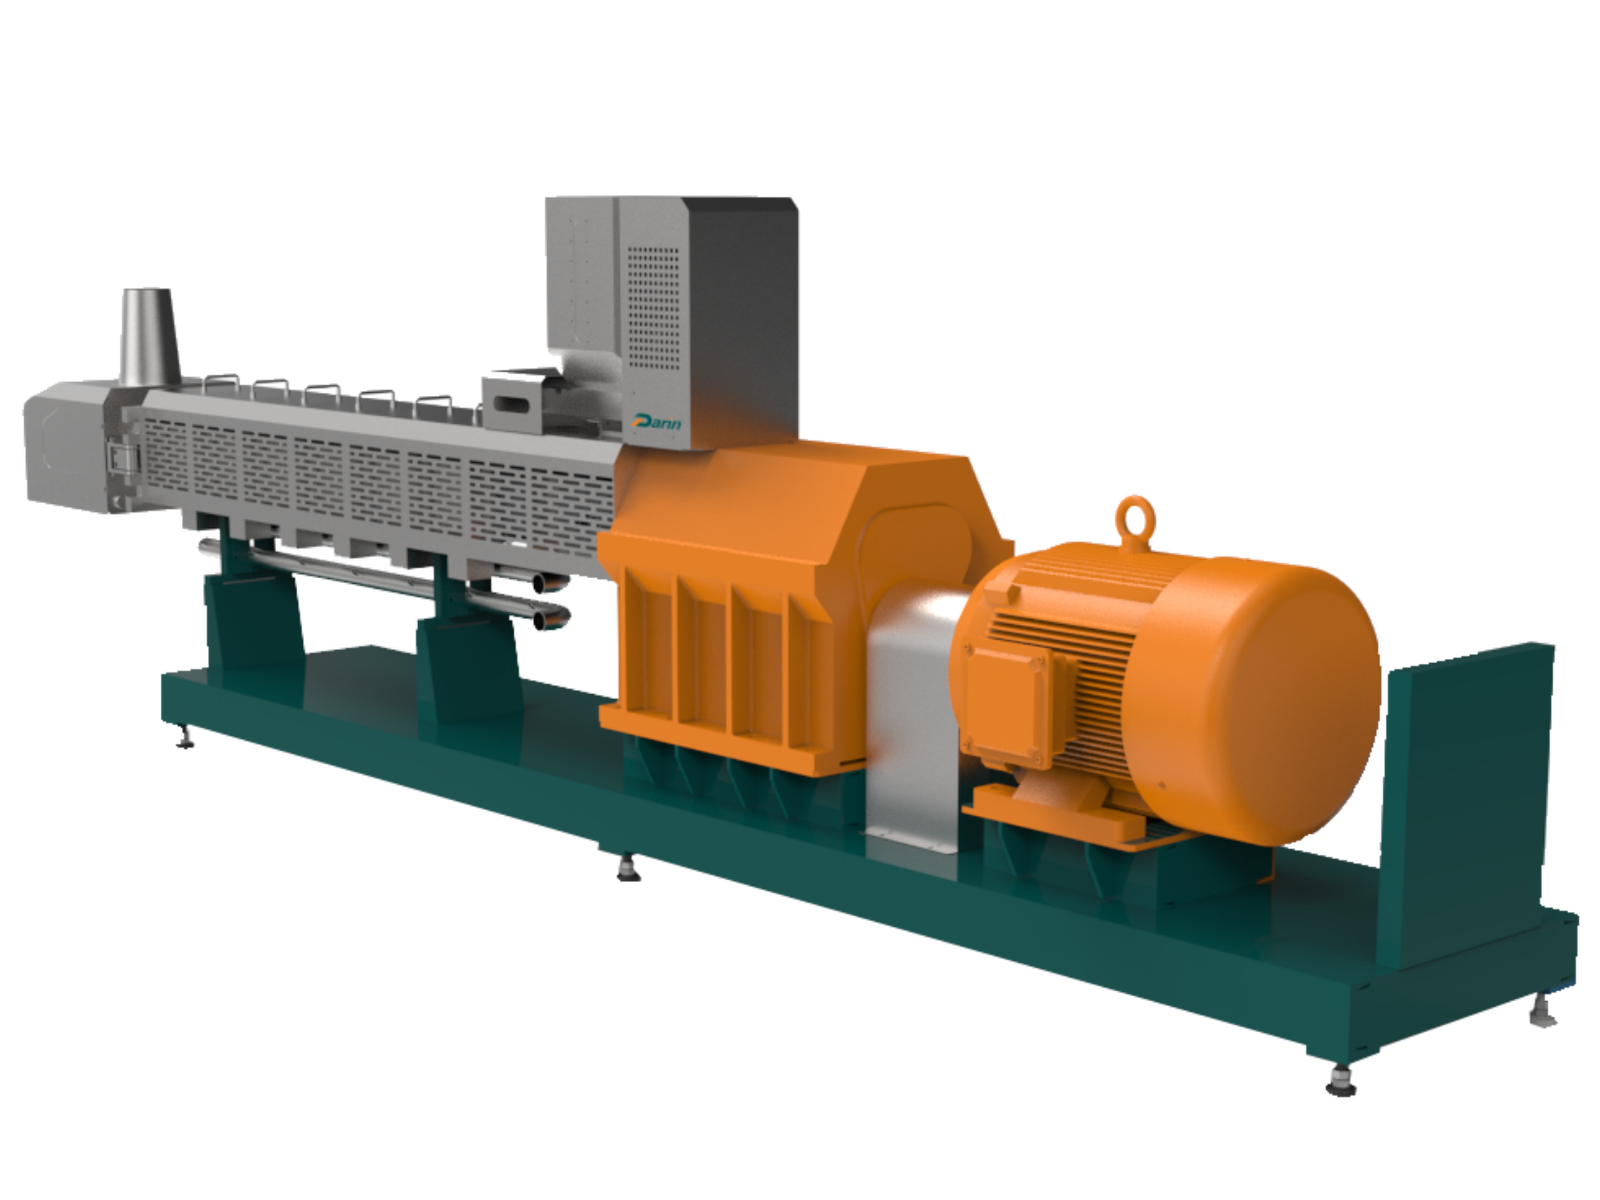
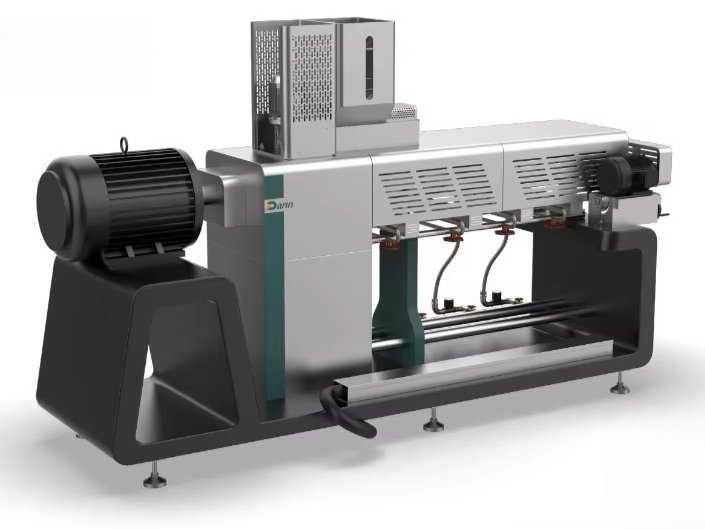
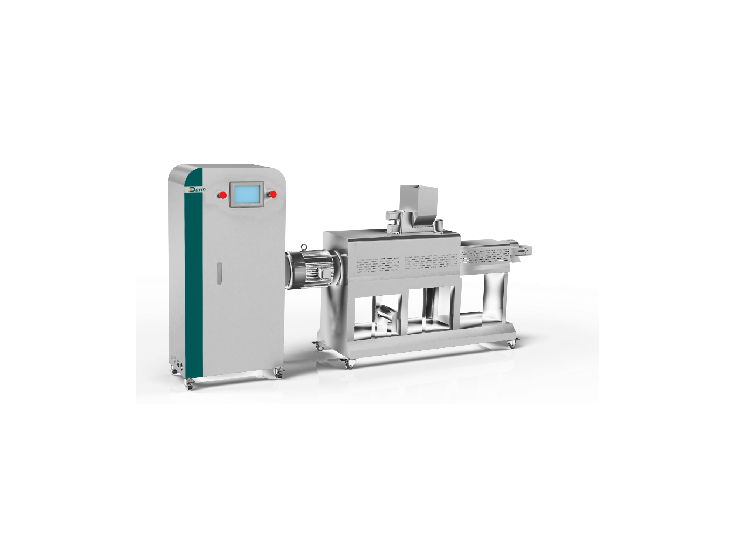
4.1 Twin-Screw Extruder Design
Darin’s DR-series twin-screw extruders use co-rotating intermeshing screws, ensuring excellent mixing and self-cleaning.
Main Components:
- Feeder
- Barrel with modular zones
- Twin-screw shafts
- Heating/cooling jacket
- Die head
Typical Configuration:
| Zone | Function | Temperature (°C) |
|---|---|---|
| Feeding | Material intake | 30–50 |
| Mixing | Shear and blending | 80–100 |
| Cooking | Starch gelatinization | 110–140 |
| Degassing | Vapor release | 90–100 |
| Die | Shaping outlet | 100–120 |
Key Process Parameters:
| Parameter | Range | Impact |
|---|---|---|
| Screw Speed | 200–500 rpm | Density and texture |
| Torque Load | 70–90% | Indicates mechanical efficiency |
| Moisture | 20–35% | Affects chew elasticity |
| Specific Mechanical Energy (SME) | 100–200 kJ/kg | Influences expansion and bonding |
A single-screw extruder can easily produce dual-color and filled dog chews.False
Only twin-screw extruders can precisely handle multiple feed streams with consistent pressure and temperature control, required for co-extruded or multi-color chews.
4.2 Product Shaping Through Dies
The extruder’s die determines geometry and surface finish. Darin provides over 60 die shapes: rods, stars, twists, rings, bones, and dental ridges.
| Die Type | Shape | Typical Use |
|---|---|---|
| Circular | Round sticks | Basic chew sticks |
| Star | 4–6 ridges | Dental sticks |
| Flat | Strip or ribbon | Jerky-style treats |
| Co-extrusion Die | Core-shell | Filled treats |
| Multi-die plate | Parallel strands | High throughput |
Die temperature and cooling calibration ensure dimensional stability.
Cooling at exit: 10–20 °C water jacket prevents deformation and improves surface smoothness.
Step 5. Co-Extrusion and Multi-Color Options
Premium dog chews often combine two materials—an inner core (meat, flavor) and an outer shell (starch or vegetable). Co-extrusion enables these high-value variants.
System Configuration:
- Two synchronized extruders
- Co-extrusion die with core–shell channels
- Servo-driven feed ratio control (outer:inner = 70:30 typical)
Engineering Advantages:
- Enhanced visual appeal
- Nutritional differentiation
- Multi-flavor possibilities
Key Controls:
- Pressure balance between inner and outer streams
- Die centering system for concentricity
- Moisture consistency (±2%)
Process Control Snapshot (for Starch-Based Dual-Color Chew)
| Parameter | Value | Control Method |
|---|---|---|
| Outer Extruder Temp | 130°C | PID control |
| Inner Extruder Temp | 110°C | Separate heater band |
| Die Pressure | 6.5 MPa | Dual transducer feedback |
| Output Rate | 250 kg/h | Servo coordination |
Typical Output Range: 150–1000 kg/h per line (scalable).

After extrusion and shaping, the newly formed dog chews—whether starch-based, meat-filled, or co-extruded—are still warm, moist, and fragile. At this point, precise cutting, drying, and cooling systems are essential to transform these semi-finished strands into durable, shelf-stable treats that meet both sensory and microbiological standards.
In this part of the guide, we’ll move through Steps 6 to 12, examining cutting, drying, cooling, inspection, packaging, automation, cleaning, and certification—all key to achieving a reliable, high-yield dog chew production line.
From extrusion to final packaging, the downstream section of a dog chew line ensures product stability, shape retention, moisture balance, and safety. Automated cutting synchronizes with the extruder output, while multi-zone dryers and precision coolers guarantee long shelf life without cracks or discoloration. Advanced quality control, metal detection, and packaging technologies make sure every chew leaving the factory meets global pet food compliance standards.
Dog chews can be sun-dried in open air for industrial-scale production.False
Industrial pet treat production requires controlled hot-air or microwave drying to maintain hygiene, uniformity, and consistent moisture content, preventing microbial contamination.
Step 6. Cutting and Forming — Precision Defines Quality
Immediately after extrusion, the continuous strands of dog chew dough must be cut into consistent lengths or shapes. Cutting precision ensures packaging efficiency and a professional product appearance.
6.1 Cutting Mechanisms
| Cutter Type | Working Principle | Control Method | Typical Use |
|---|---|---|---|
| Rotary Cutter | Rotating blades synchronized with extrusion speed | Servo motor | Continuous rod or stick shapes |
| Guillotine Cutter | Pneumatic knife cuts at set intervals | PLC controlled | Bone or cube-shaped chews |
| Twisting Unit | Mechanically twists dual-color strands | Servo-driven | Twisted sticks |
| Embossing Roller | Imprints logo or texture | Temperature-controlled roll | Dental or branded treats |
Technical Highlights:
- Servo motor control allows length accuracy ±1 mm.
- Sensor feedback loop ensures synchronization with extruder throughput.
- Stainless steel cutting chambers prevent contamination.
6.2 Product Handling
Cut pieces fall onto a vibrating cooling conveyor that separates overlapping pieces. Cooling to 50–60°C prevents sticking and prepares the chews for drying.
Output Example (500 kg/h line):
- 250–300 sticks/minute
- Uniform diameter 10–15 mm
- Length adjustable 50–180 mm
Step 7. Drying System — The Key to Texture and Shelf Life
Drying is the most energy-intensive and time-sensitive stage in dog chew production. The goal is to reduce moisture from 20–30% to 8–12% while maintaining flexibility and preventing cracks.
7.1 Multi-Layer Belt Dryer
This is the standard dryer in Darin Machinery’s starch-based and co-extruded chew lines. It uses a continuous hot-air system with independent zones for uniform drying.
Engineering Parameters:
| Parameter | Range | Function |
|---|---|---|
| Temperature | 80–120°C | Moisture removal |
| Air Velocity | 1.5–2.5 m/s | Even heat transfer |
| Residence Time | 1.5–3 hours | Moisture balance |
| Final Moisture | ≤12% | Shelf stability |
Each layer of the dryer (3–7 tiers) carries chews on food-grade mesh belts. PID controllers maintain independent zone temperatures for optimal drying profiles.
Advantages:
- Energy-efficient heat recovery system
- Gentle air circulation avoids deformation
- Automatic cleaning of air filters
7.2 Hot-Air Circulation Oven
Used in pilot or specialty lines (200–300 kg/h). Ideal for small-batch production or high-end jerky-type chews requiring gradual drying.
7.3 Microwave Dryer (Optional)
For premium soft chews, microwave dryers accelerate drying by volumetric heating—preserving elasticity and flavor.
Operating Parameters:
- Frequency: 2450 MHz
- Output Power: 60–80 kW
- Time: 10–15 min
Microwave drying damages the nutritional content of pet chews.False
Properly controlled microwave drying preserves nutrients and reduces drying time, minimizing heat damage compared to prolonged hot-air exposure.
7.4 Moisture Control Curve
| Stage | Time (min) | Target Moisture (%) | Remarks |
|---|---|---|---|
| Preheat | 0–20 | 20–25 | Surface evaporation |
| Core Drying | 20–80 | 12–18 | Controlled airflow |
| Final Drying | 80–120 | 8–12 | Moisture equalization |
| Cooling | 120–140 | Stable | Ambient balance |
Maintaining the proper drying curve ensures soft, glossy texture without internal stress fractures.
Step 8. Cooling and Conveying
After drying, chews remain hot and brittle. Controlled cooling stabilizes their structure and prevents condensation during packaging.
Cooling System Configuration:
- Stainless steel conveyor (length: 6–10 m)
- Filtered air circulation (20–25°C)
- Adjustable cooling duration (10–30 min)
- Optional dehumidifier module
Technical Indicators:
- Final product temperature ≤35°C
- Relative humidity ≤50%
- Airflow direction alternating top-bottom
Design Optimization:
In Darin lines, air diffusers ensure even temperature distribution across conveyor width. PLC-integrated sensors trigger alarms for any deviation >2°C.
Step 9. Quality Inspection and Sorting
Modern production lines integrate intelligent inspection systems for product uniformity, hygiene, and safety.
9.1 Metal Detection
To prevent contamination, an inline metal detector is installed between the cooler and packaging section.
Detection sensitivity: Fe ≥0.8 mm, Non-Fe ≥1.0 mm.
9.2 Check Weigher
Automatic check weighers ensure each pack meets target weight within ±1.5%.
9.3 Optical Sorter (Optional)
High-resolution cameras detect color or shape deviations. Rejected pieces are pneumatically removed.
Quality Control Targets:
| Attribute | Specification | Testing Frequency |
|---|---|---|
| Moisture | 8–12% | Every batch |
| Density | 1.05–1.20 g/cm³ | Hourly |
| Tensile Strength | >1.2 MPa | Daily |
| Surface Smoothness | No cracks | Continuous |
| Color Uniformity | ΔE ≤ 2.0 | Continuous |
Darin’s advanced AI vision systems automatically store inspection images in the PLC for traceability under ISO 22000 compliance.
Step 10. Packaging — Protecting Freshness and Brand Image
Packaging determines shelf life and consumer appeal. A good packaging system minimizes oxygen exposure, ensures sealing integrity, and enhances presentation.
10.1 Packaging Options
| Packaging Type | Description | Machine Type | Speed (packs/min) |
|---|---|---|---|
| Pillow Bag | Flow-wrap single sticks | Horizontal flow wrapper | 60–120 |
| Stand-up Pouch | Zipper resealable bag | Rotary pre-made bag packer | 30–60 |
| Bulk Bag | 1–5 kg large packs | VFFS machine | 30–70 |
Advanced Functions:
- Nitrogen flushing to extend shelf life
- Date code printer and barcode applicator
- Multihead weigher integration for accuracy ±1 g
10.2 Barrier Film Selection
| Product Type | Recommended Film | Features |
|---|---|---|
| Soft Chew | PET/AL/PE | High oxygen barrier |
| Dental Stick | OPP/CPP | Glossy finish |
| Rawhide Bone | Kraft + PE | Natural texture look |
10.3 Palletizing and Case Packing
Automated pick-and-place robots can stack finished bags into cartons. Darin’s end-of-line automation reduces labor by 40% and ensures consistent pallet patterns for export shipping.
Step 11. Automation, Control, and Digital Integration
In a modern factory, automation defines not only productivity but also consistency and traceability.
11.1 Central PLC Control
- Siemens PLC with touch-screen HMI
- Recipe management (up to 200 formulations)
- Real-time monitoring of temperature, torque, and moisture
- Alarm log and data export for HACCP compliance
11.2 Data Connectivity
Ethernet/Modbus connection allows remote monitoring through Darin’s IoT platform.
Supervisors can check output rates, energy use, or temperature trends from any location.
11.3 Energy Efficiency
- Variable frequency drives (VFD) on motors reduce energy by up to 20%.
- Smart drying air recirculation saves heat energy.
- Automatic standby mode during idle feed times.
Energy Consumption Benchmark (500 kg/h line):
| Section | Power (kW) | Energy Efficiency |
|---|---|---|
| Extruder | 45 | Optimized screw geometry |
| Dryer | 36 | Recycled hot air |
| Mixer & Feeder | 10 | VFD control |
| Cooling & Conveying | 2 | Low-friction design |
| Packaging | 3.5 | Servo motors |
Step 12. Cleaning, Maintenance, and Sanitation
Pet treat lines must meet strict hygienic standards. Darin designs all contact surfaces in SS304/SS316 with tool-free disassembly.
12.1 Clean-in-Place (CIP) System
- Automatic water and detergent spraying nozzles
- Hot water (70–80°C) circulation
- Drain design preventing residue accumulation
Recommended Cleaning Schedule:
| Frequency | Task | Equipment |
|---|---|---|
| Daily | Wipe exterior surfaces | Mixers, conveyors |
| Weekly | Full barrel disassembly | Extruder |
| Monthly | Lubricate bearings | Motors |
| Quarterly | Replace sealing gaskets | Dryer doors |
| Yearly | Calibration and sensor verification | Full line |
12.2 Safety Design
- Emergency stop buttons at each module
- Overload protection and interlocking doors
- CE-compliant safety guards
- Dust extraction in mixing and cutting sections
Dog chew machinery can operate safely without daily cleaning.False
Regular cleaning is mandatory to prevent microbial growth and ensure consistent quality under HACCP and ISO 22000 standards.
Step 13. Quality Certification and Regulatory Compliance
To access international markets, compliance with food safety and machinery regulations is essential.
| Certification | Scope | Requirement |
|---|---|---|
| CE Marking | Machinery safety | Mandatory for EU |
| ISO 9001:2015 | Quality management | Factory certification |
| HACCP / ISO 22000 | Food safety | Required for food processing |
| FDA CFR Title 21 | Food contact materials | U.S. compliance |
| GMP (Good Manufacturing Practice) | Hygiene and process control | Voluntary but recommended |
Darin Machinery’s equipment meets or exceeds all these standards, ensuring worry-free export to markets across Europe, North America, and Asia-Pacific.
Step 14. Example: Complete Dog Chew Line Configuration
| Section | Equipment | Model | Power (kW) | Capacity (kg/h) | Material |
|---|---|---|---|---|---|
| Mixer | Horizontal Ribbon Mixer | DR-MX500 | 7.5 | 500 | SS304 |
| Extruder | Twin-Screw Extruder | DR-65 | 45 | 500 | SS304 |
| Cutter | Servo Rotary Cutter | DR-CUT | 1.5 | — | SS304 |
| Dryer | Multi-Layer Belt Dryer | DR-DRY | 36 | 500 | SS304 |
| Cooler | Cooling Conveyor | DR-COOL | 2 | — | SS304 |
| Metal Detector | Inline Unit | DR-MD | 1 | — | — |
| Packaging | Automatic Pillow Wrapper | DR-PACK | 3.5 | 60 packs/min | SS304 |
Total Power: ~95 kW
Line Length: ~25 m
Operator Requirement: 2–3 persons/shift
Factory Layout Recommendation:
Straight-line layout with 800–1000 m² area, ensuring smooth raw-to-finished flow and hygiene zoning.
Step 15. Case Studies
Case 1: 500 kg/h Co-Extruded Dog Chew Line – Germany
- Dual-extruder setup with core–shell design
- Energy-saving dryer reduced cost by 18%
- Output: 4.2 tons/day
- Passed CE and HACCP audits within 2 months
Case 2: 300 kg/h Dental Stick Line – Vietnam
- High-speed rotary cutter (300 pcs/min)
- Local starch sourcing
- Custom die design for X-ridge dental shapes
Case 3: 800 kg/h Starch-Based Twisted Stick Line – Brazil
- Triple-die head for 3-color extrusion
- Integrated automatic packaging system
- Increased output by 25% vs previous line
Step 16. Troubleshooting Guide
| Problem | Possible Cause | Solution |
|---|---|---|
| Uneven color | Poor mixing or inconsistent temperature | Check preconditioner steam and die temp |
| Cracks after drying | Too high temperature or fast airflow | Reduce initial drying zone temp |
| Sticky chews | Incomplete drying or insufficient cooling | Extend final zone or add dehumidifier |
| Non-uniform shape | Die wear or extrusion pressure fluctuation | Replace die, calibrate feed rate |
| Poor bonding in co-extruded core | Moisture mismatch between layers | Adjust inner/outer moisture ratio to ±2% |
Step 17. Cost Analysis and ROI
Estimated CAPEX (500 kg/h line):
- Equipment: USD 180,000–250,000
- Installation & training: USD 10,000
- Spare parts & molds: USD 5,000
- Total: ~USD 200,000–270,000
Operational Cost per Hour:
| Item | Cost (USD/h) | Notes |
|---|---|---|
| Electricity | 9–12 | 95 kW total |
| Labor | 5–8 | 3 operators |
| Ingredients | 150–180 | Formula dependent |
| Packaging film | 10–15 | Stand-up pouch |
| Maintenance | 2–3 | Routine cost |
Typical ROI: 10–15 months depending on output and market price.
Step 18. Future Trends in Dog Chew Production
- Functional Chews: Incorporating probiotics, vitamins, and dental care ingredients.
- Sustainability: Using biodegradable films and plant-based proteins.
- AI Process Monitoring: Predictive maintenance and automatic recipe correction.
- Smart Recipe Adjustment: Moisture/viscosity sensors feeding real-time data to PLC.
Darin Machinery’s next-generation DRX line integrates sensor fusion technology to adjust screw speed and drying automatically, achieving 3–5% higher yield with less energy.
Conclusion
Producing high-quality dog chews isn’t merely about extrusion—it’s about orchestrating a precise sequence of engineering controls, from ingredient mixing to packaging. Each system—mixer, extruder, dryer, cooler, and packager—must operate in perfect harmony to ensure consistent quality, safety, and efficiency.
By mastering these 12+ stages, pet food manufacturers can scale confidently, diversify their product range, and compete globally. Whether producing starch-based sticks or dual-color filled bones, automation, hygiene, and technical precision form the backbone of success.
Ready to Build Your Complete Dog Chew Production Line?
Darin Machinery has spent over 20 years helping manufacturers across 70+ countries design and install pet treat lines—from small pilot systems to 1-ton/hour industrial plants. Each line is customized to your recipe, factory layout, and local regulatory standards.
Let’s make your project our next success story.
📞 Contact Darin Machinery Today
🌐 www.petreatsmachine.com
📧 Email: darin4@darin.cn
📱 WhatsApp: +86 156 5000 7983
Your trusted engineering partner for efficient, hygienic, and profitable dog chew production.